Apex Data Engineering

Apex Data Engineering
About Us

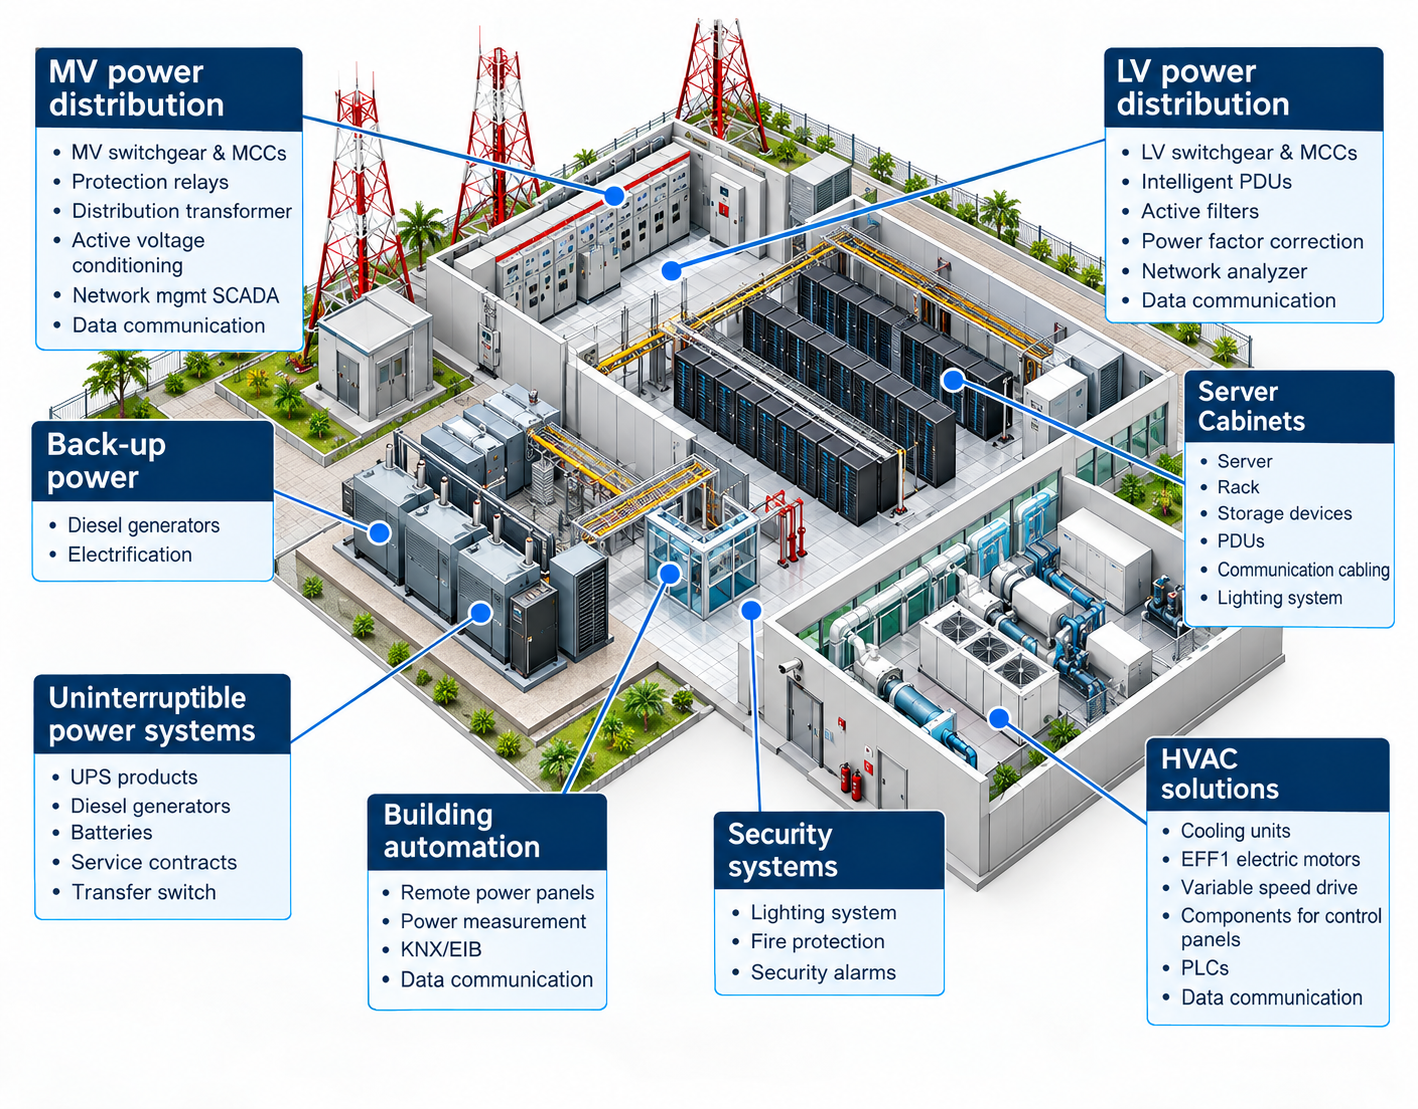
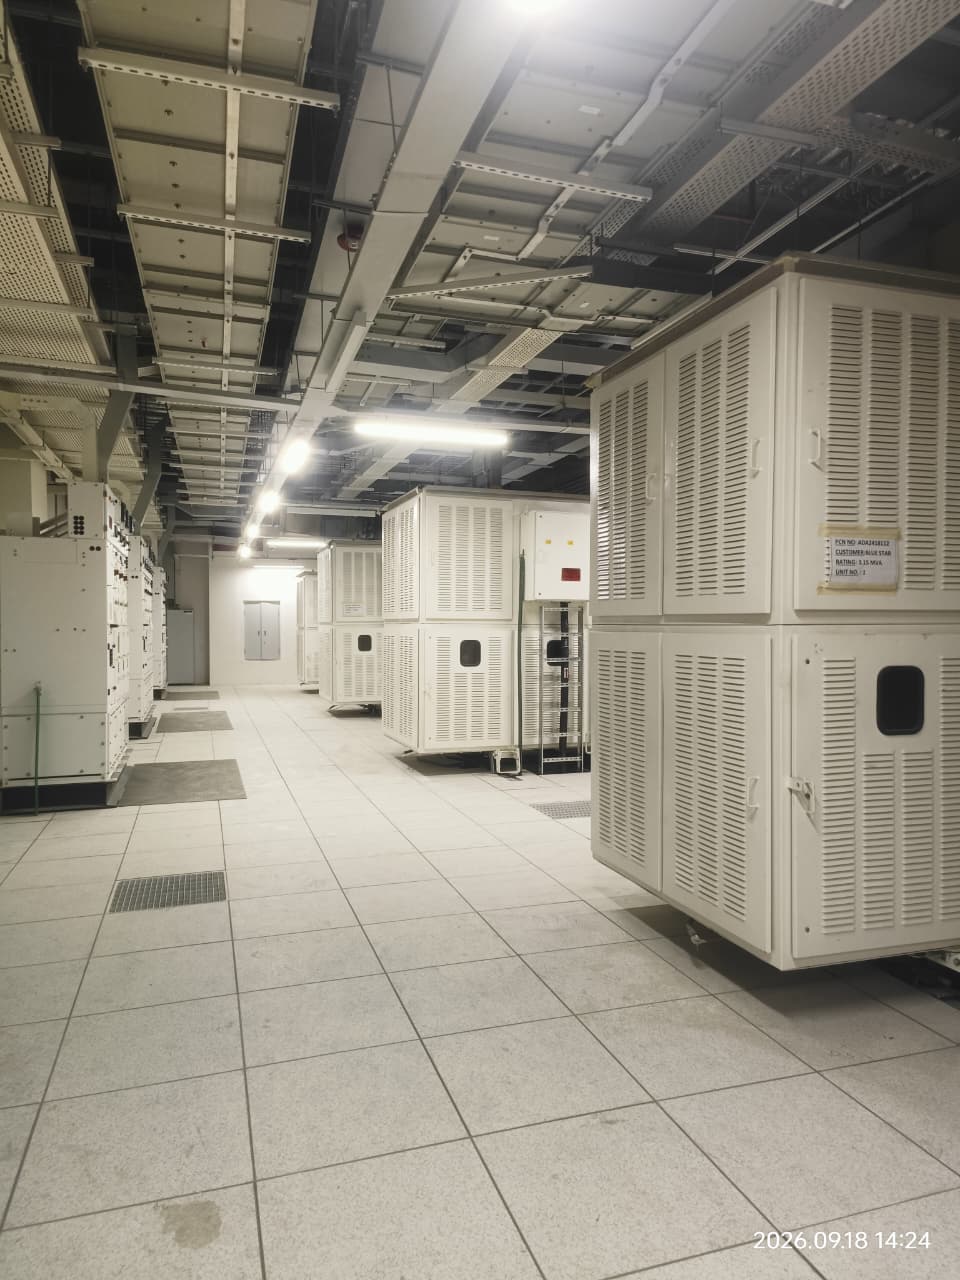
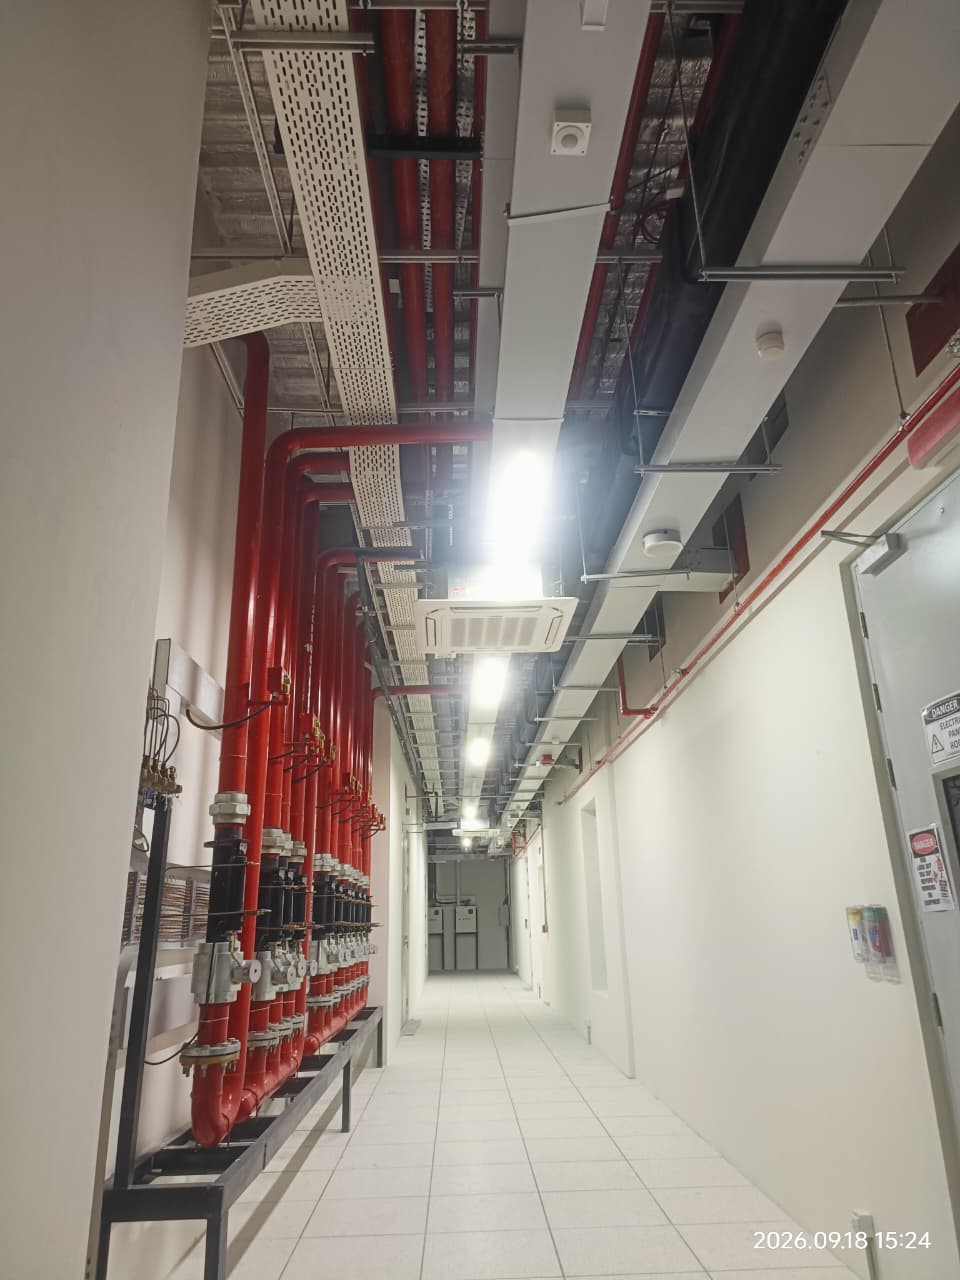
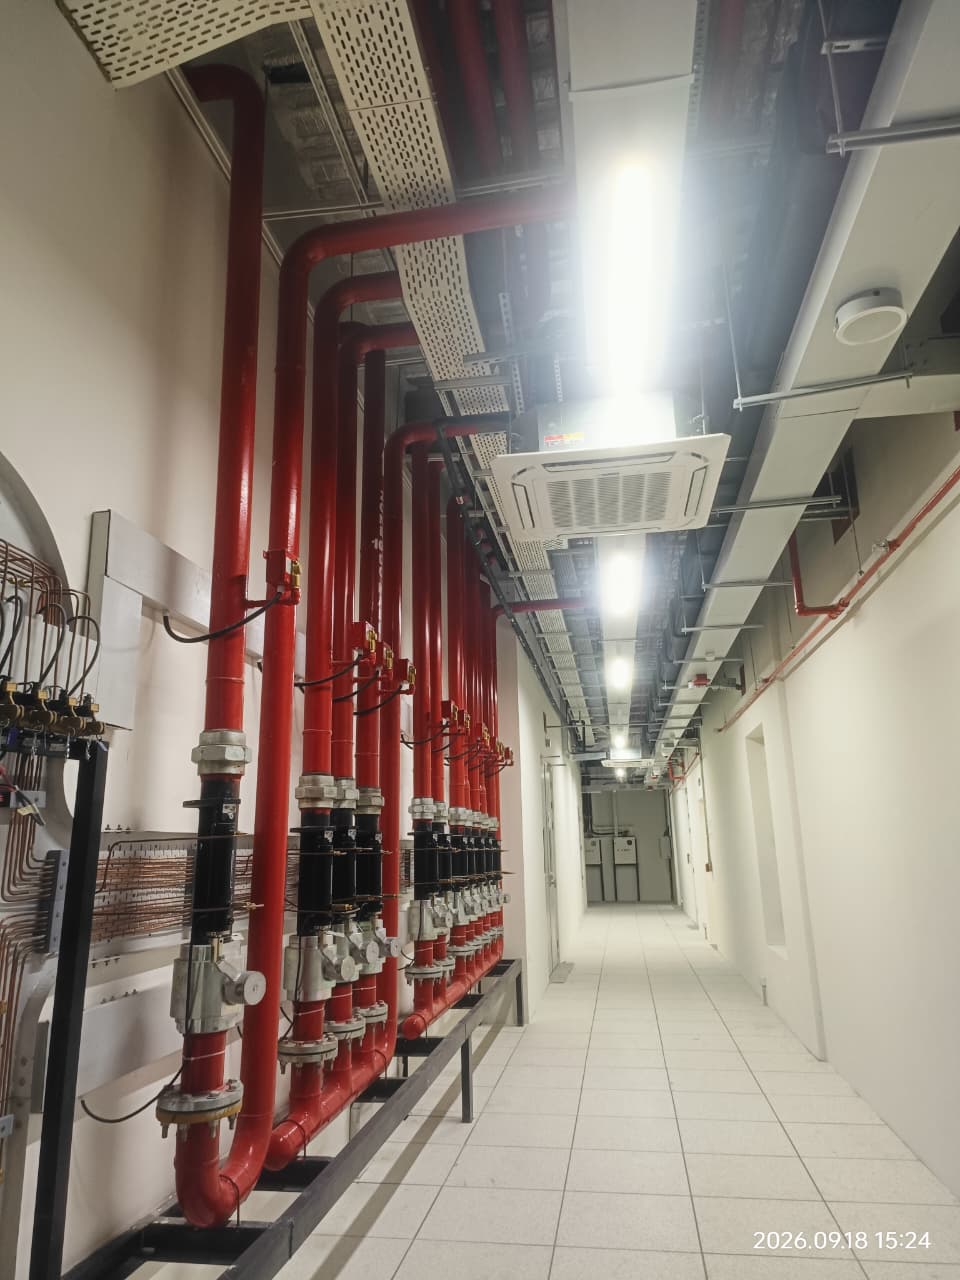
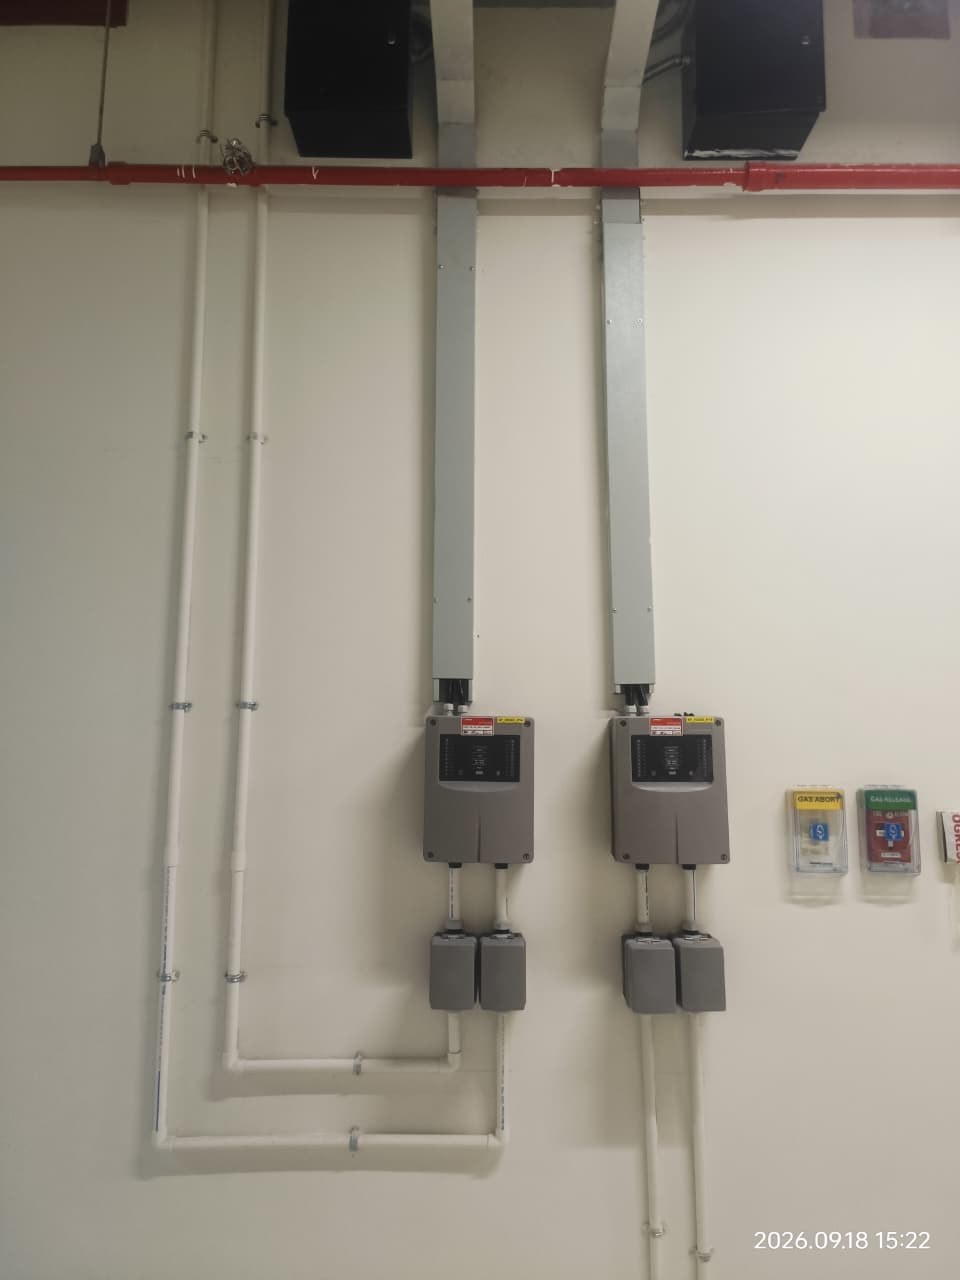
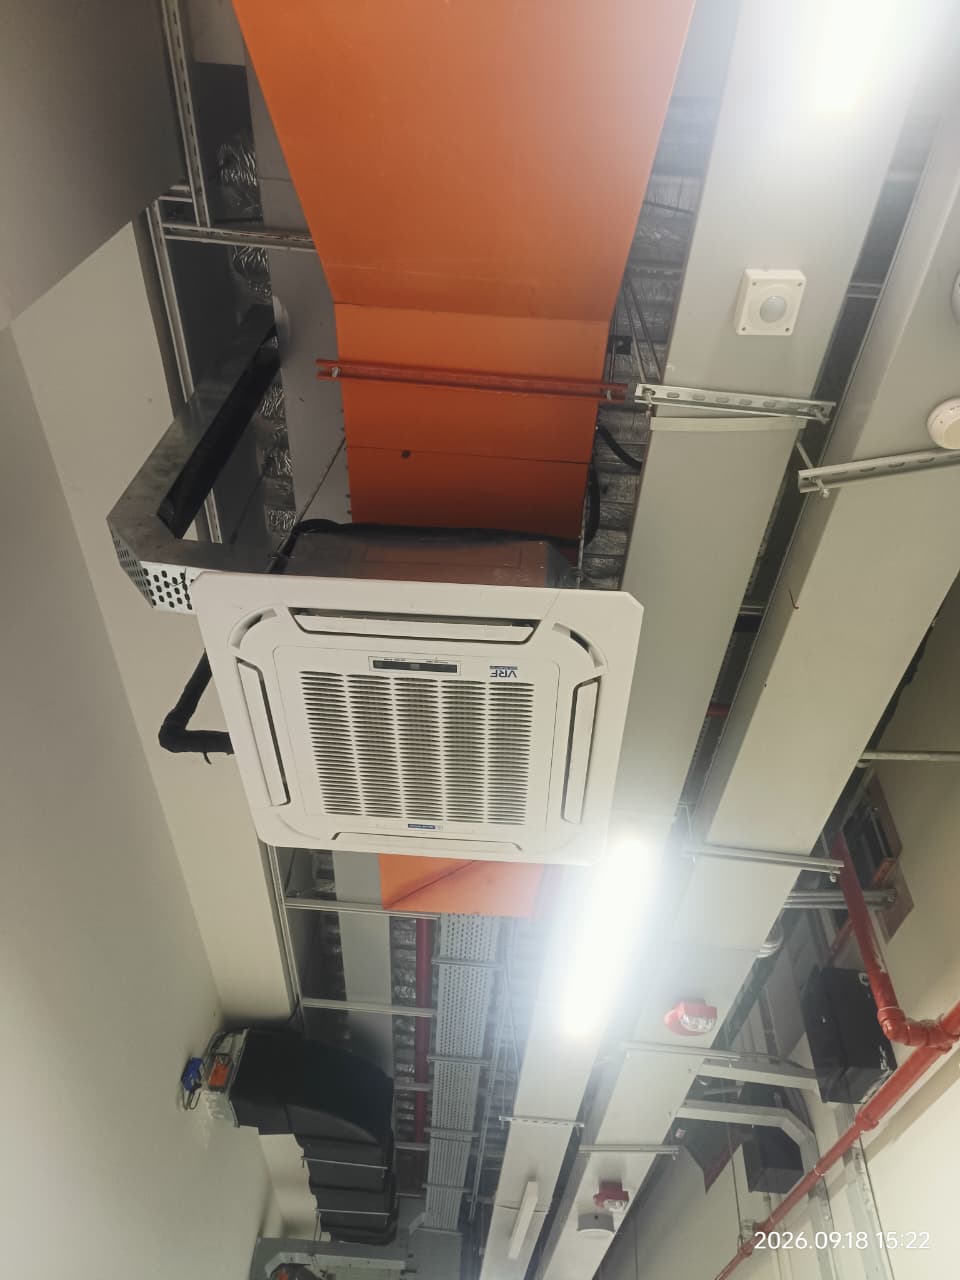
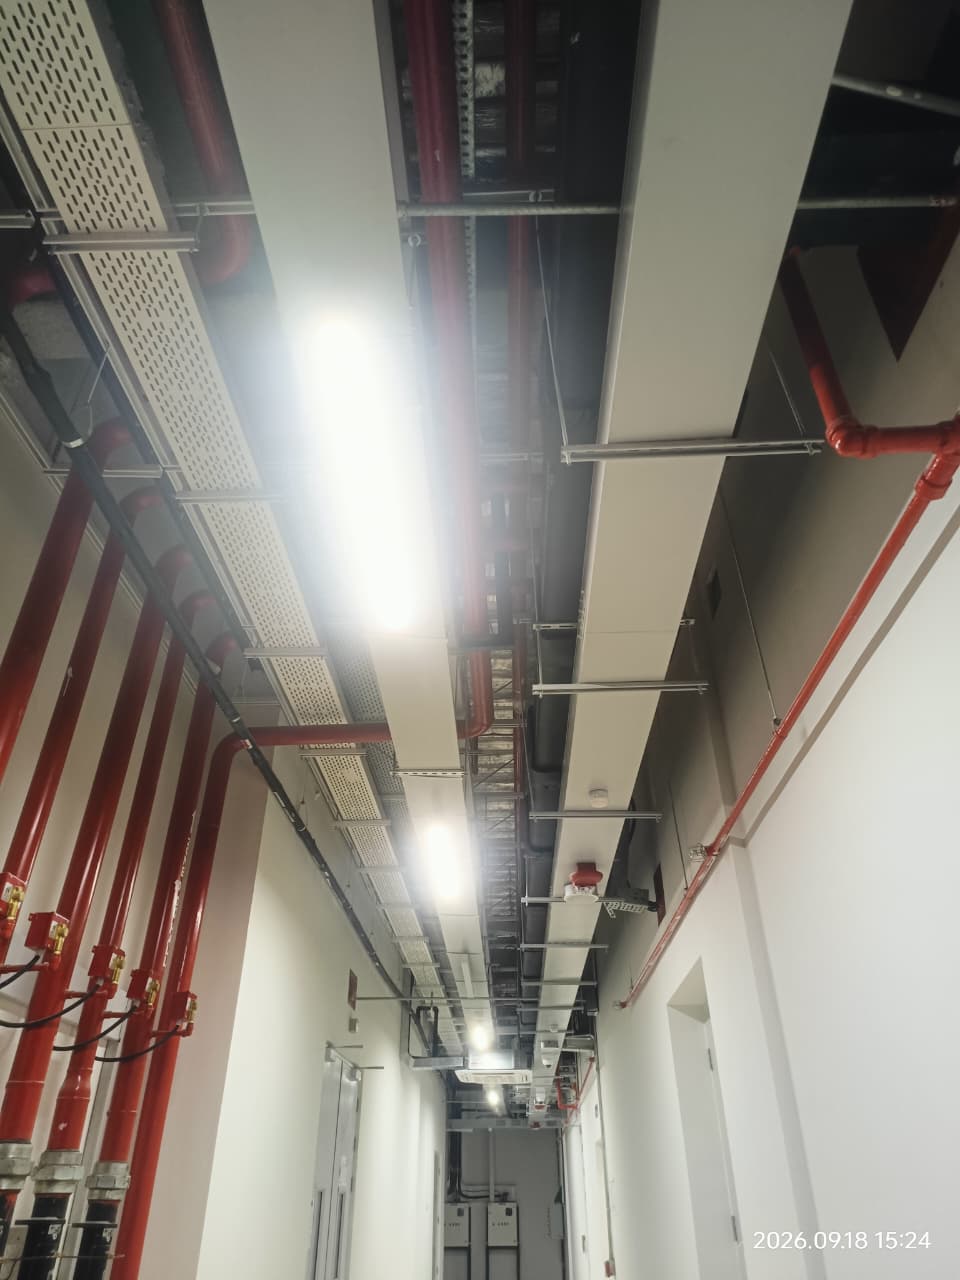
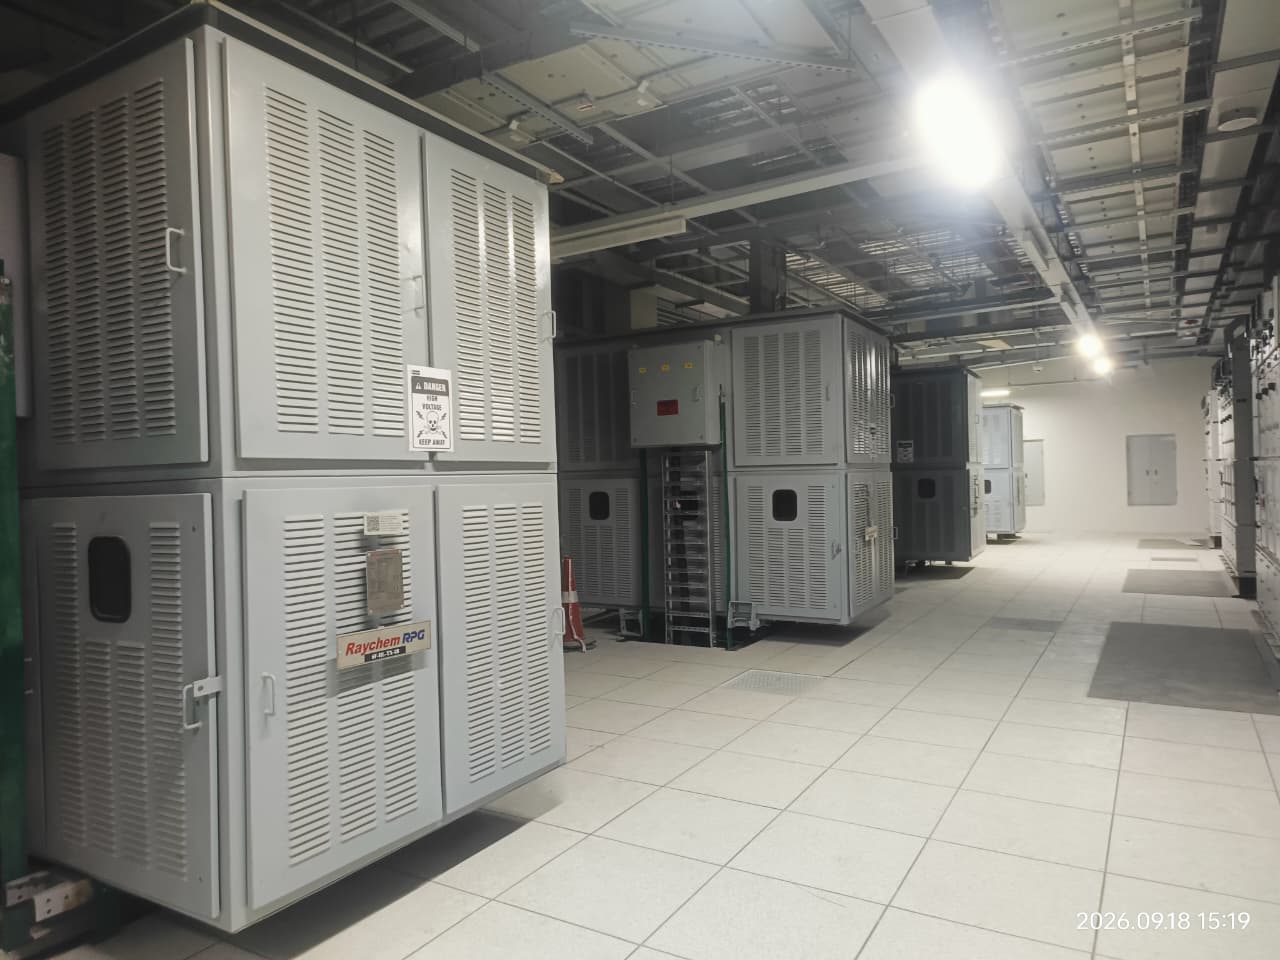
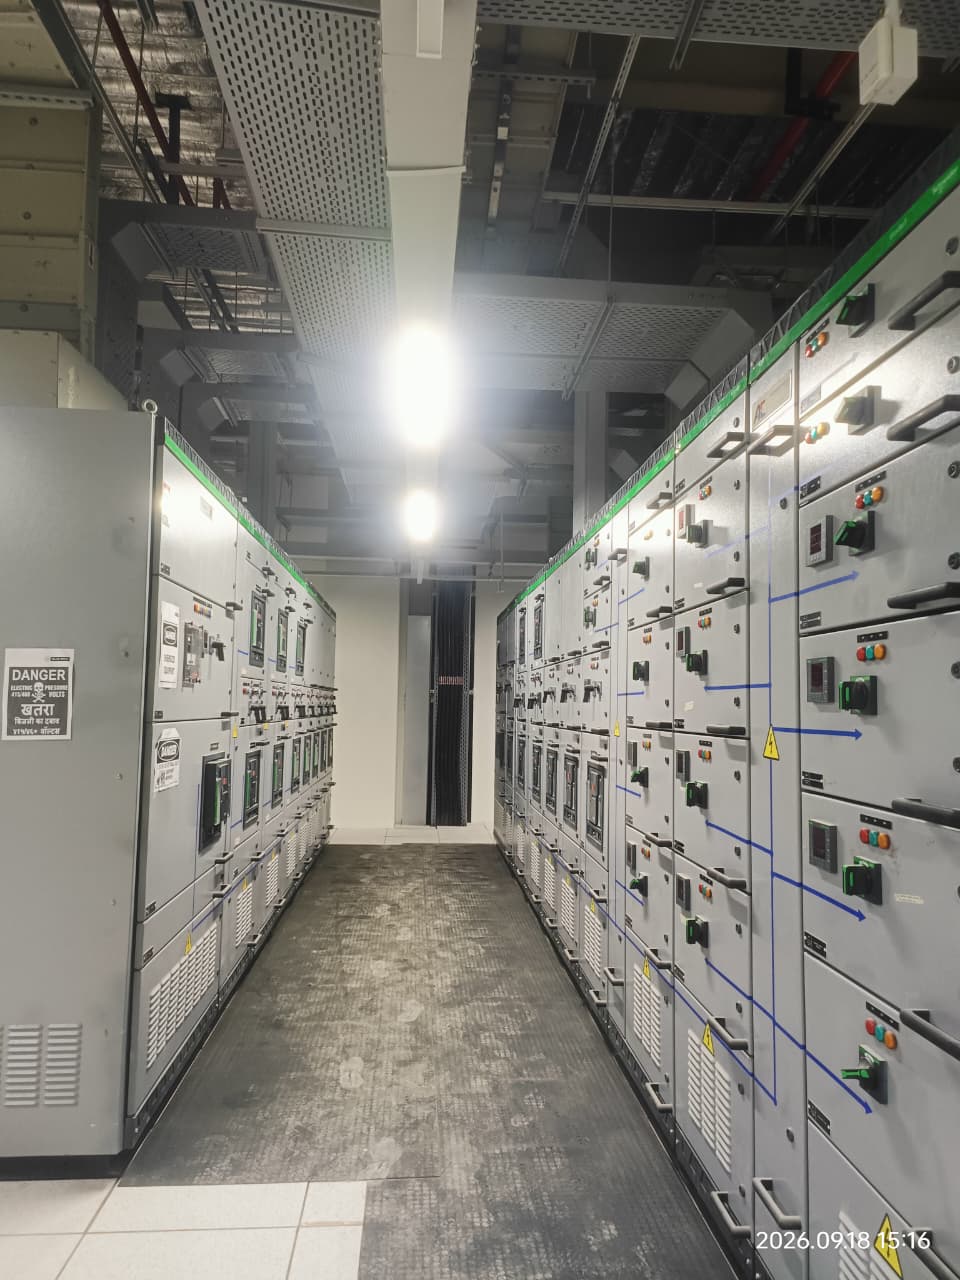
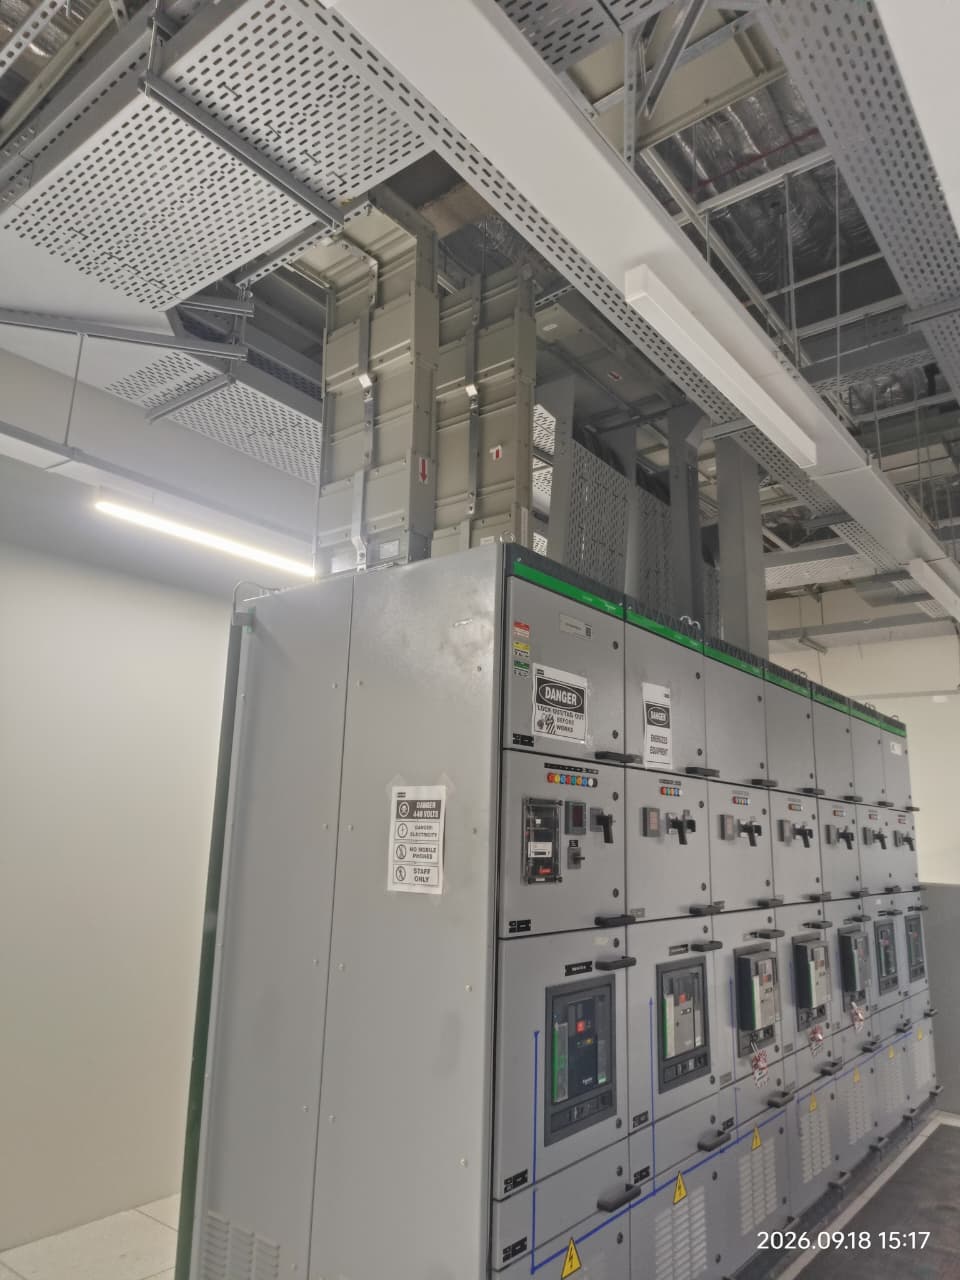
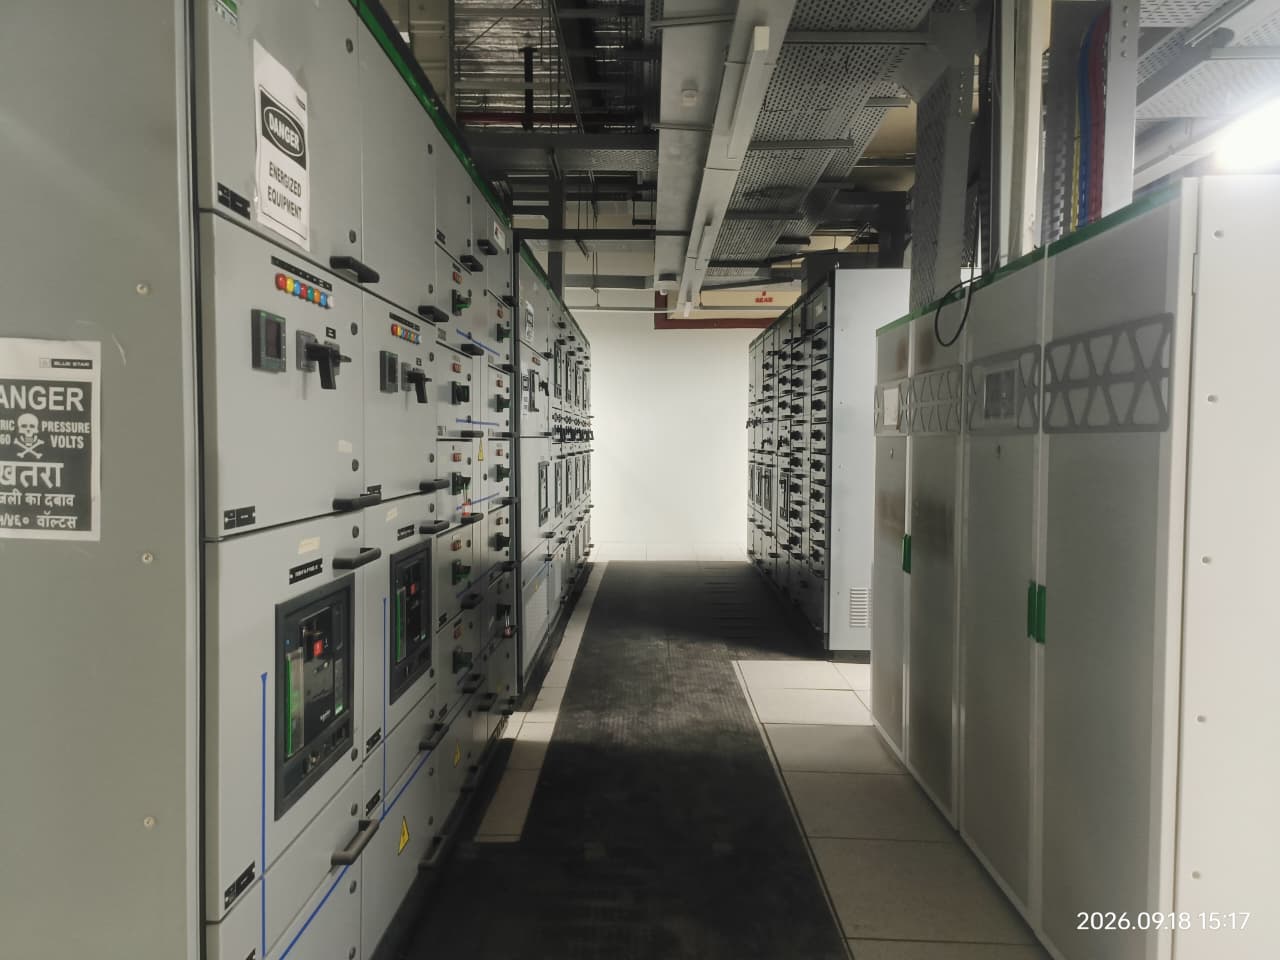
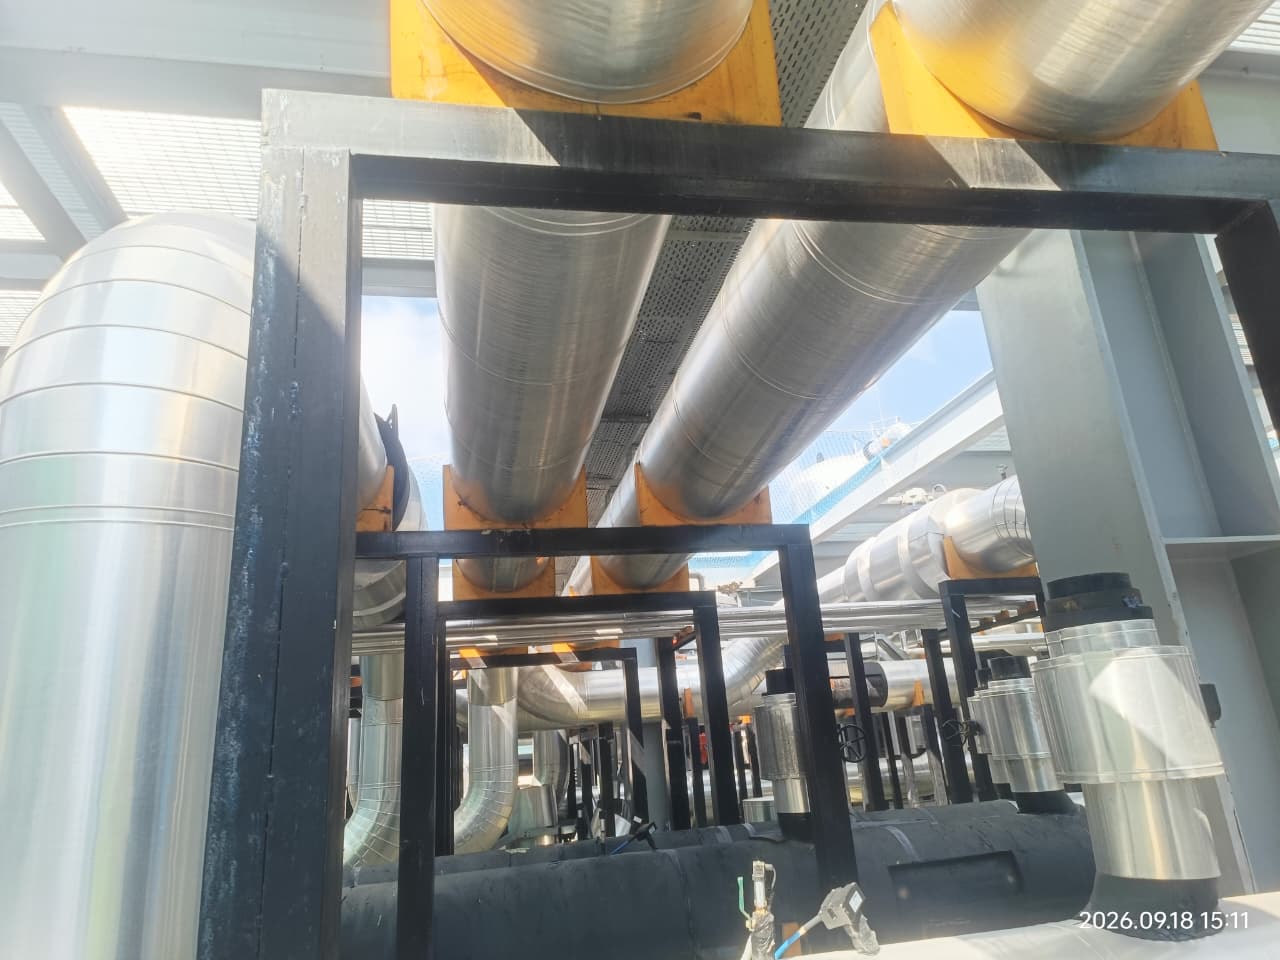
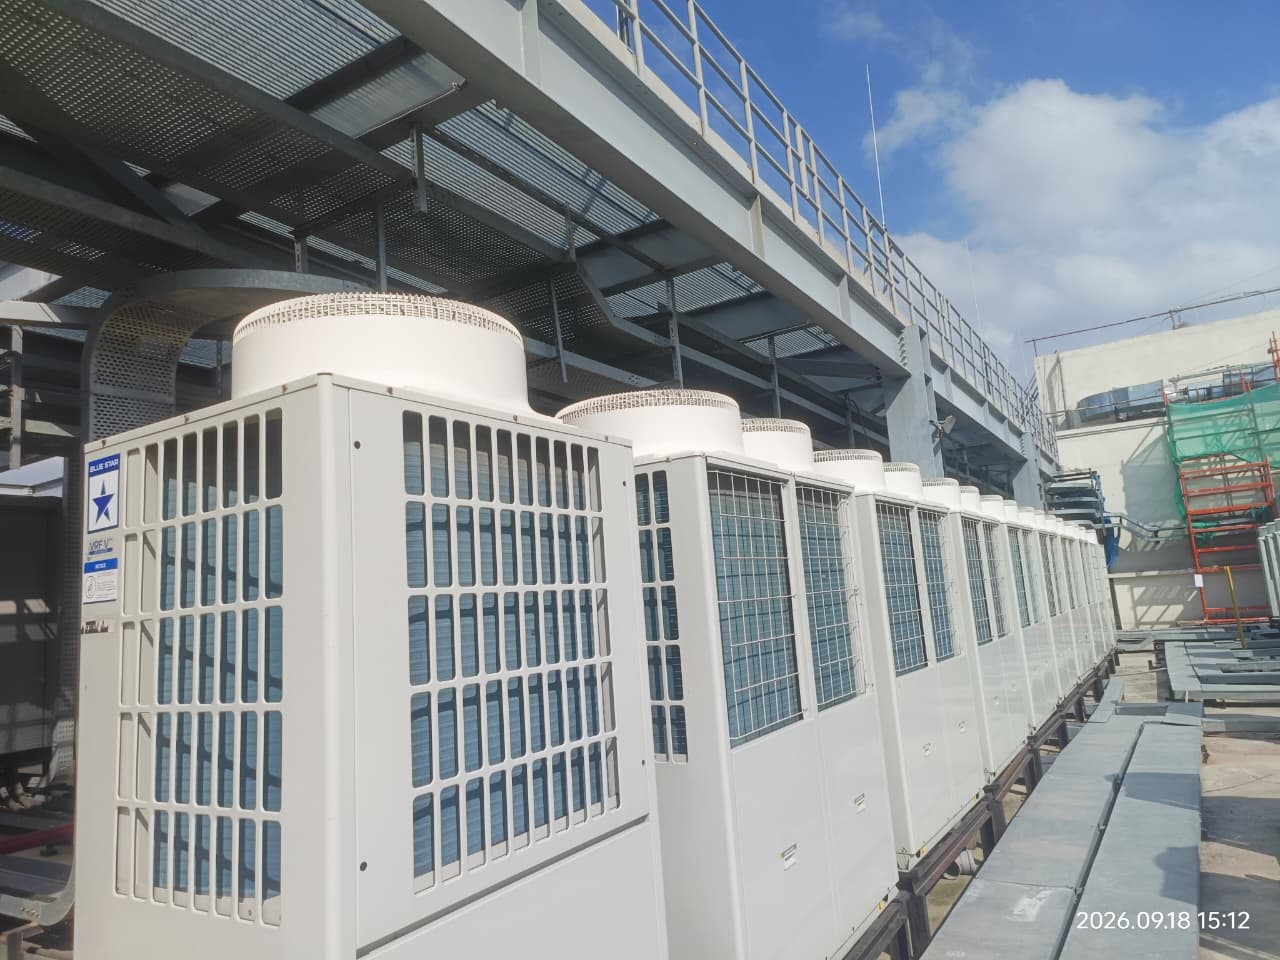
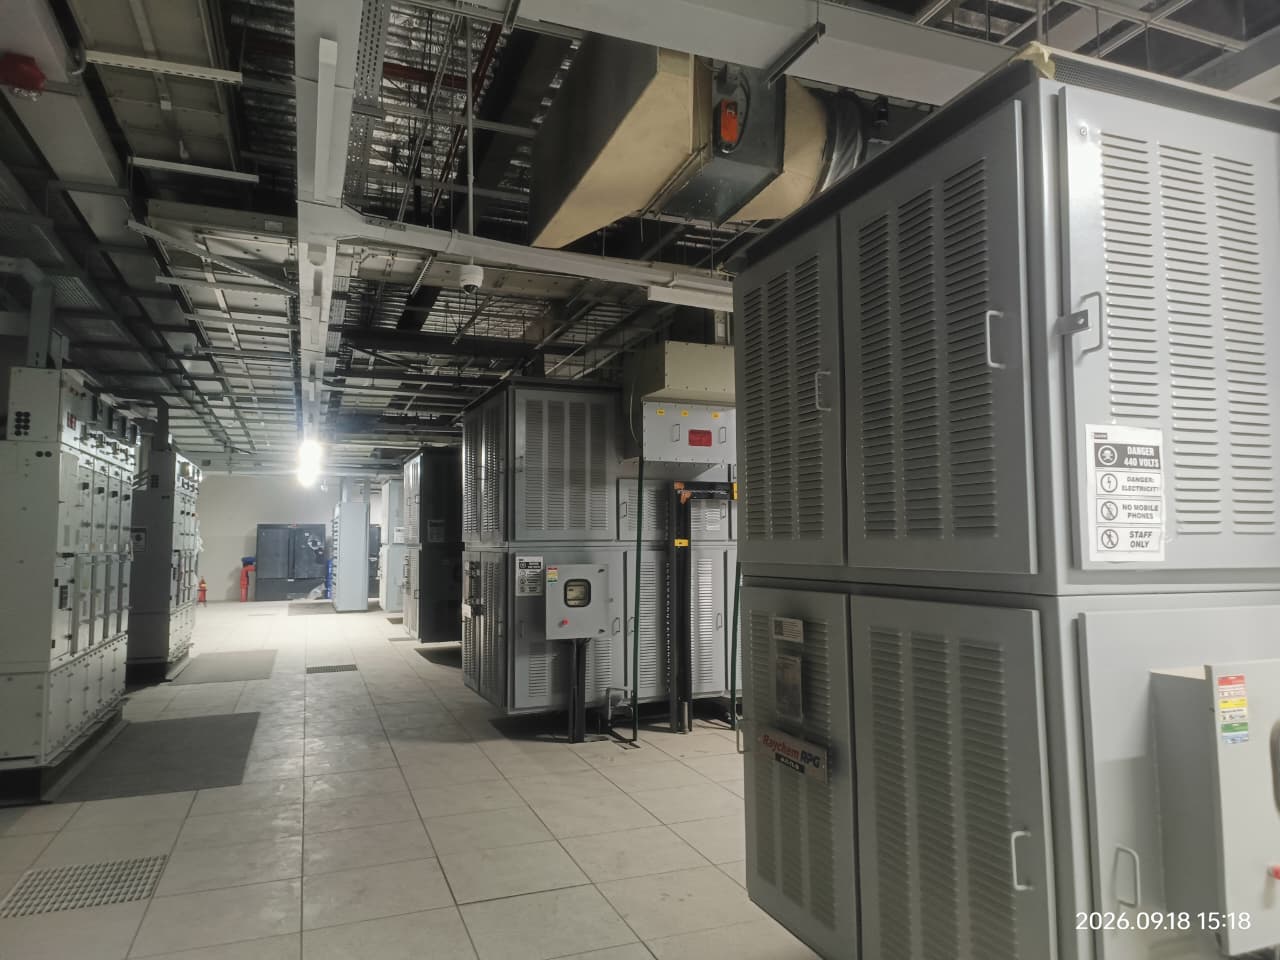
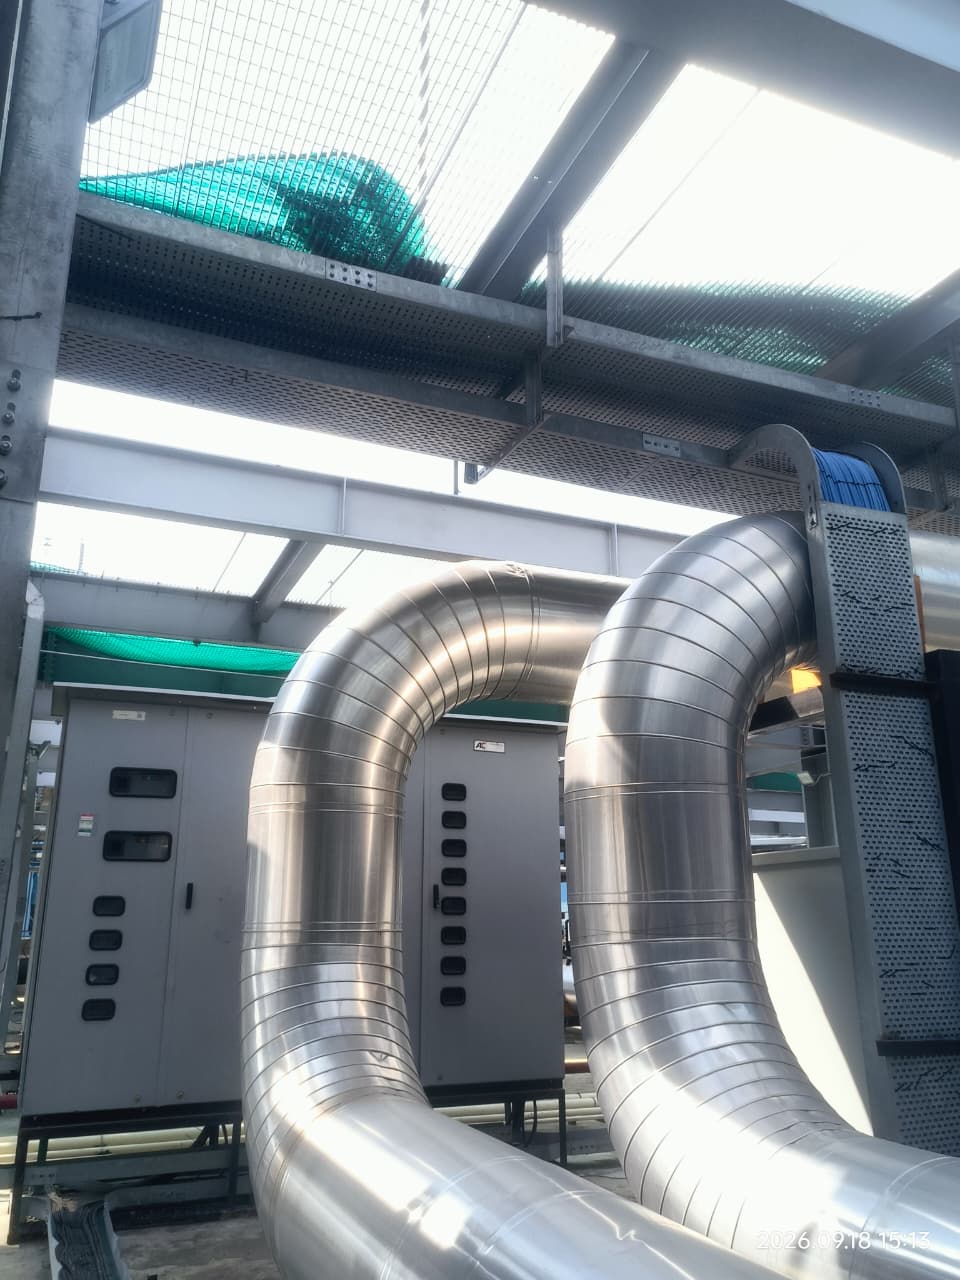
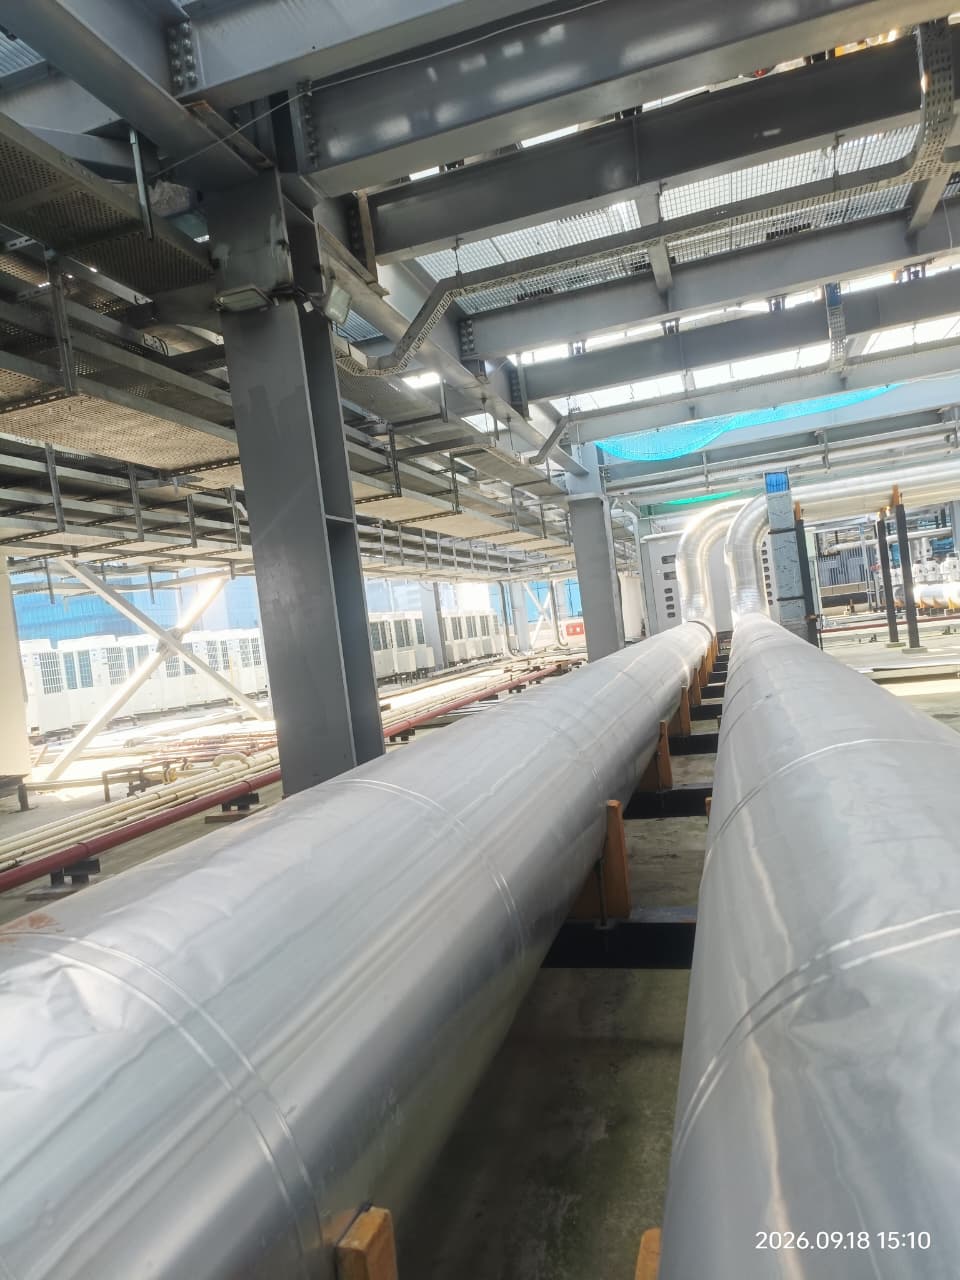
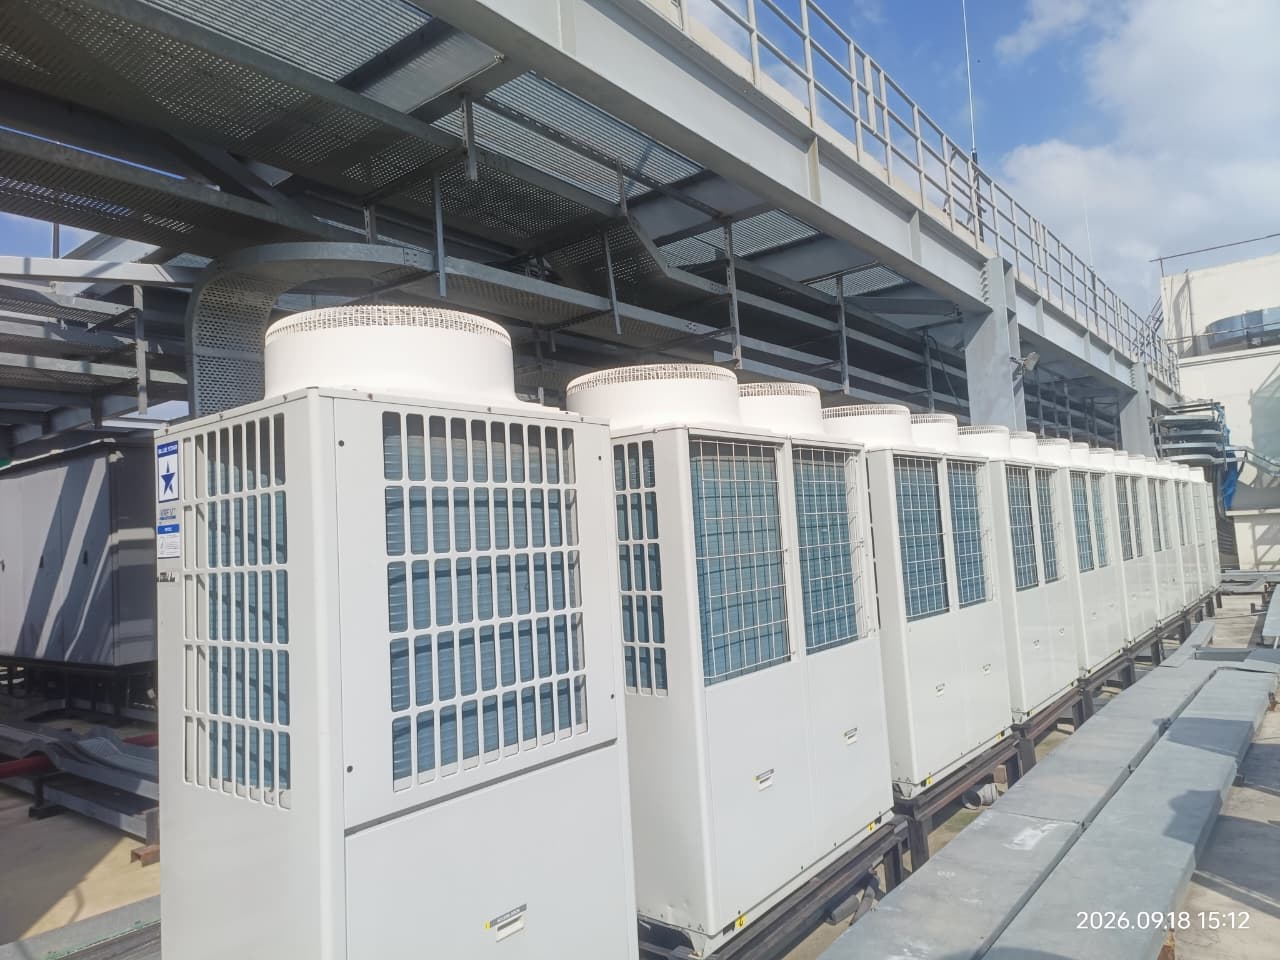
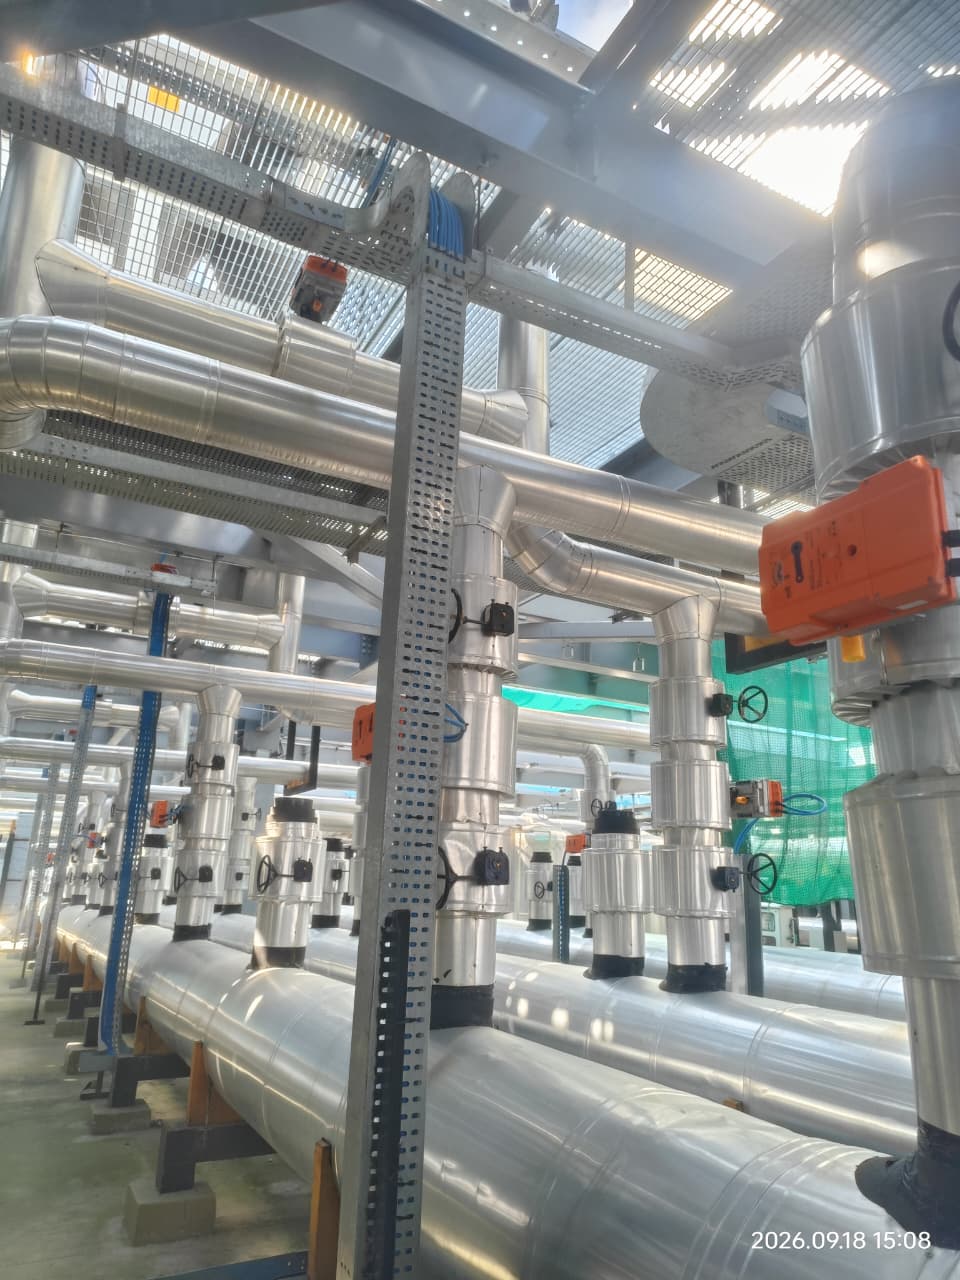
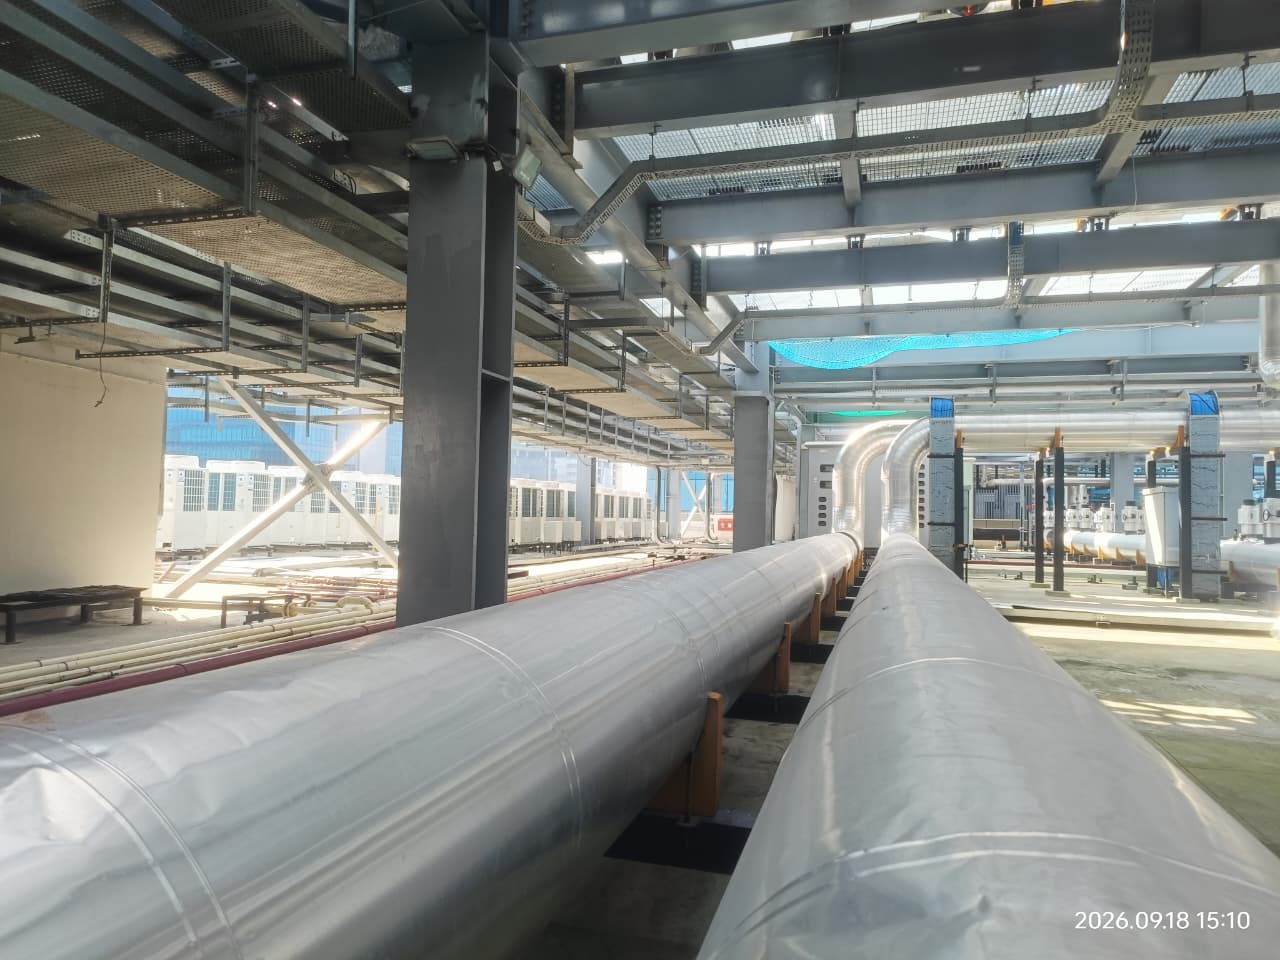
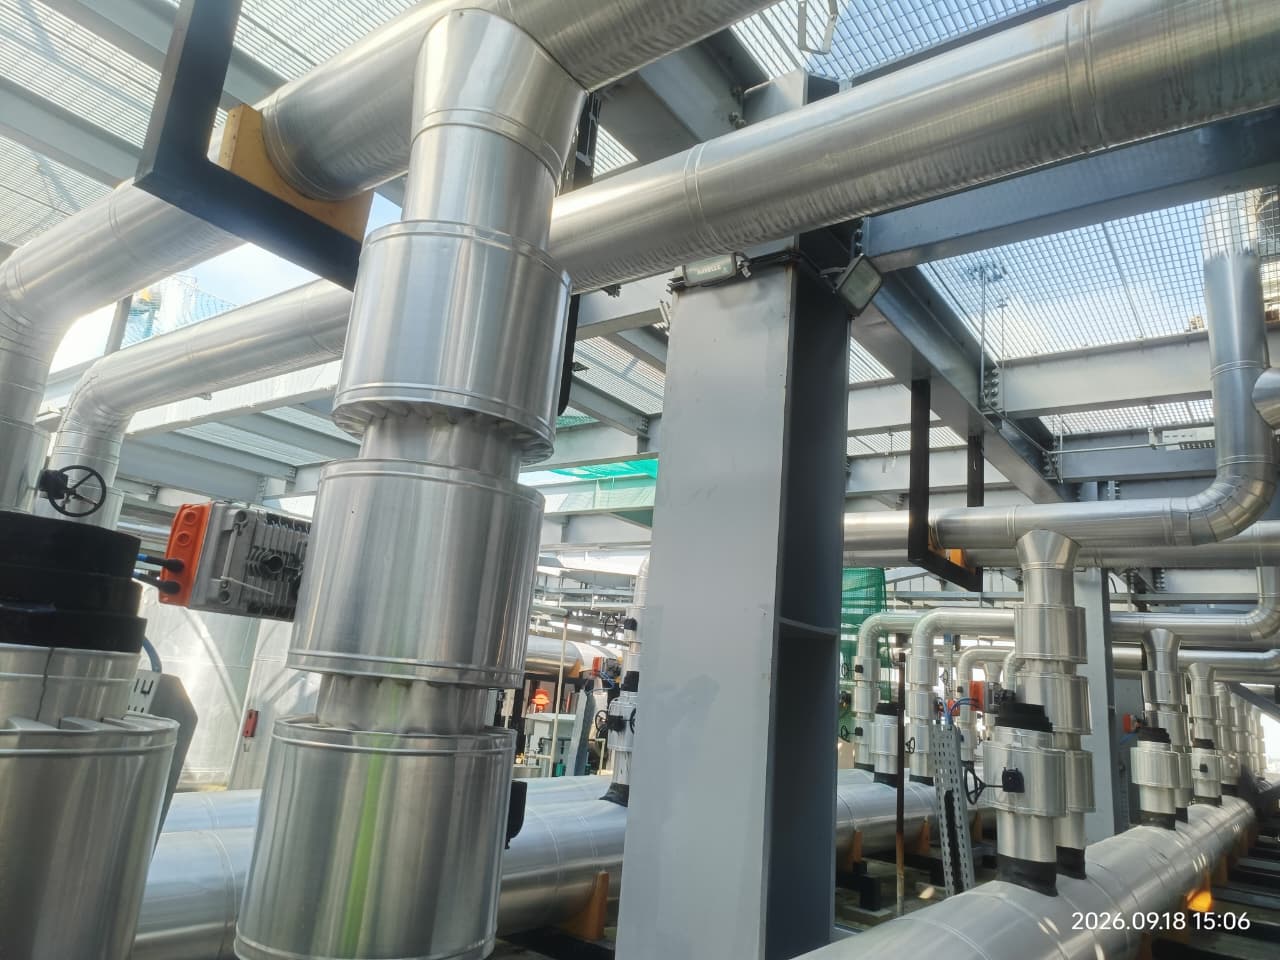
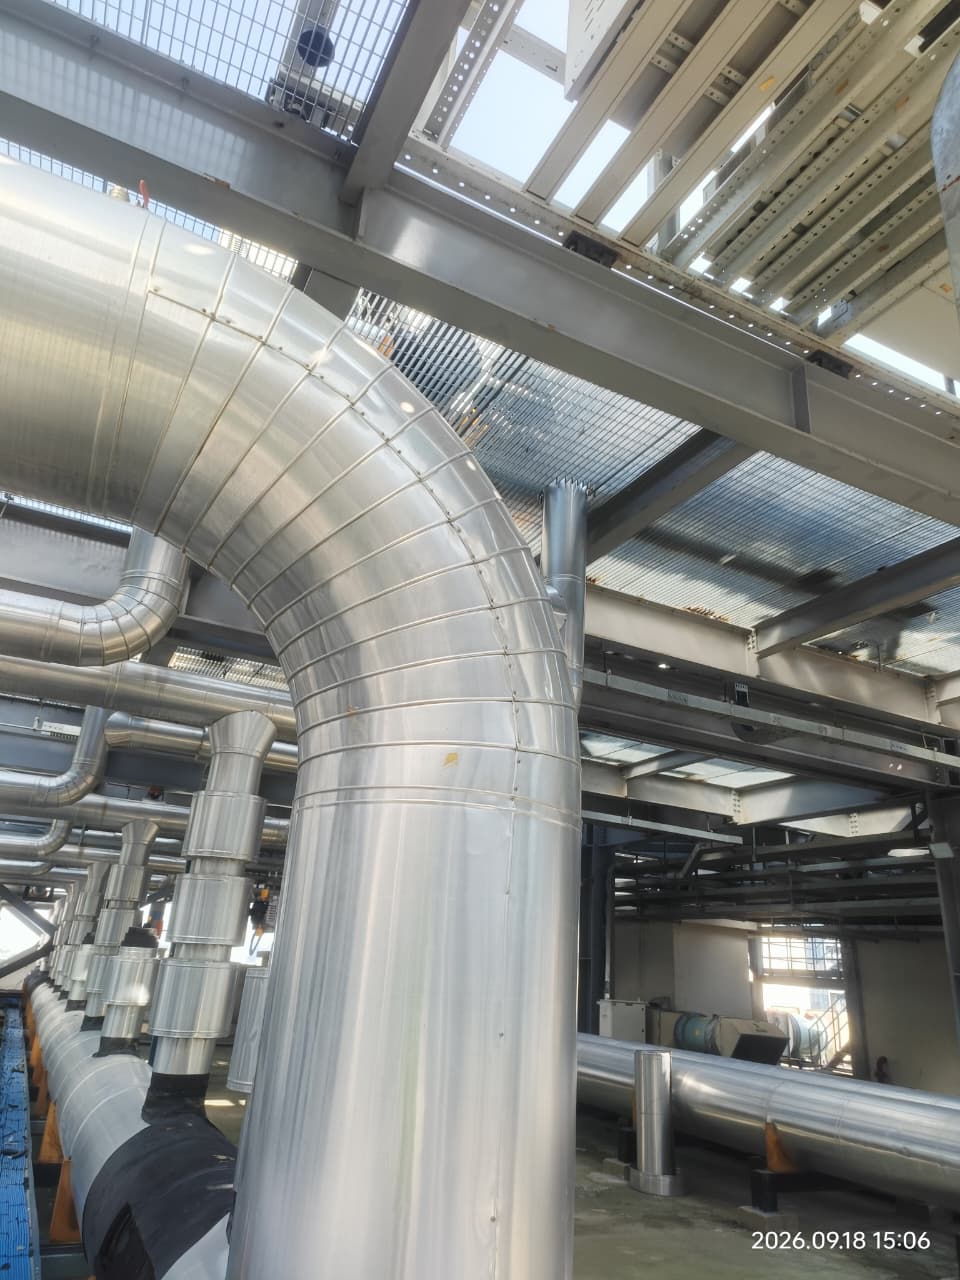
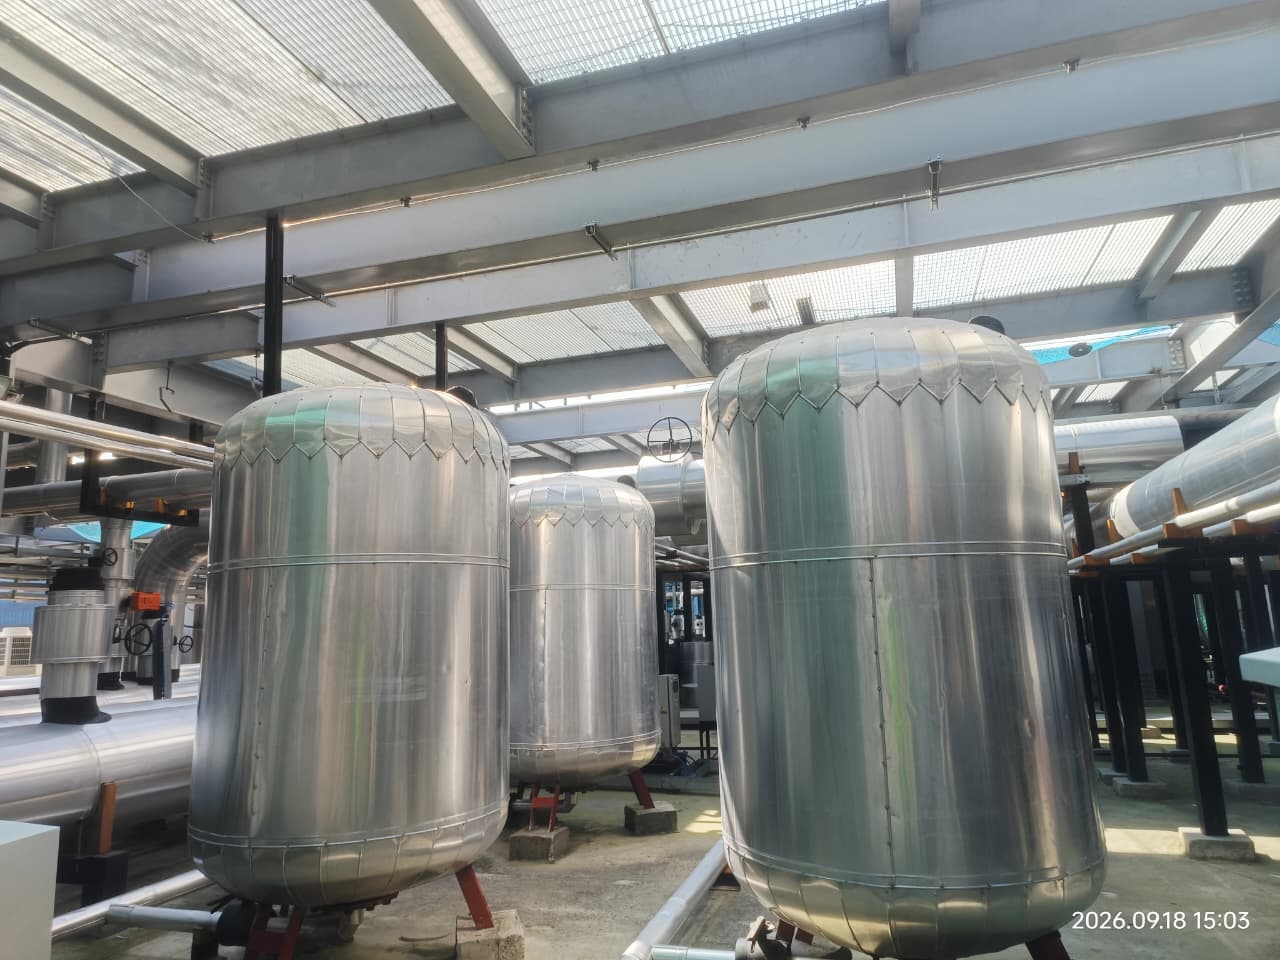
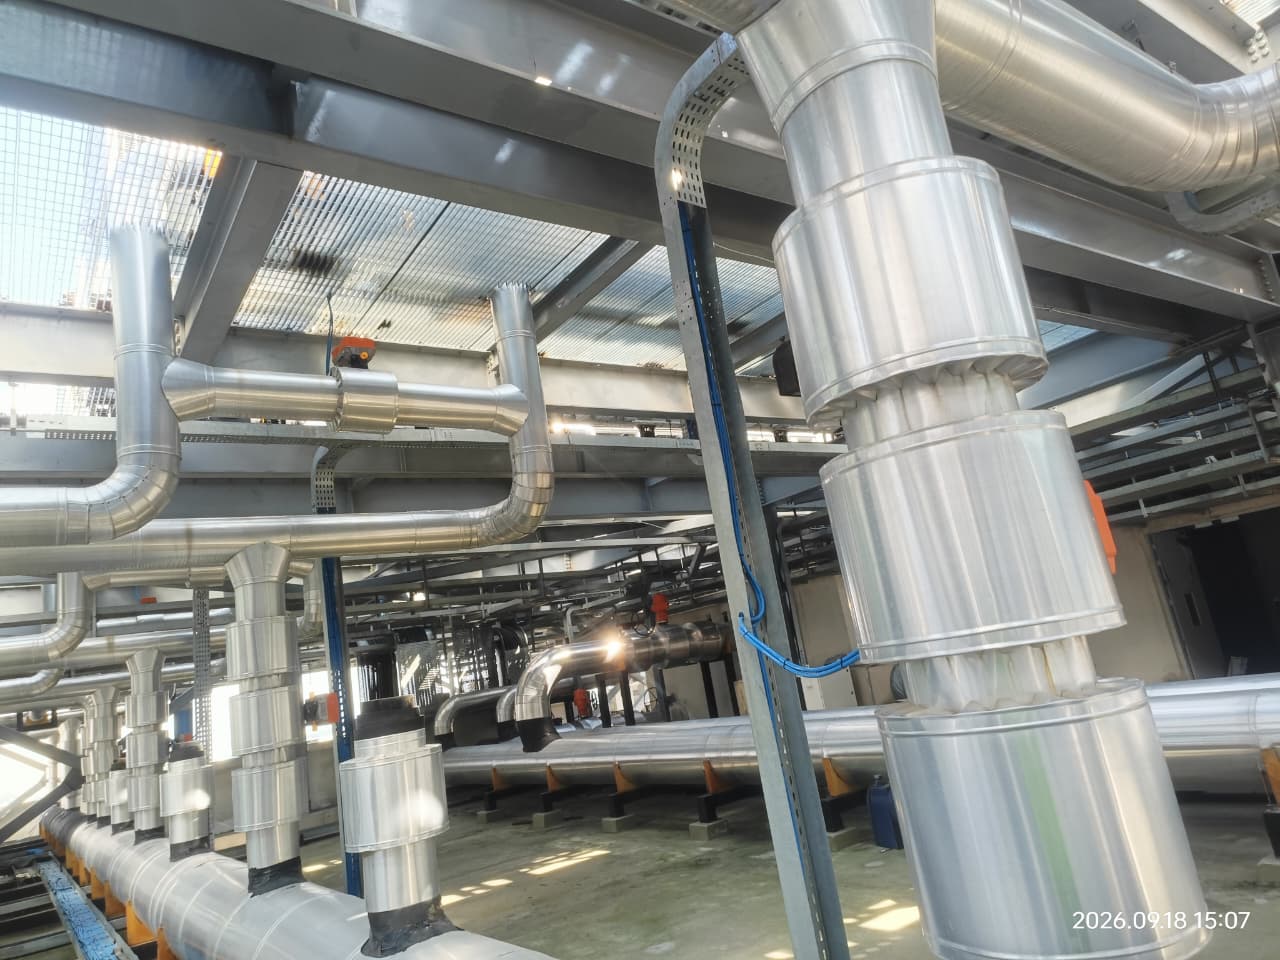
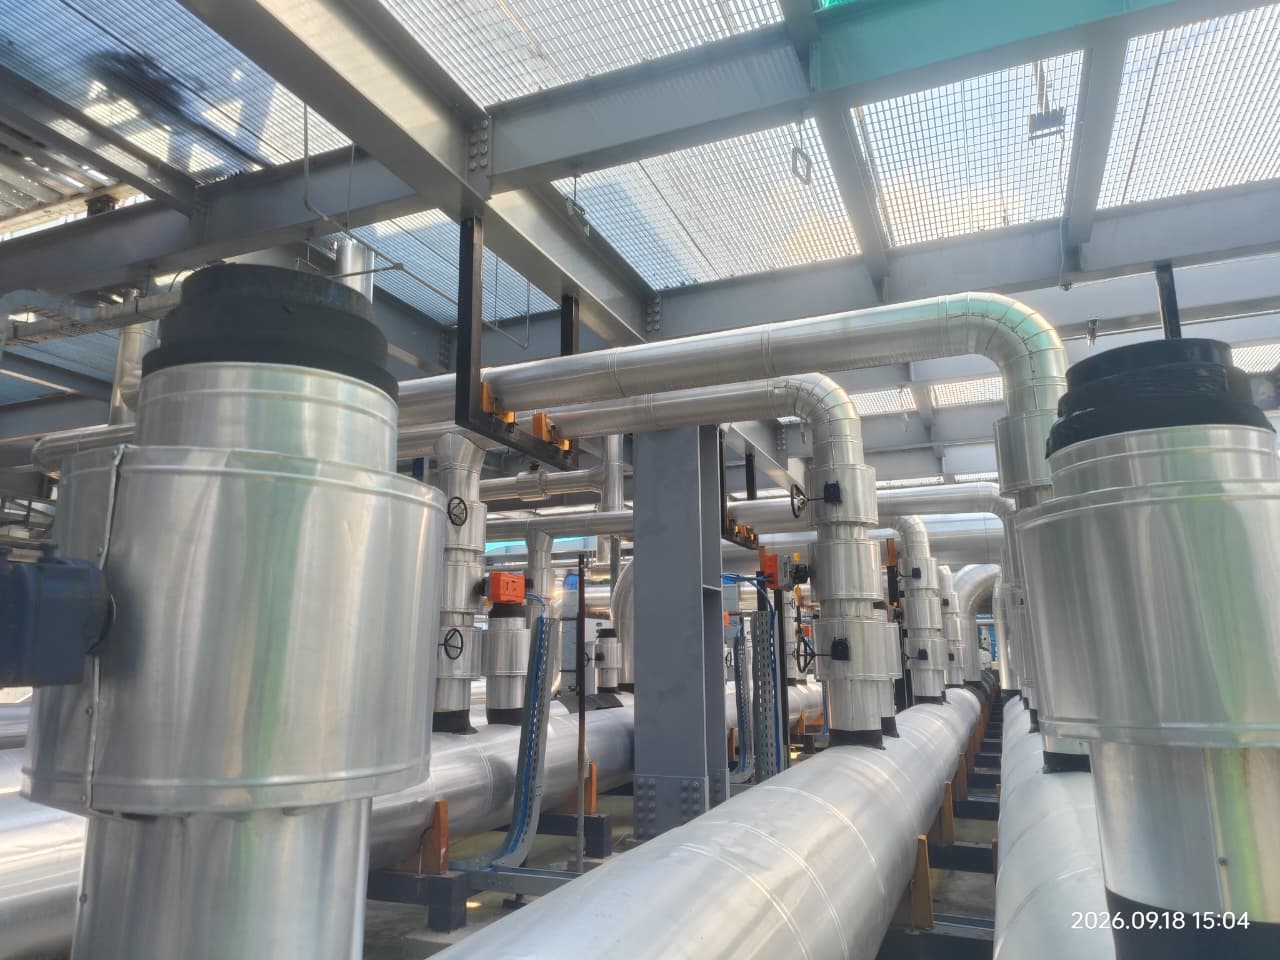
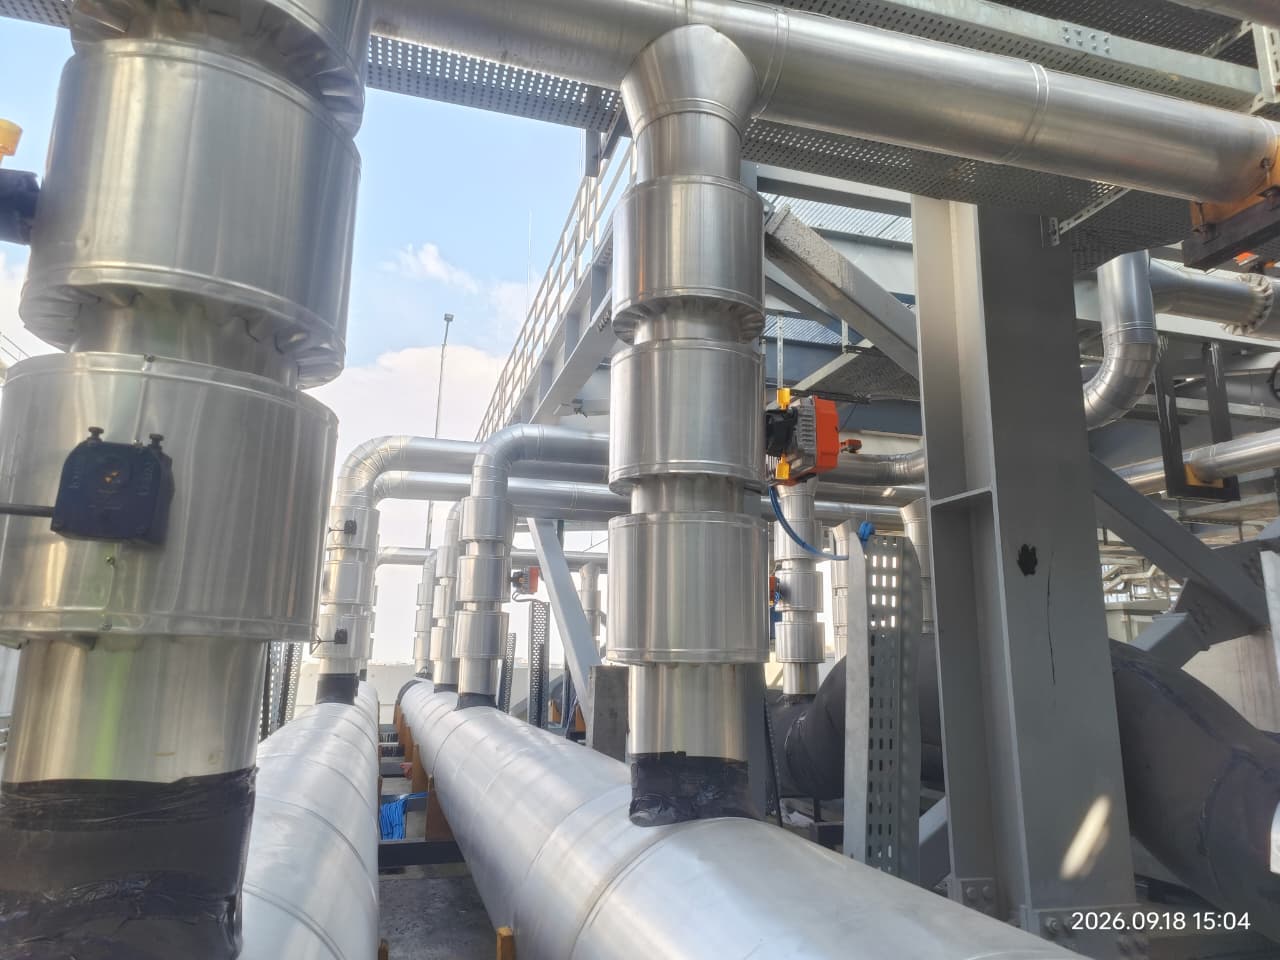
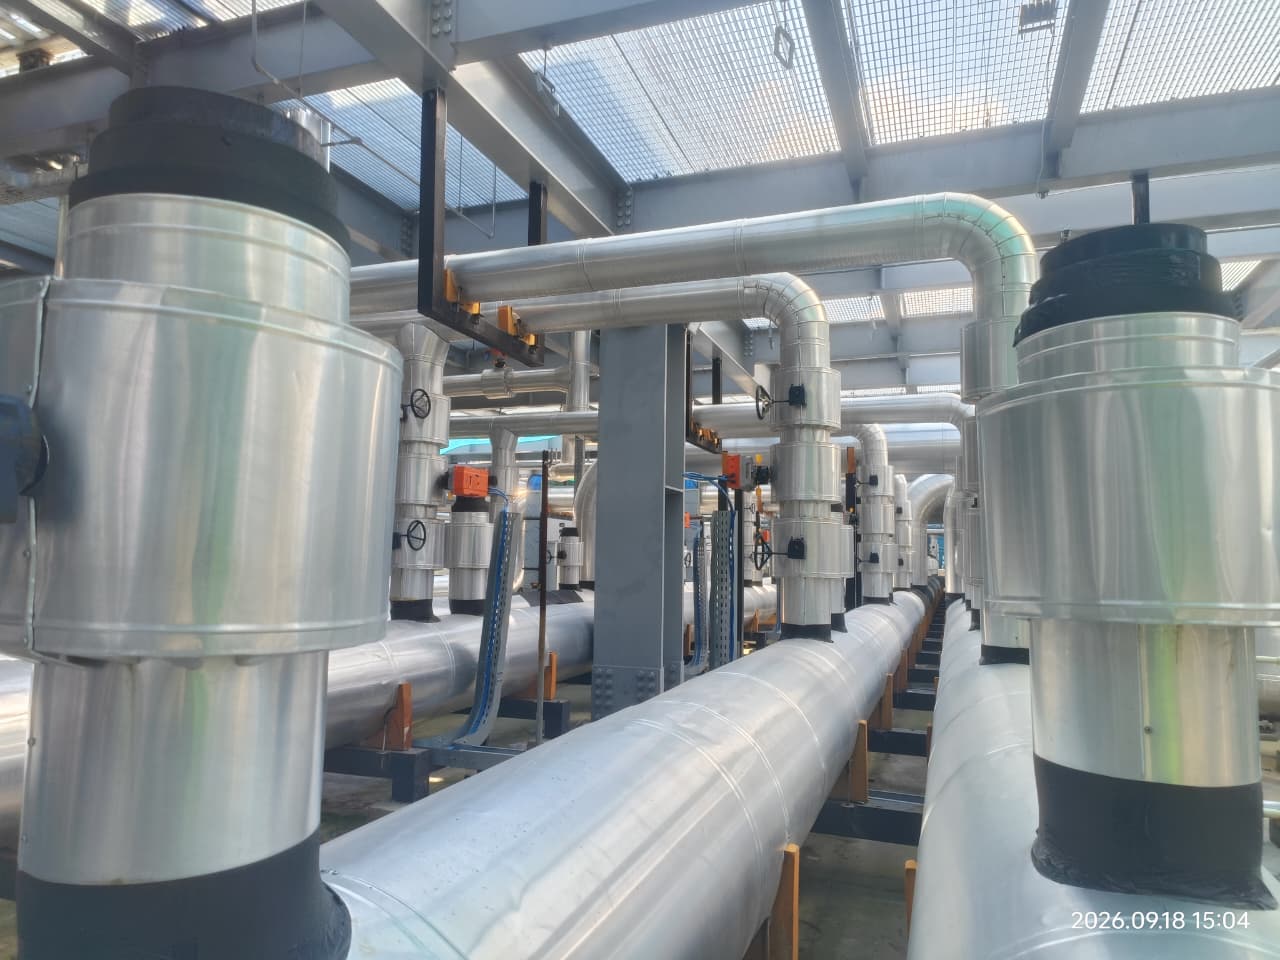
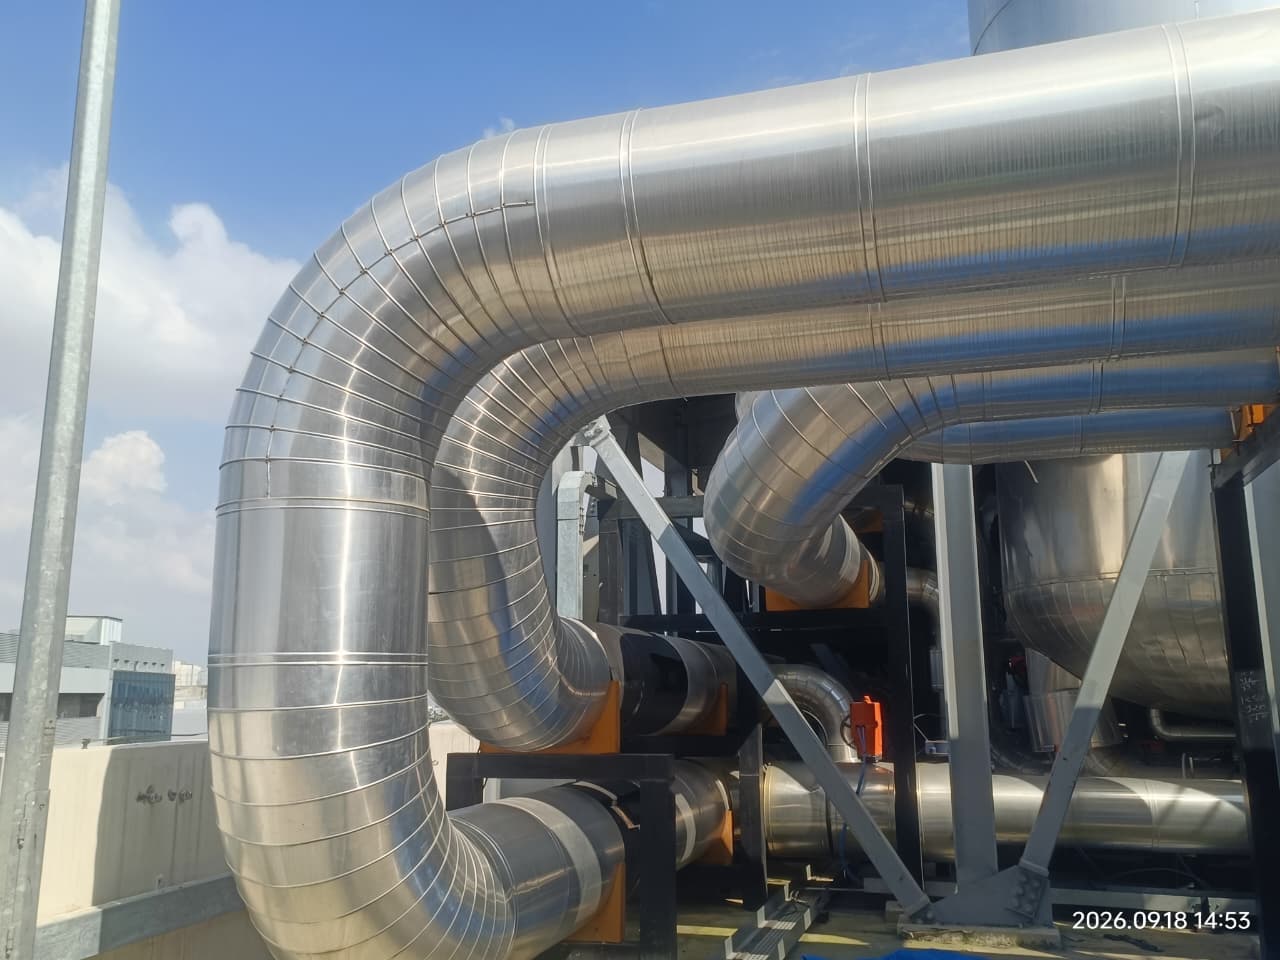
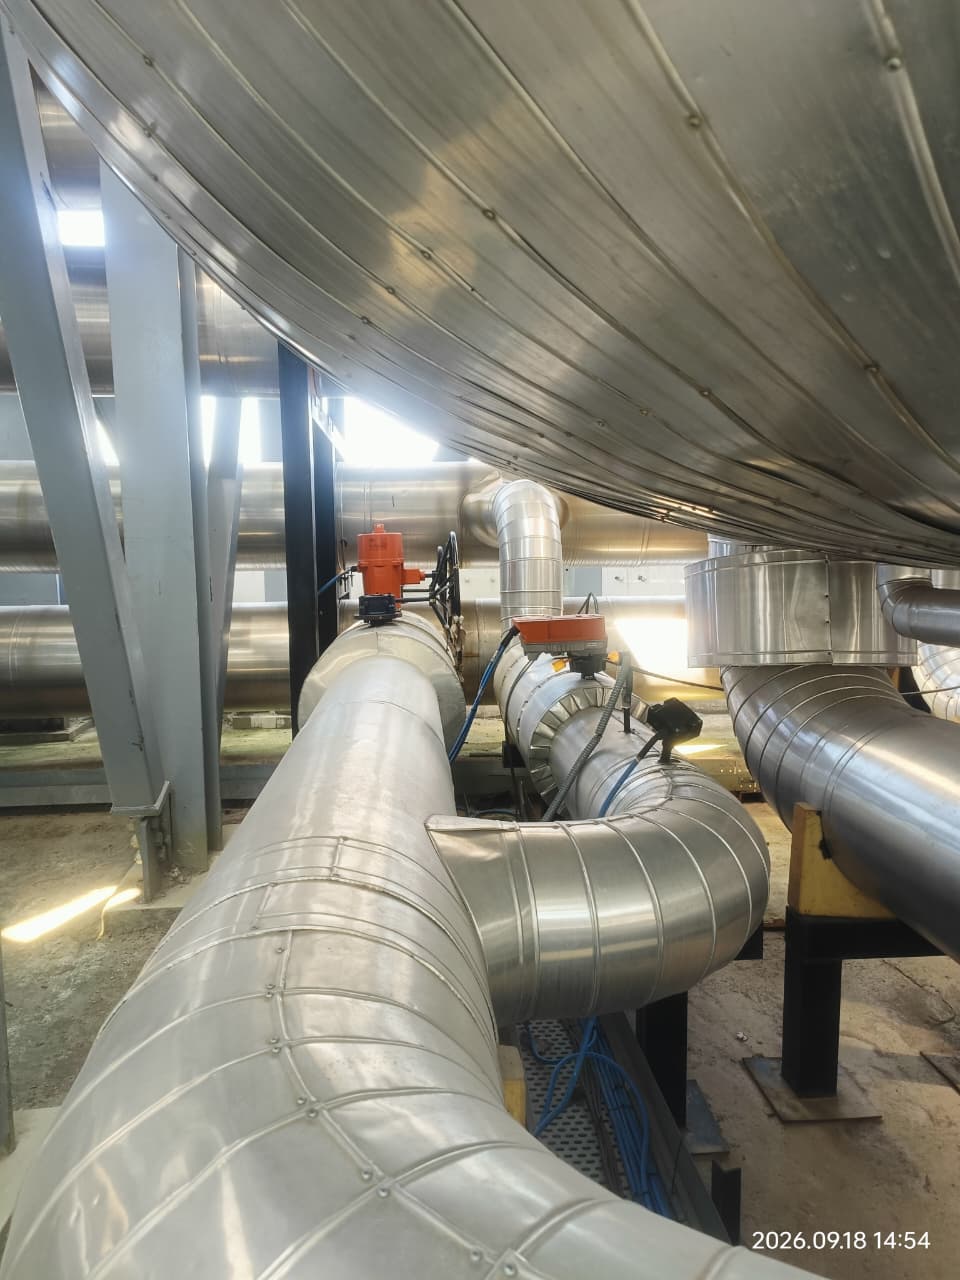
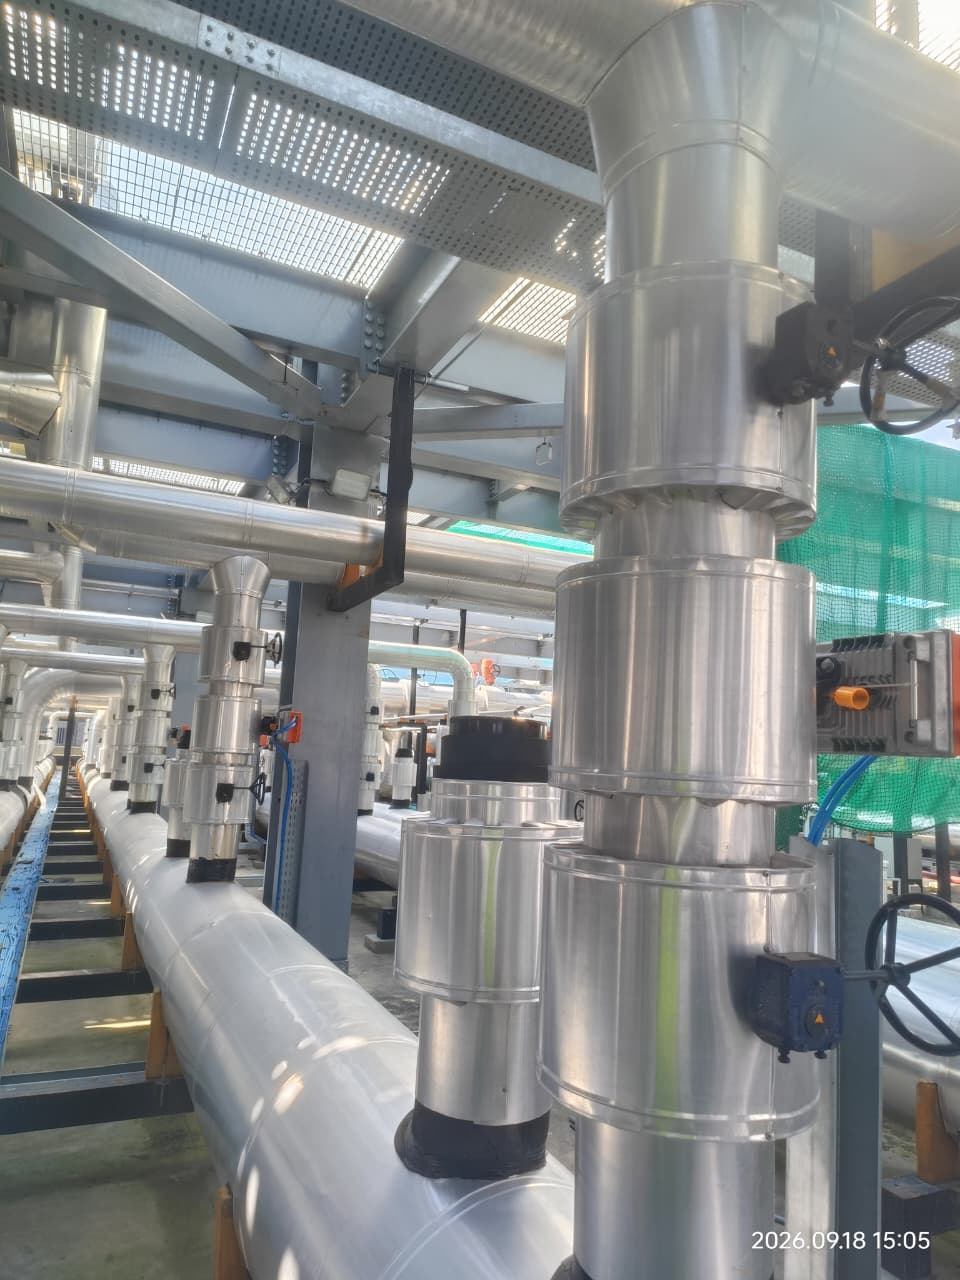
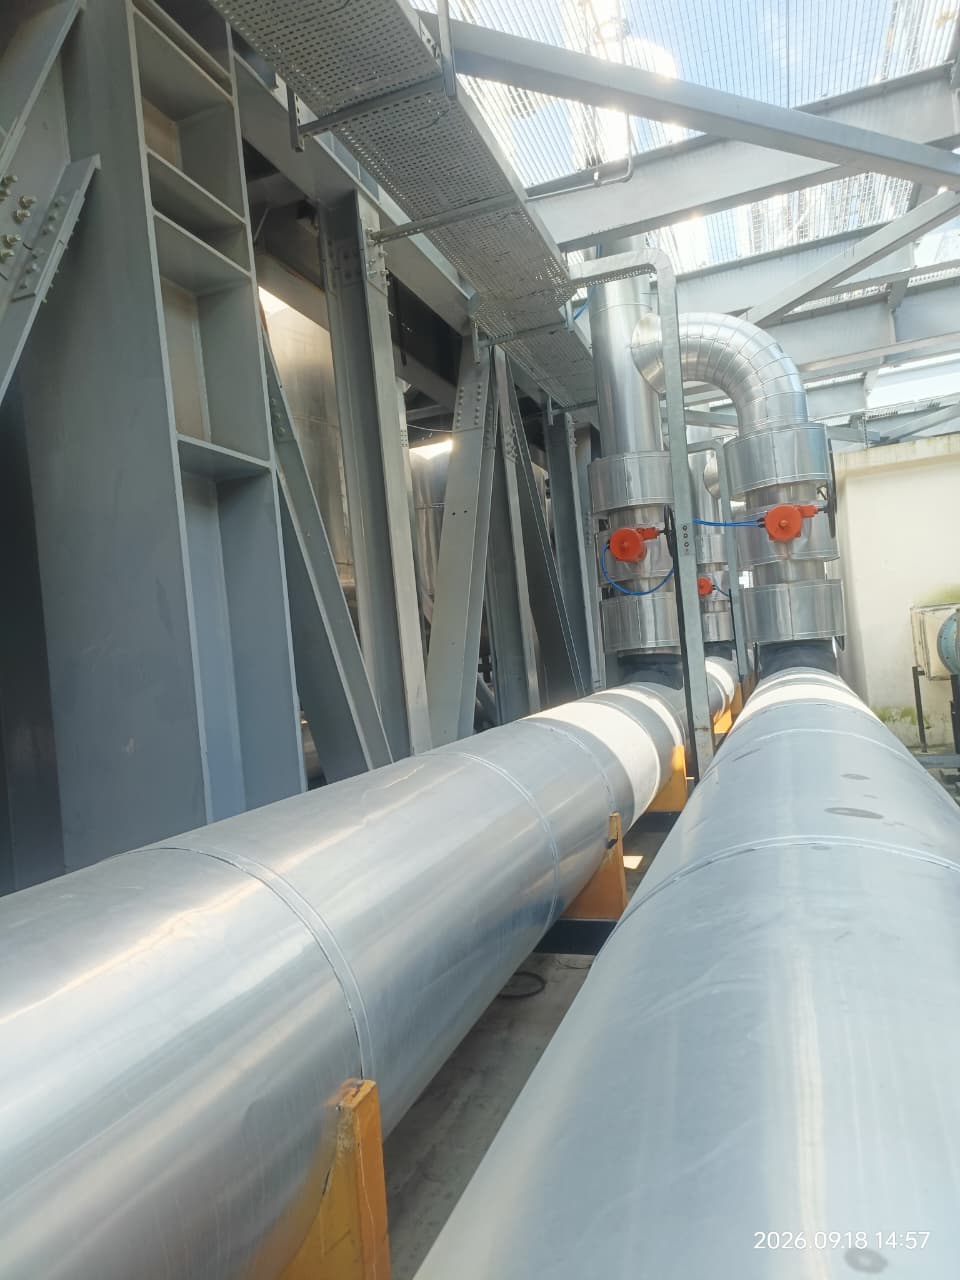
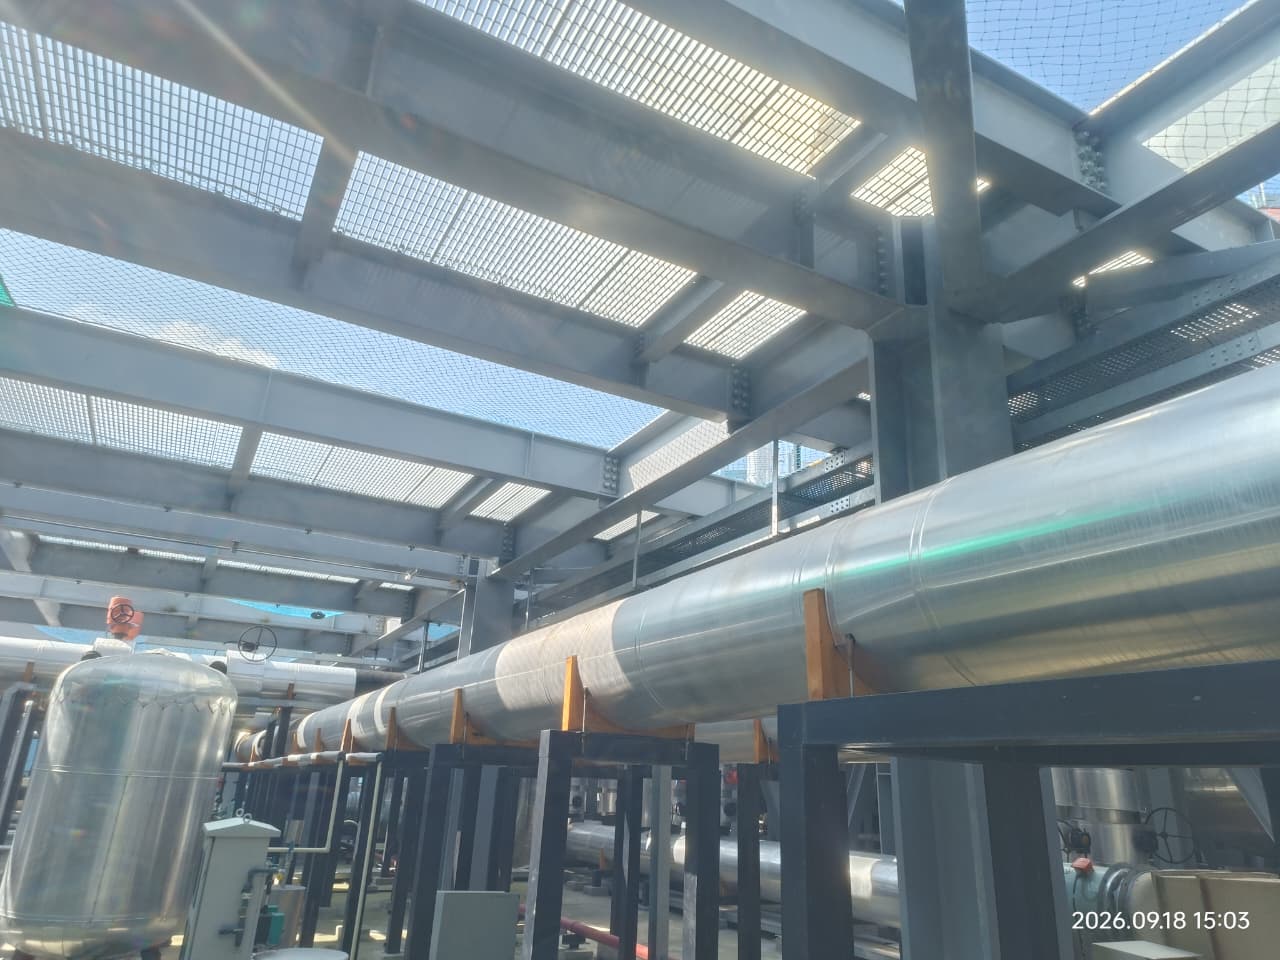
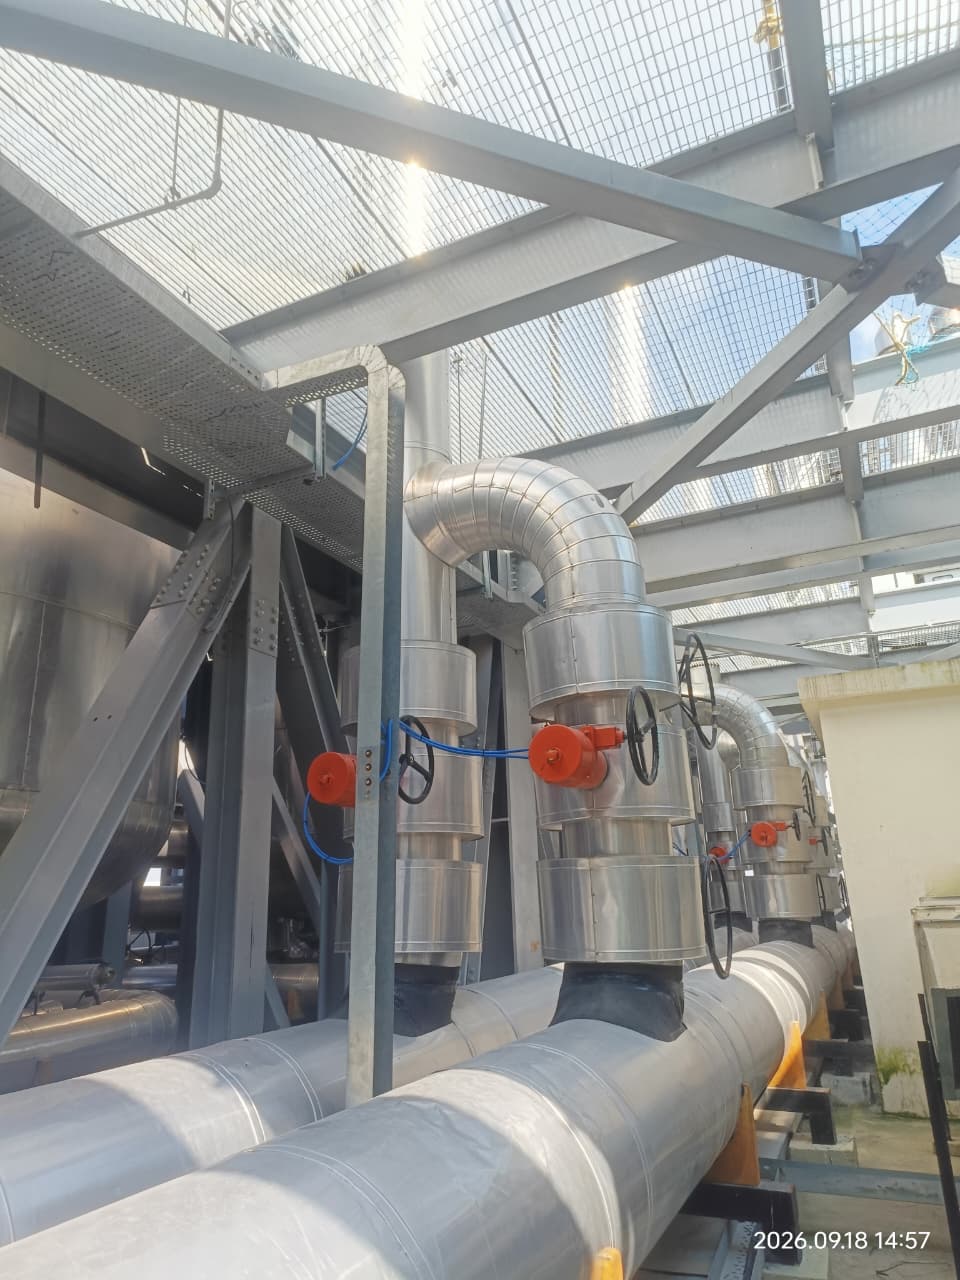
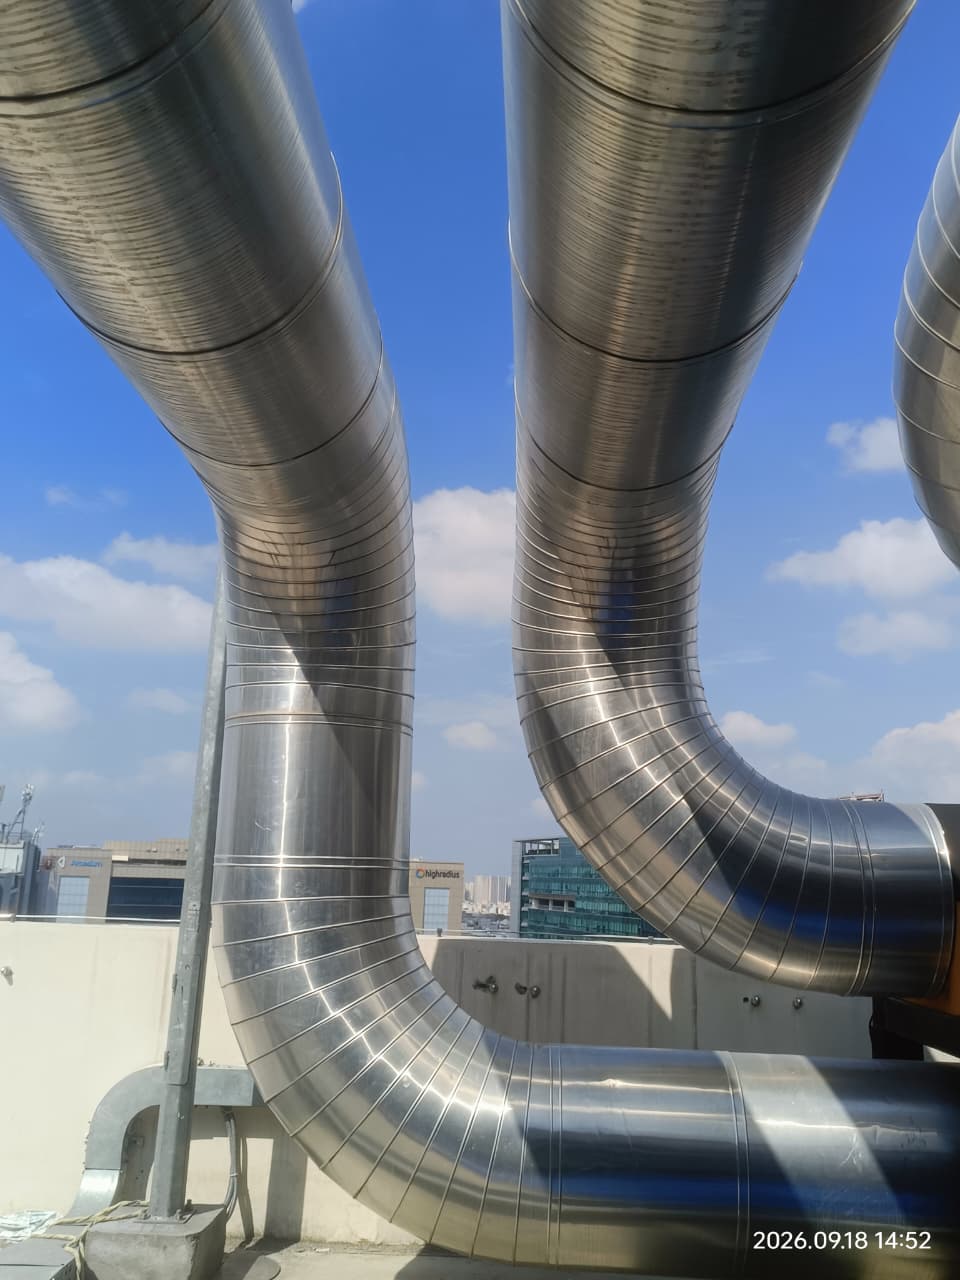
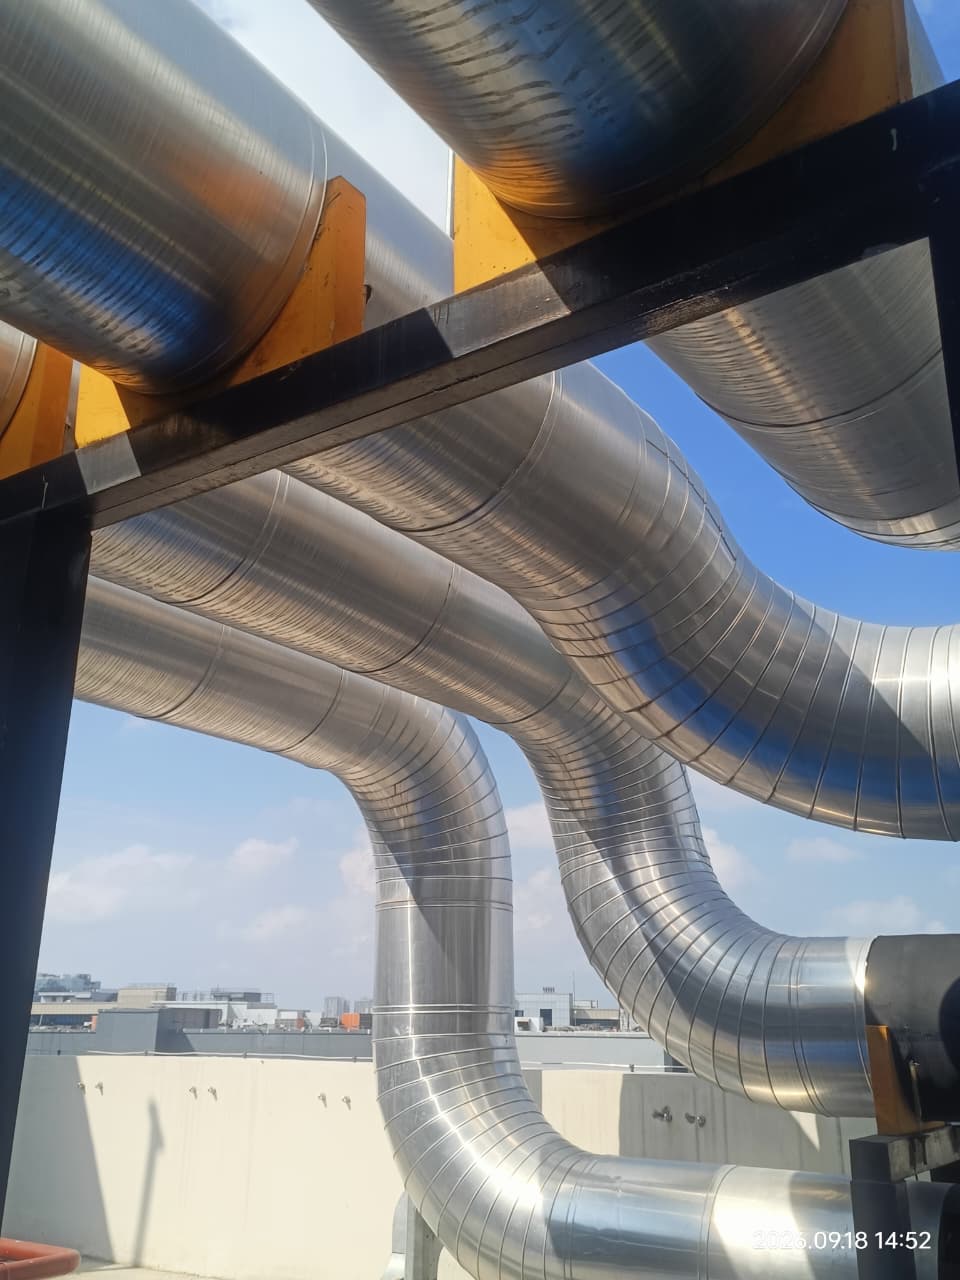
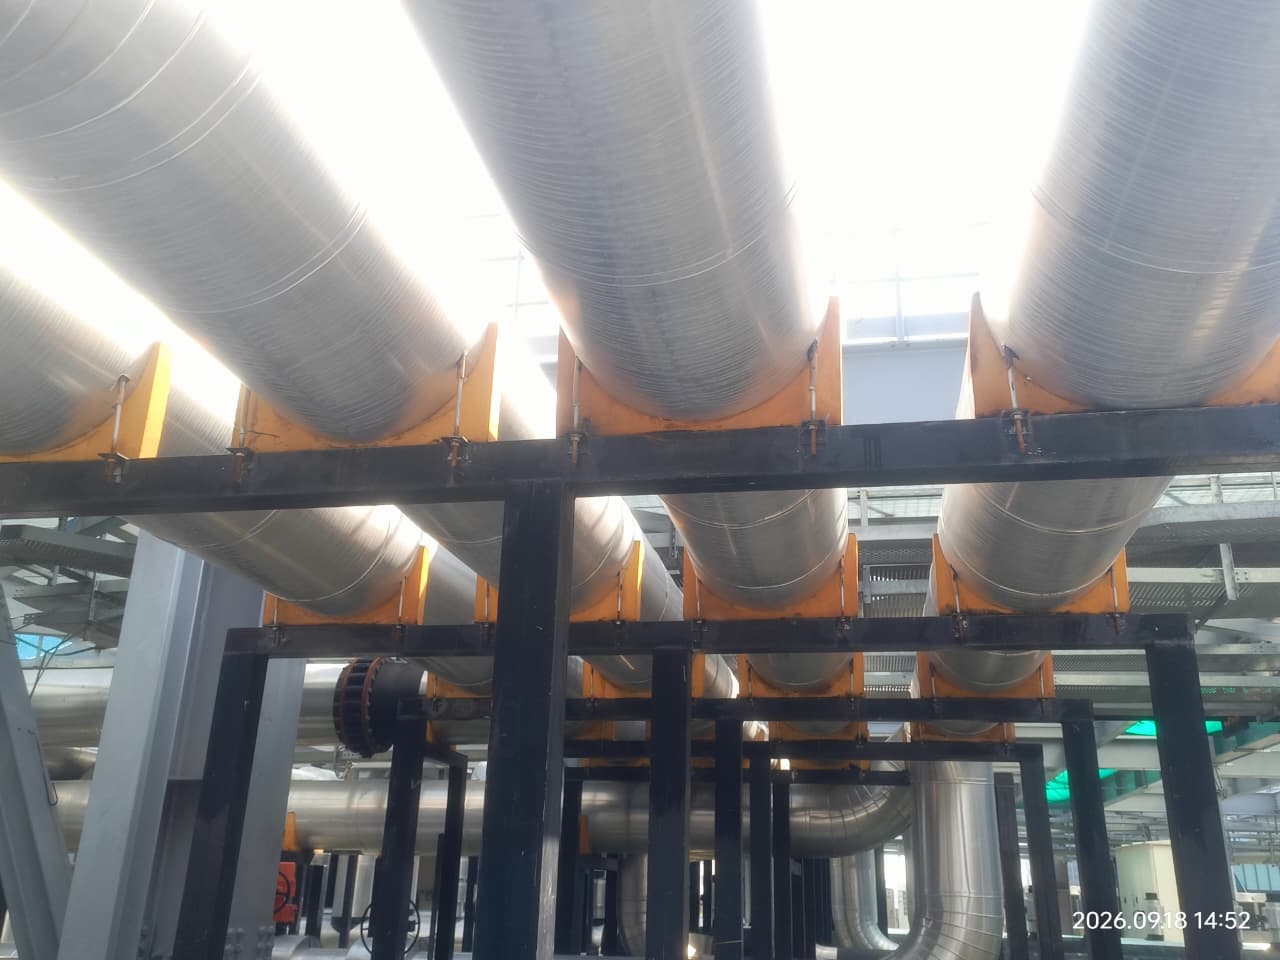
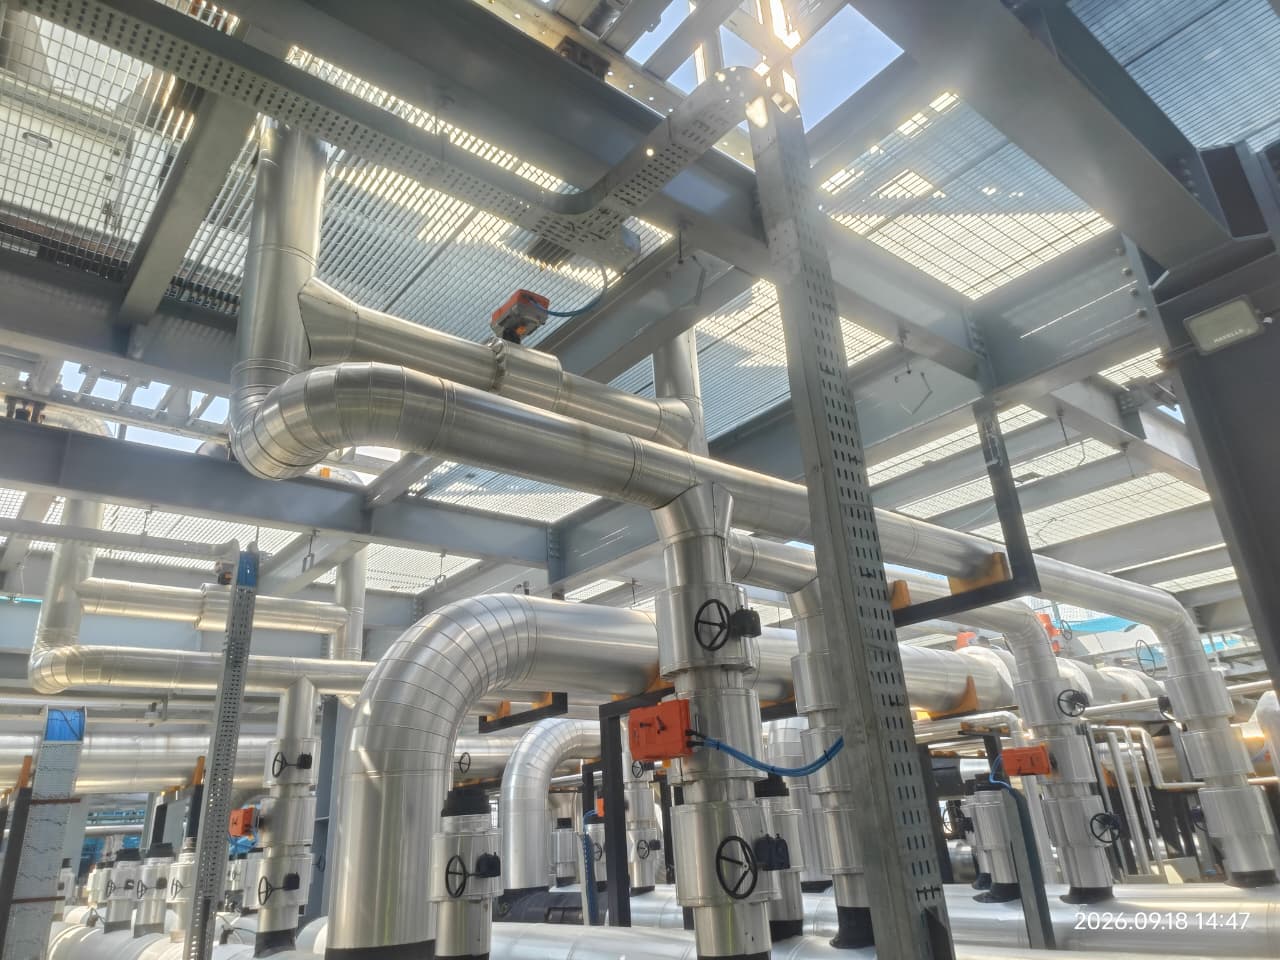
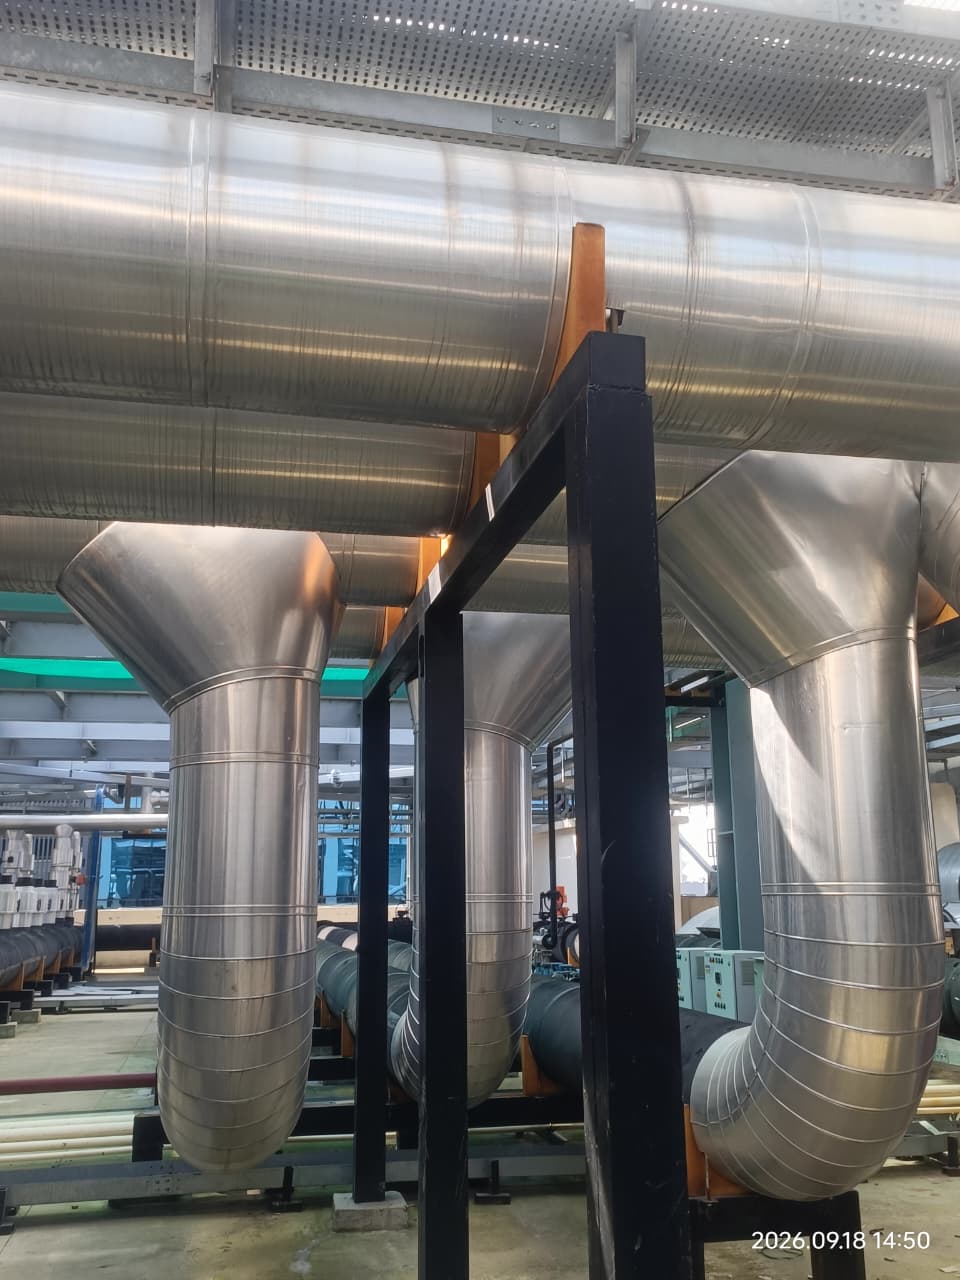
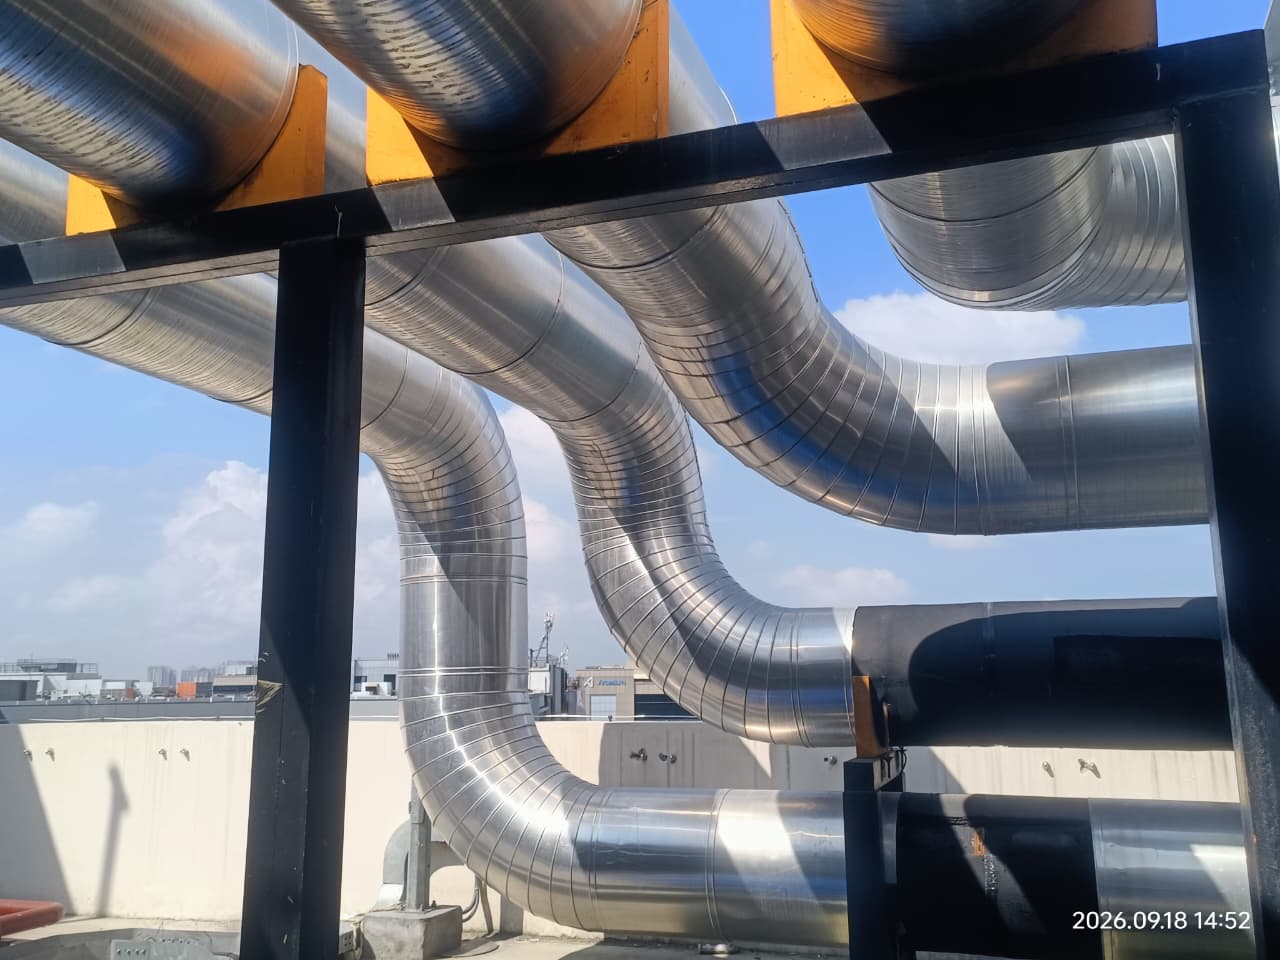
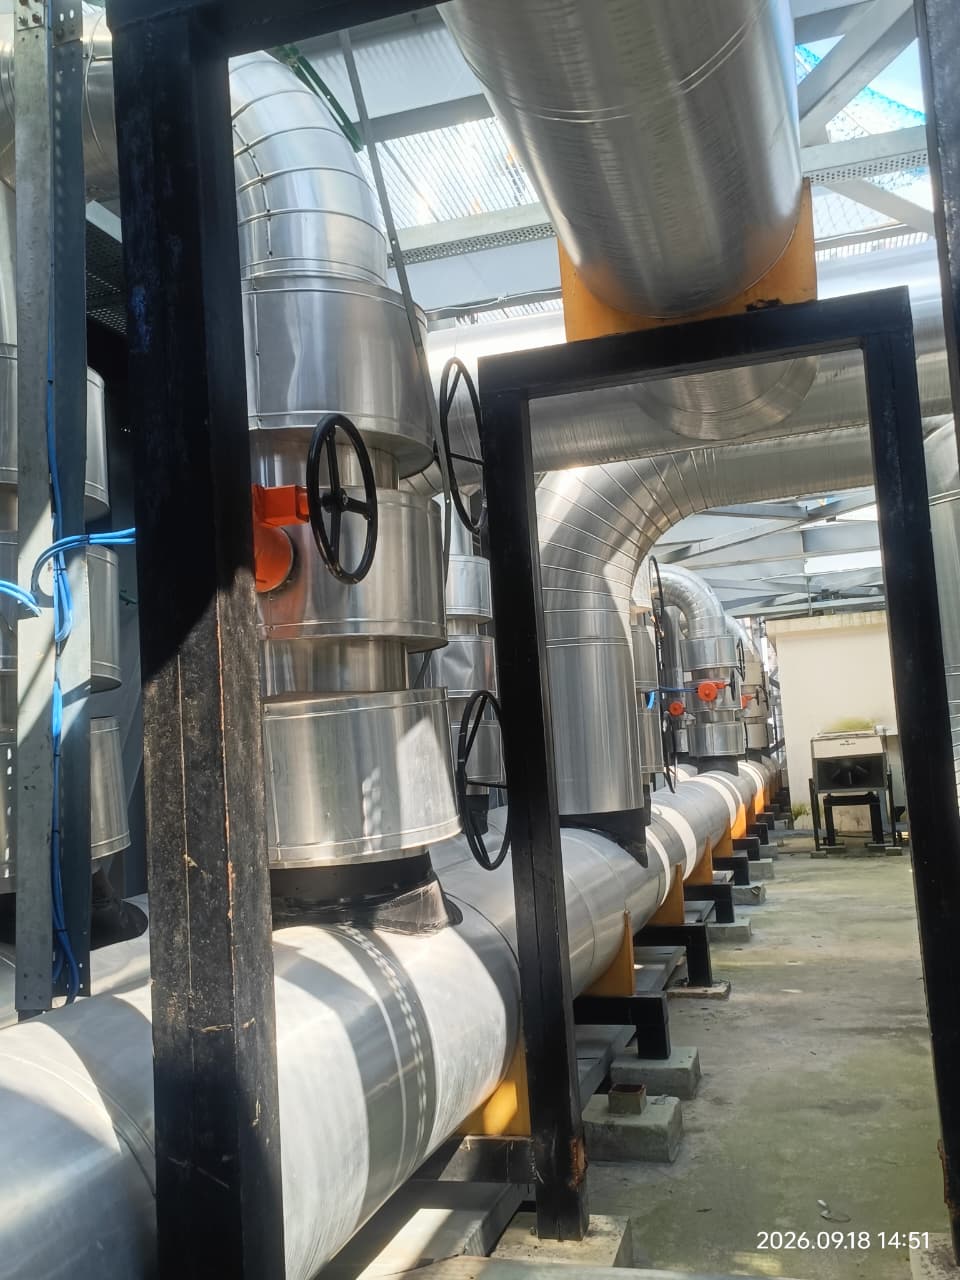
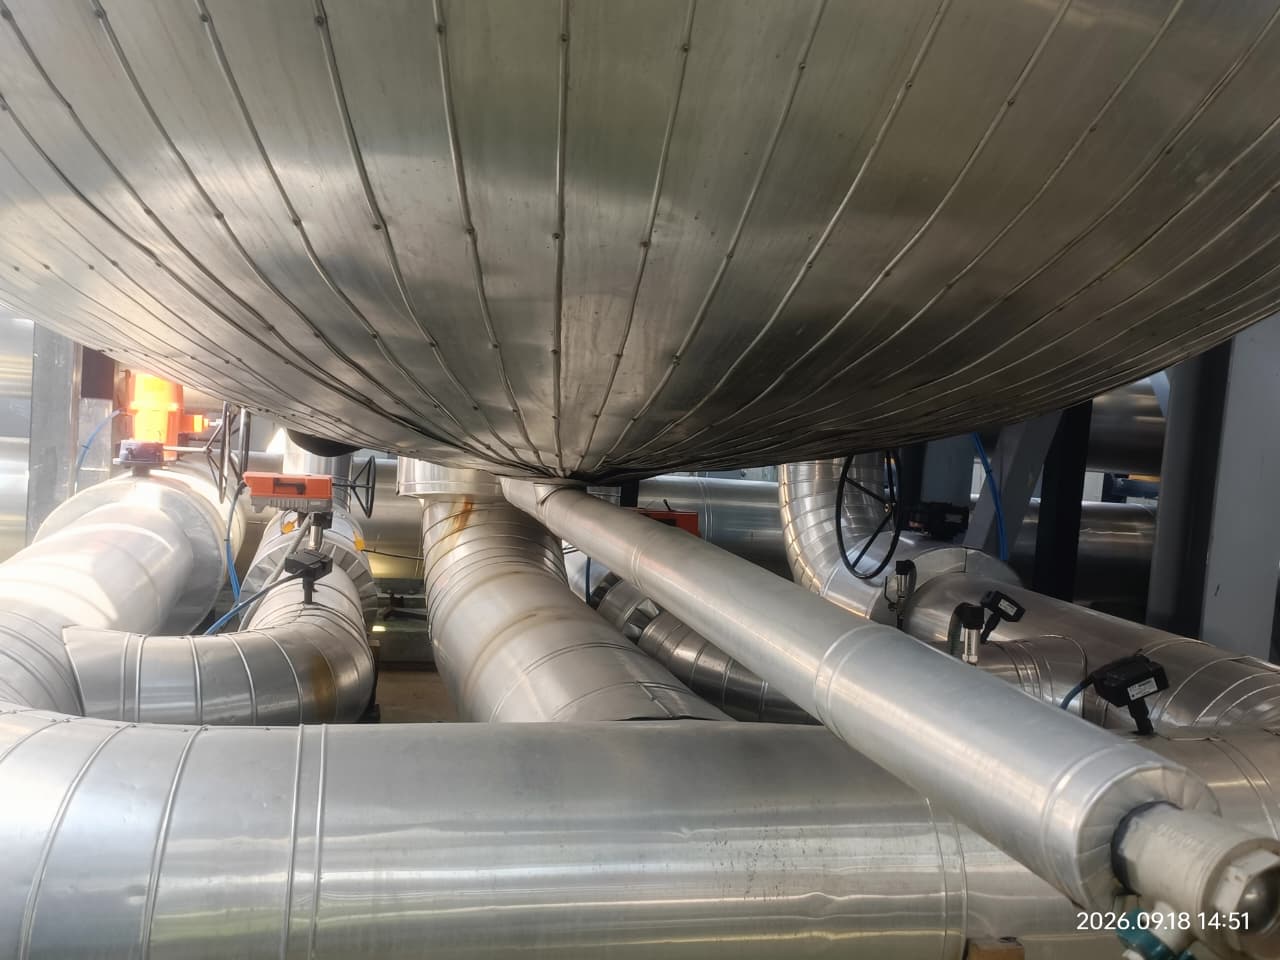
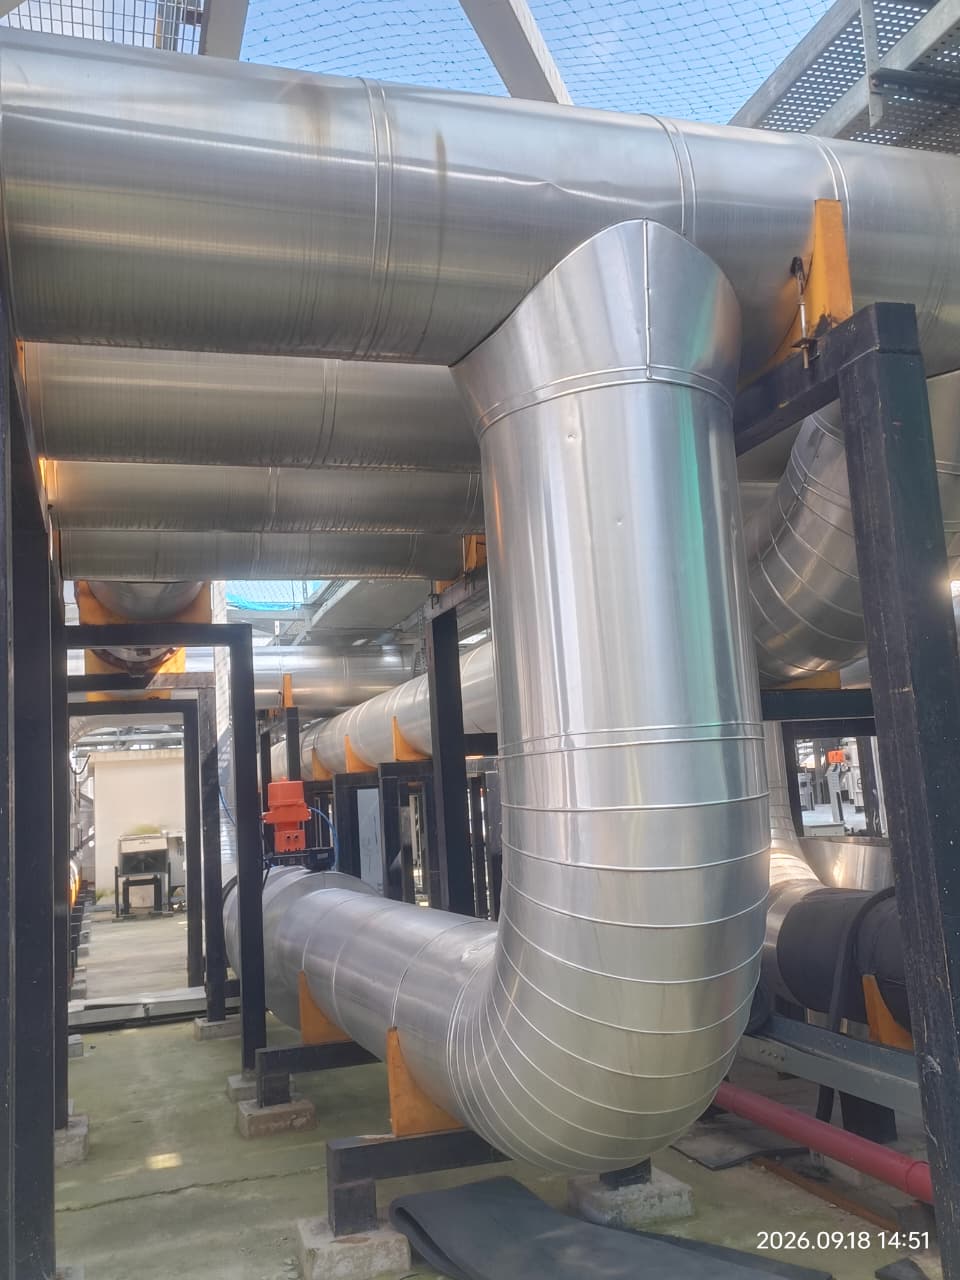
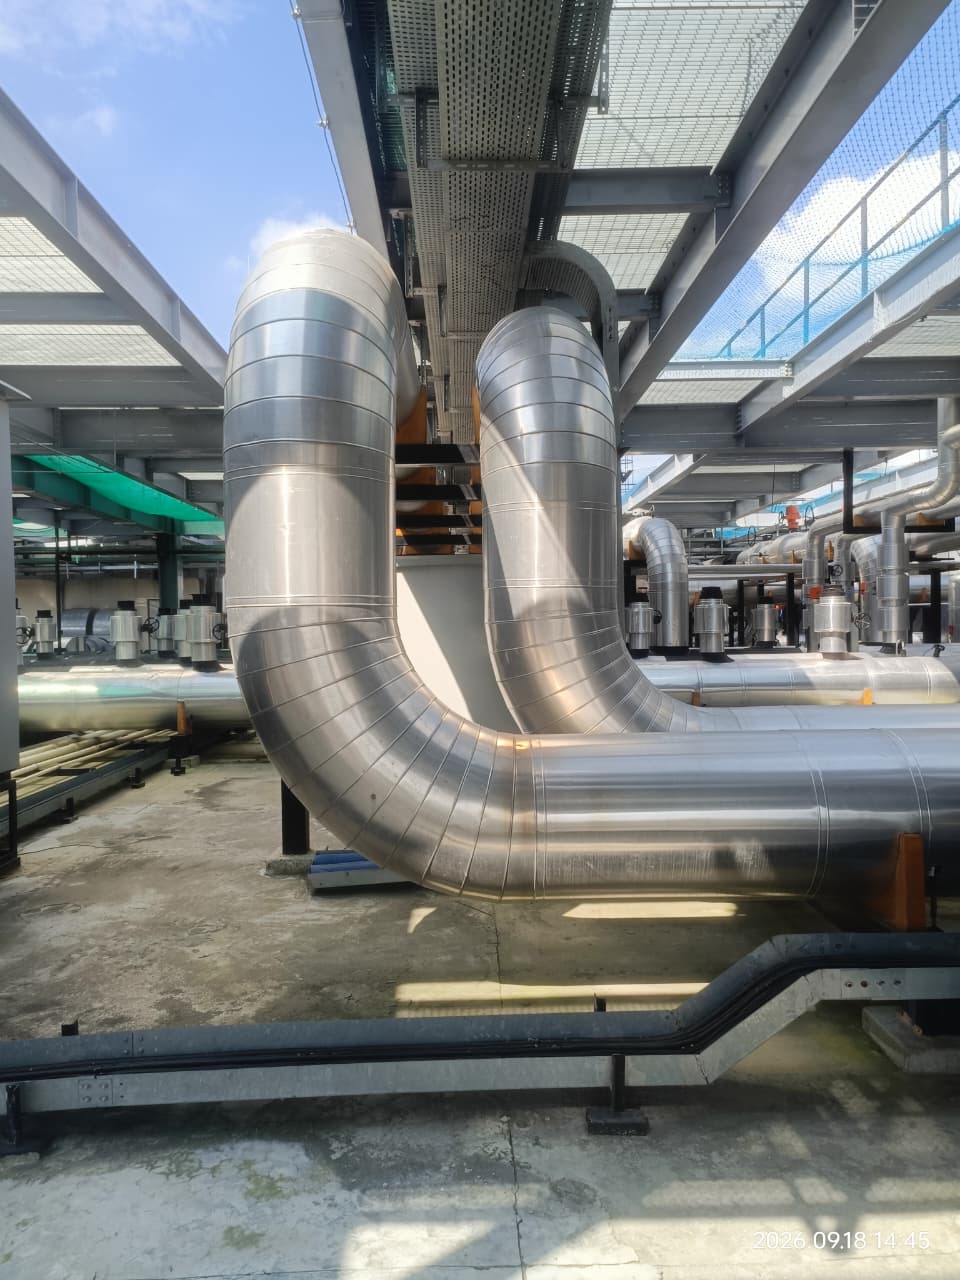
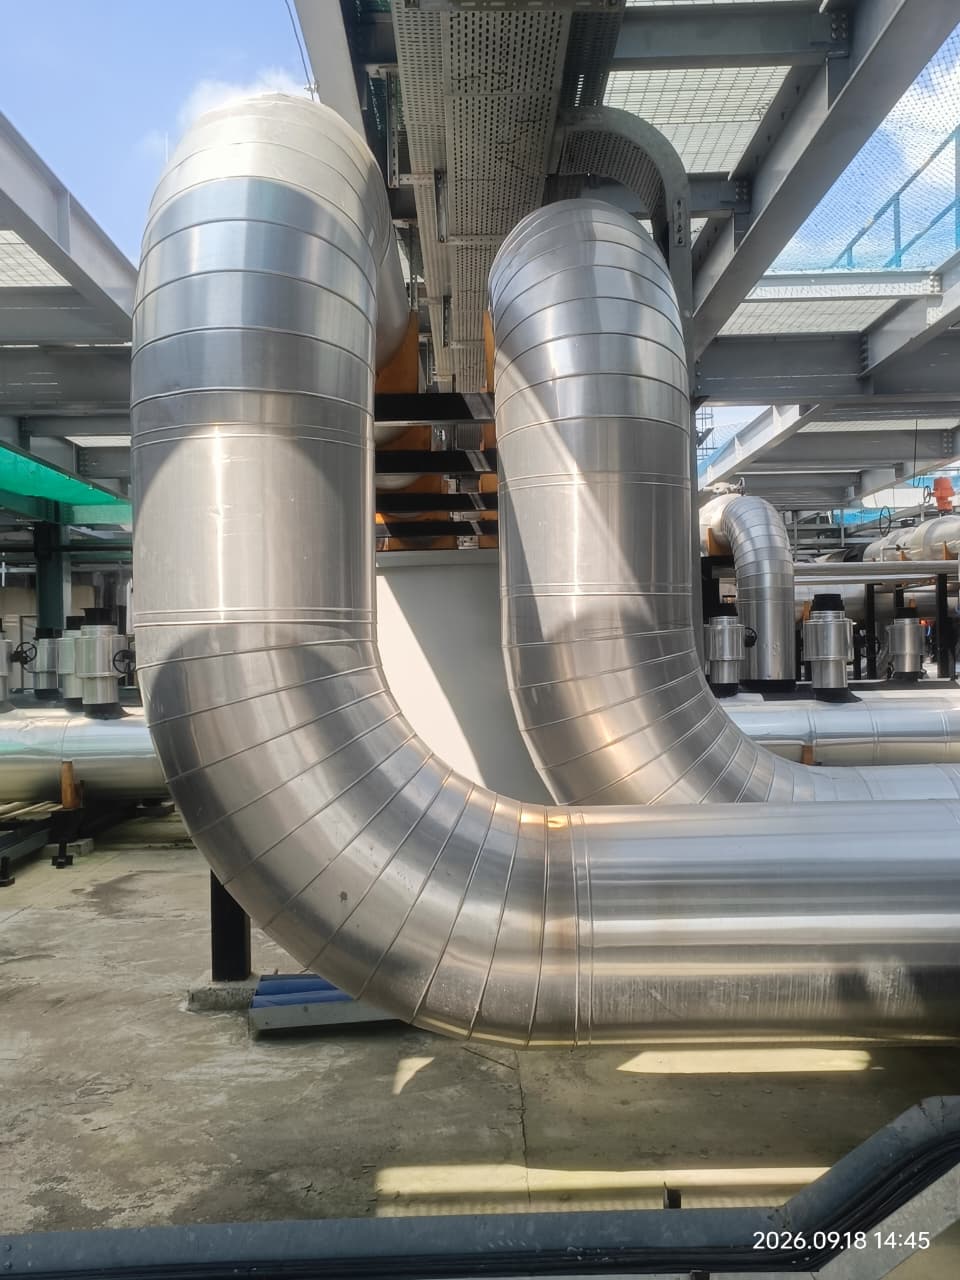
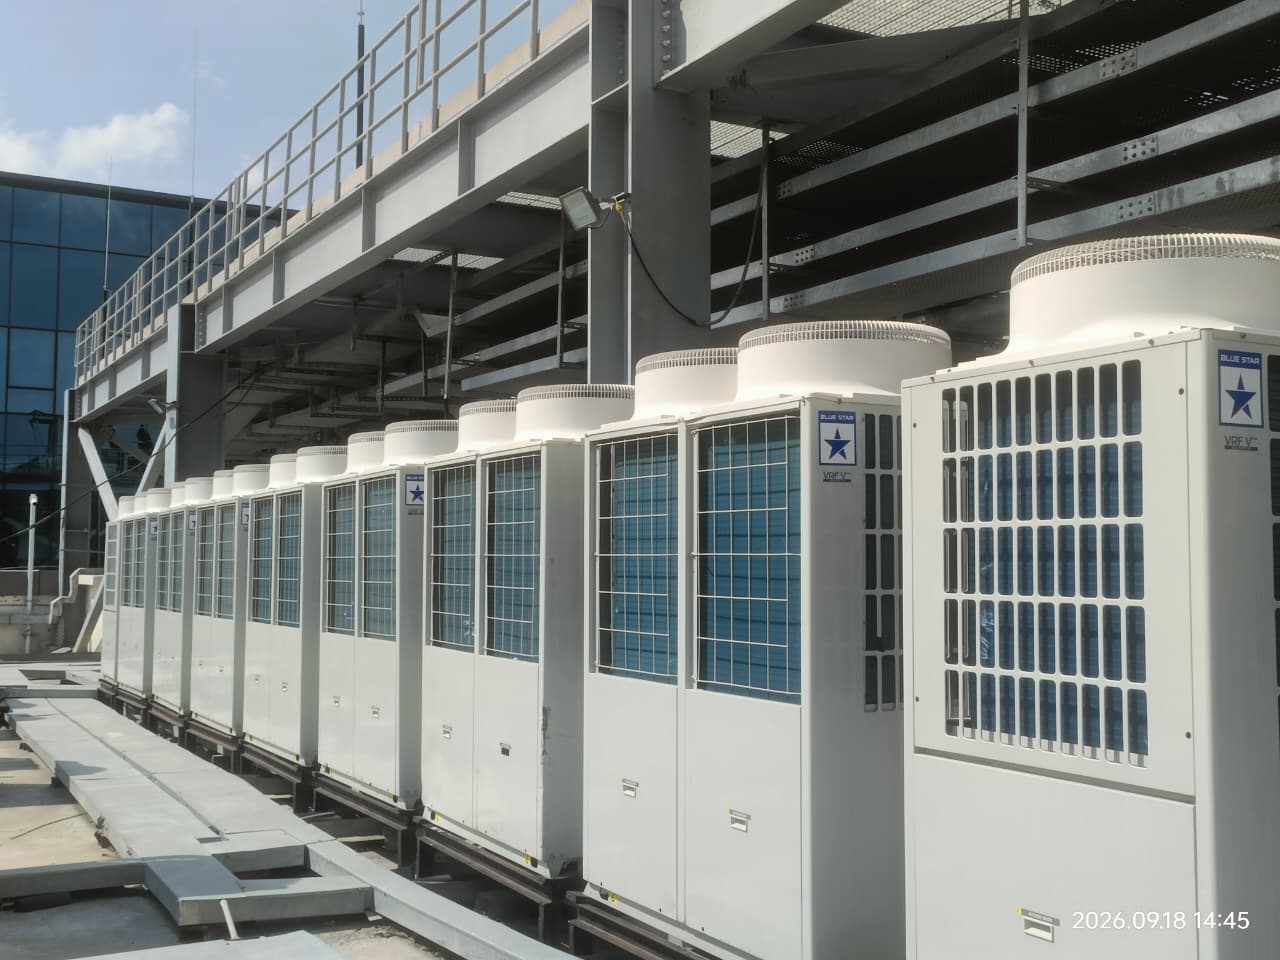
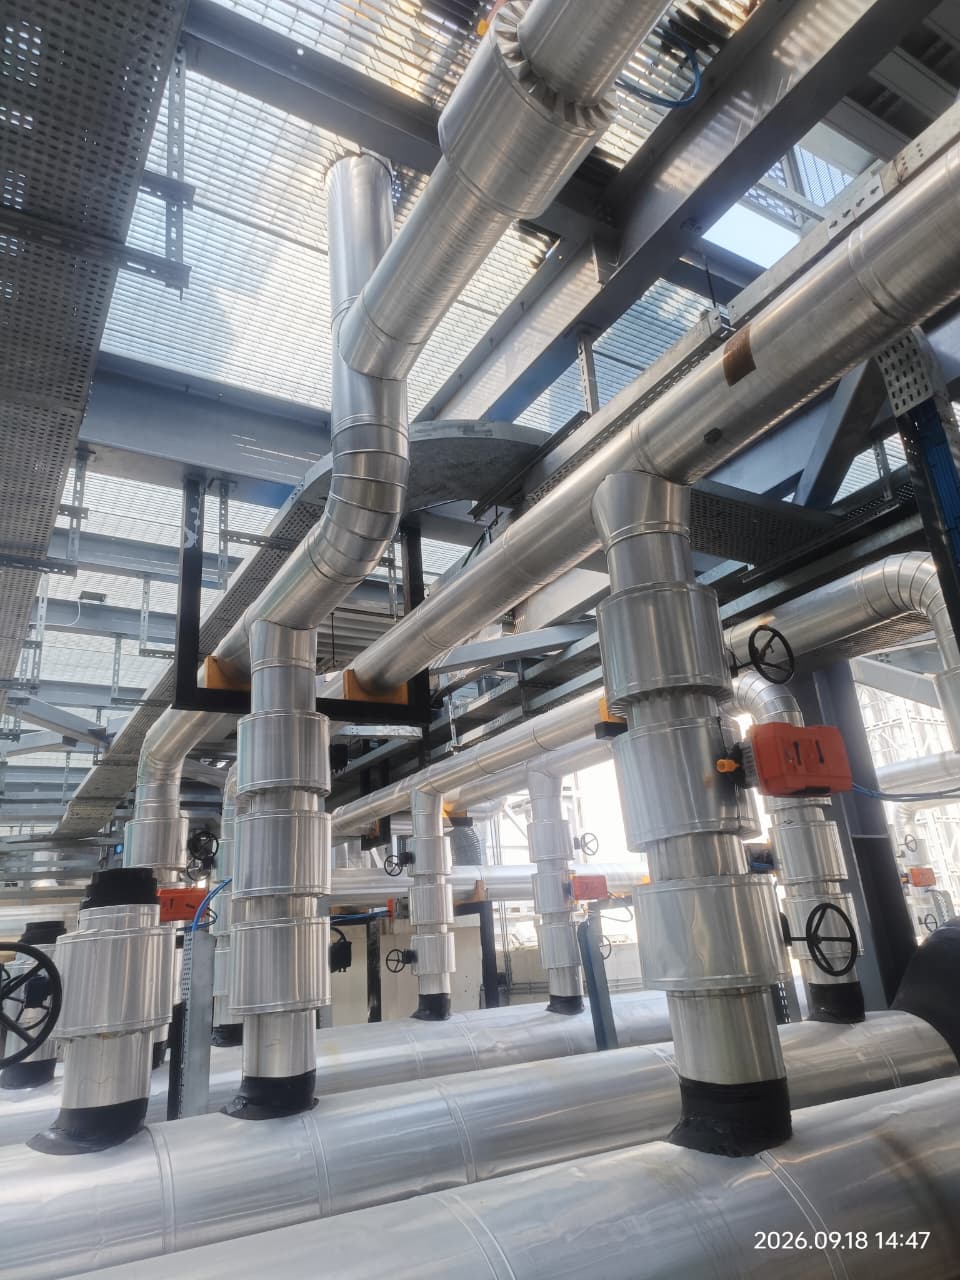
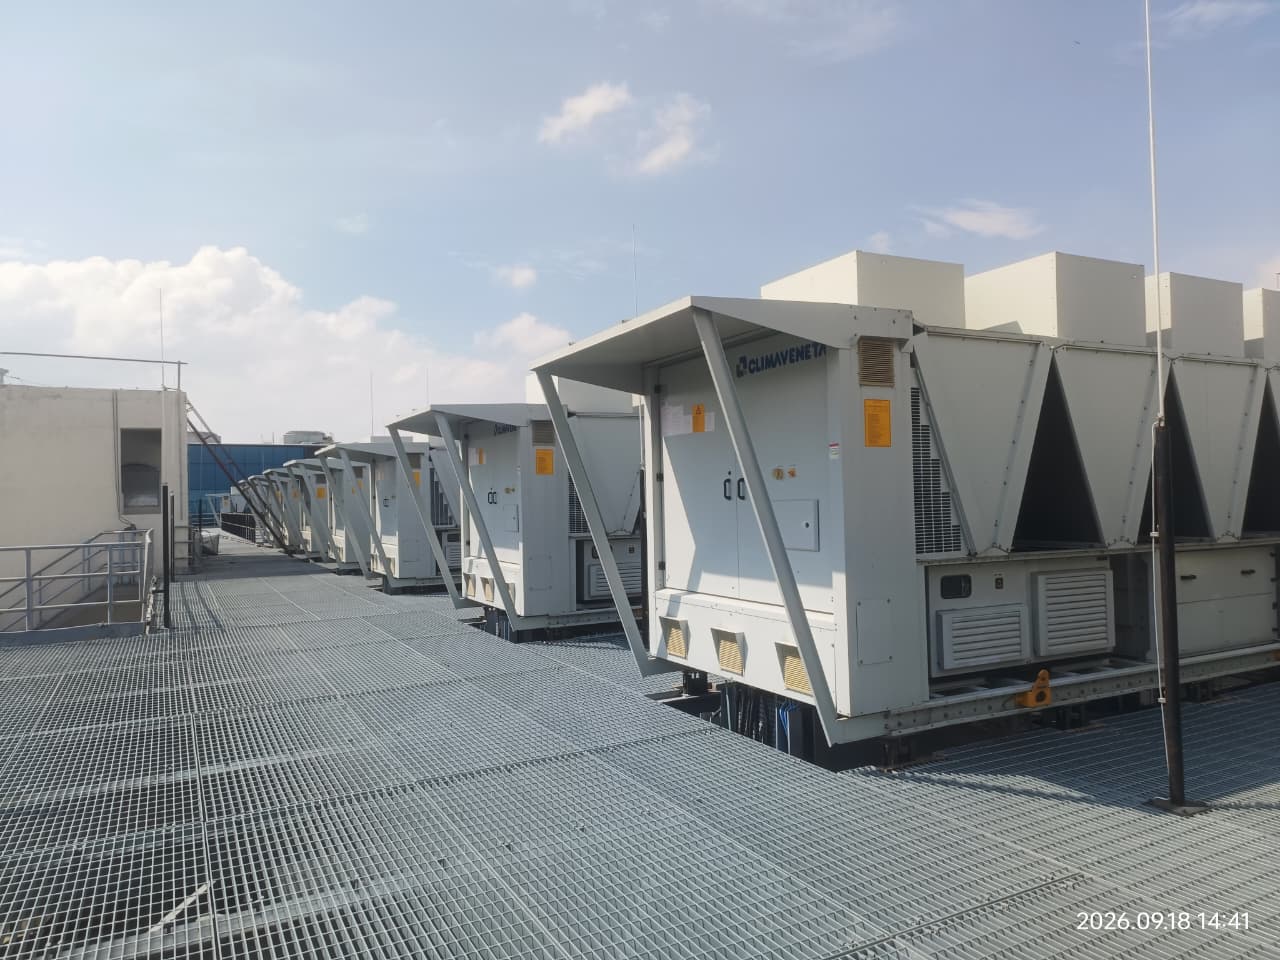
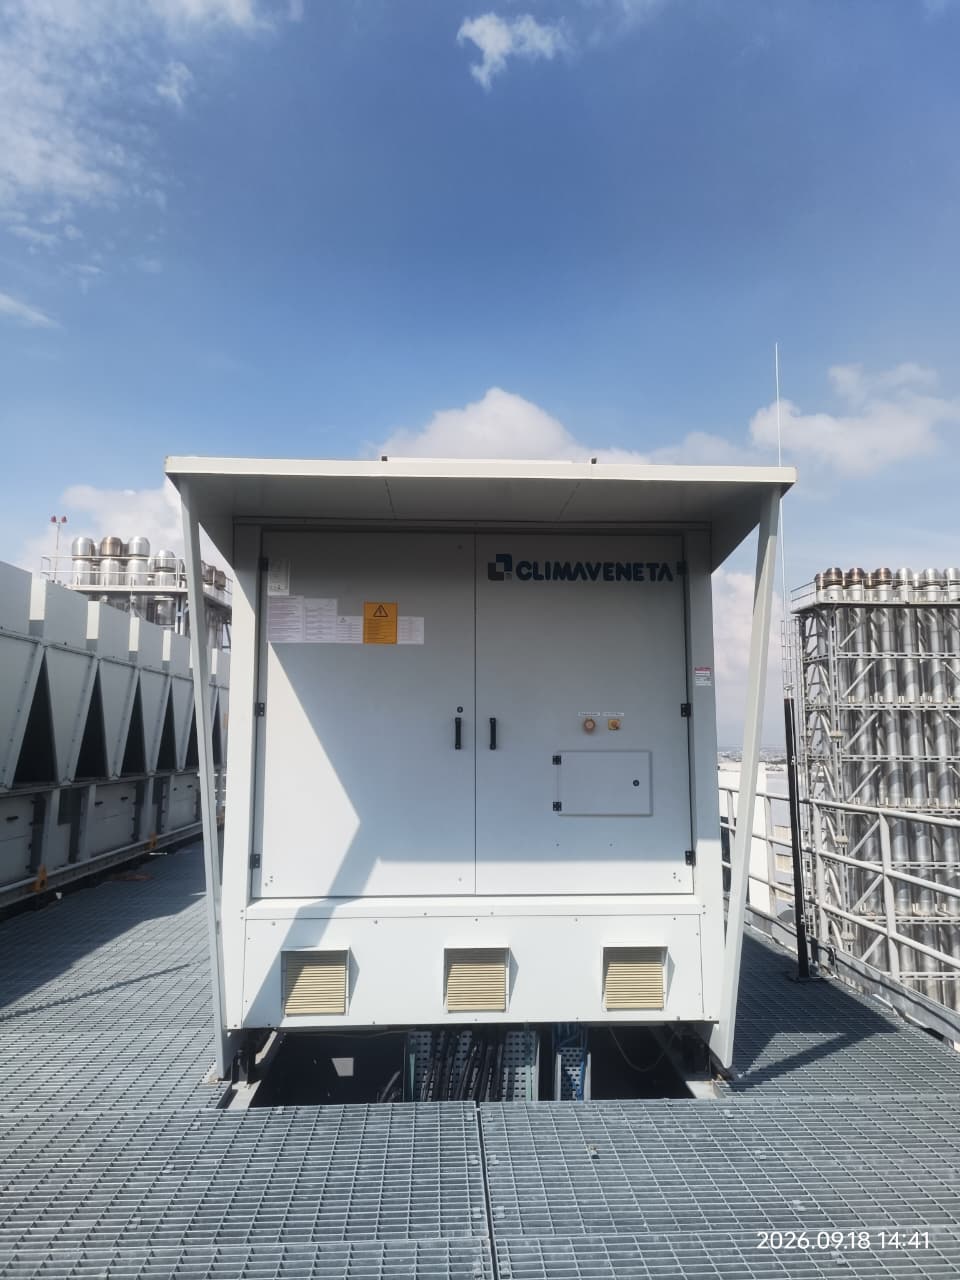
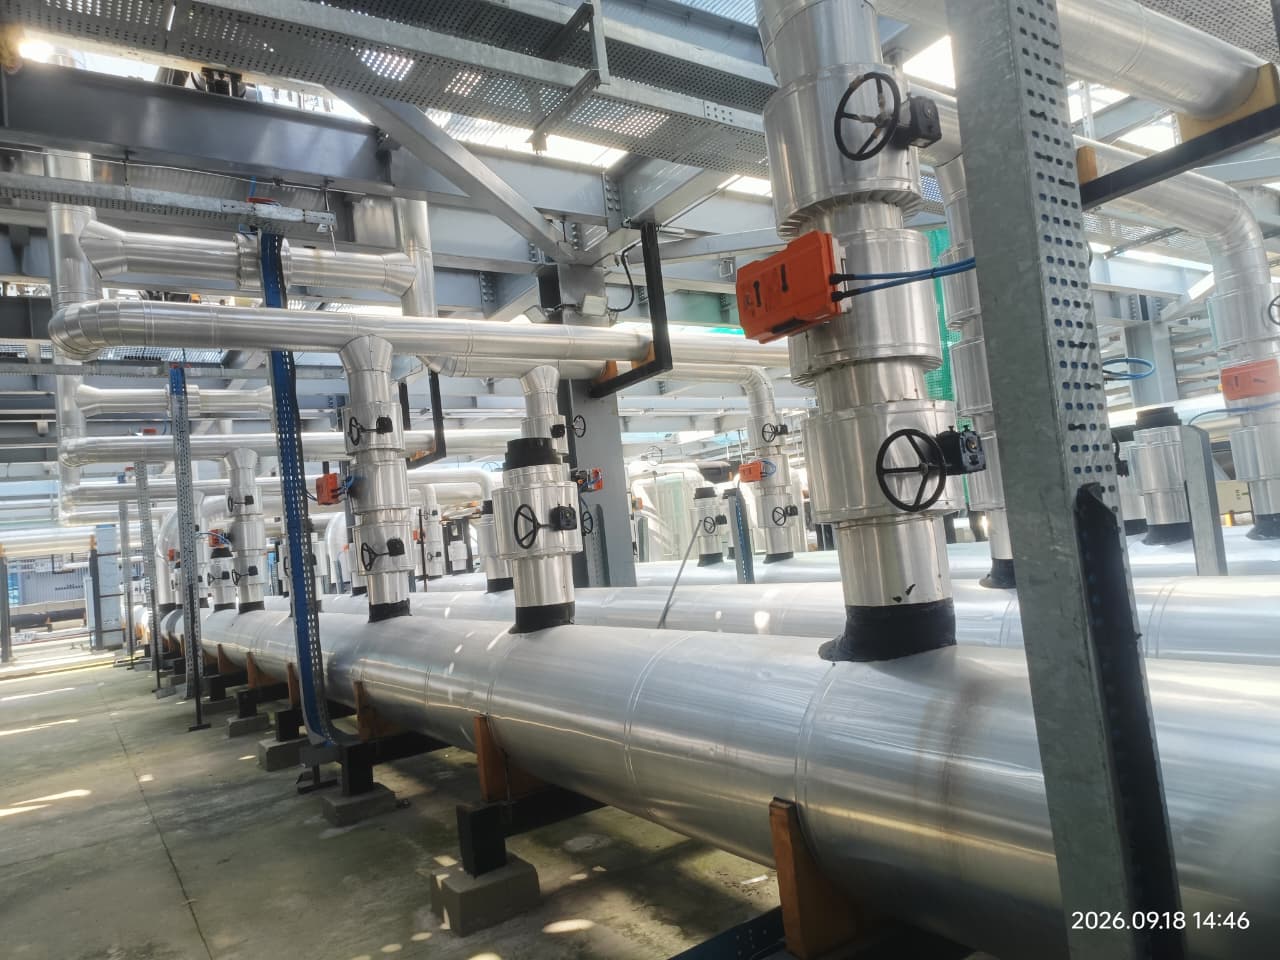
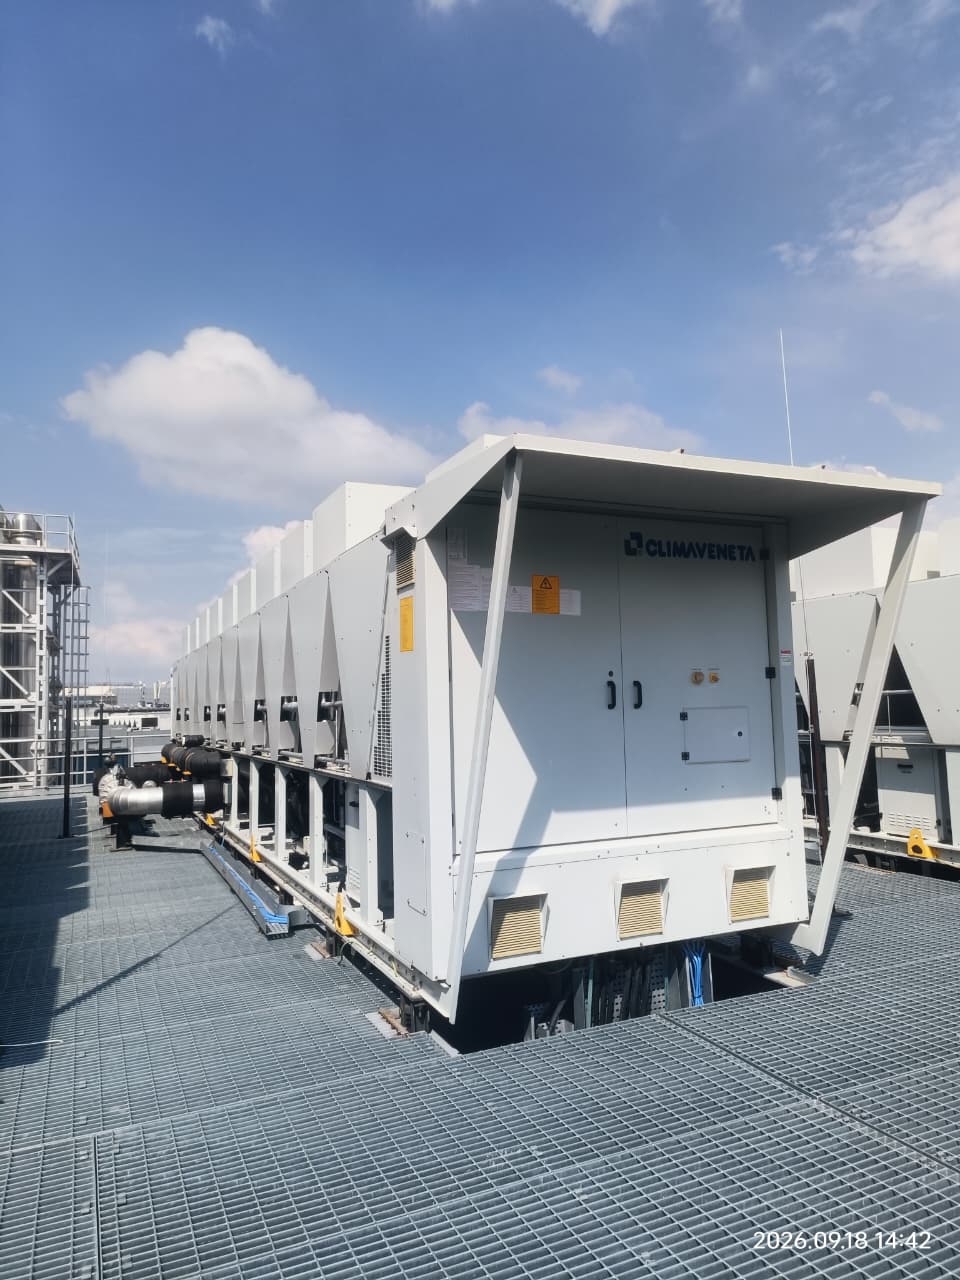
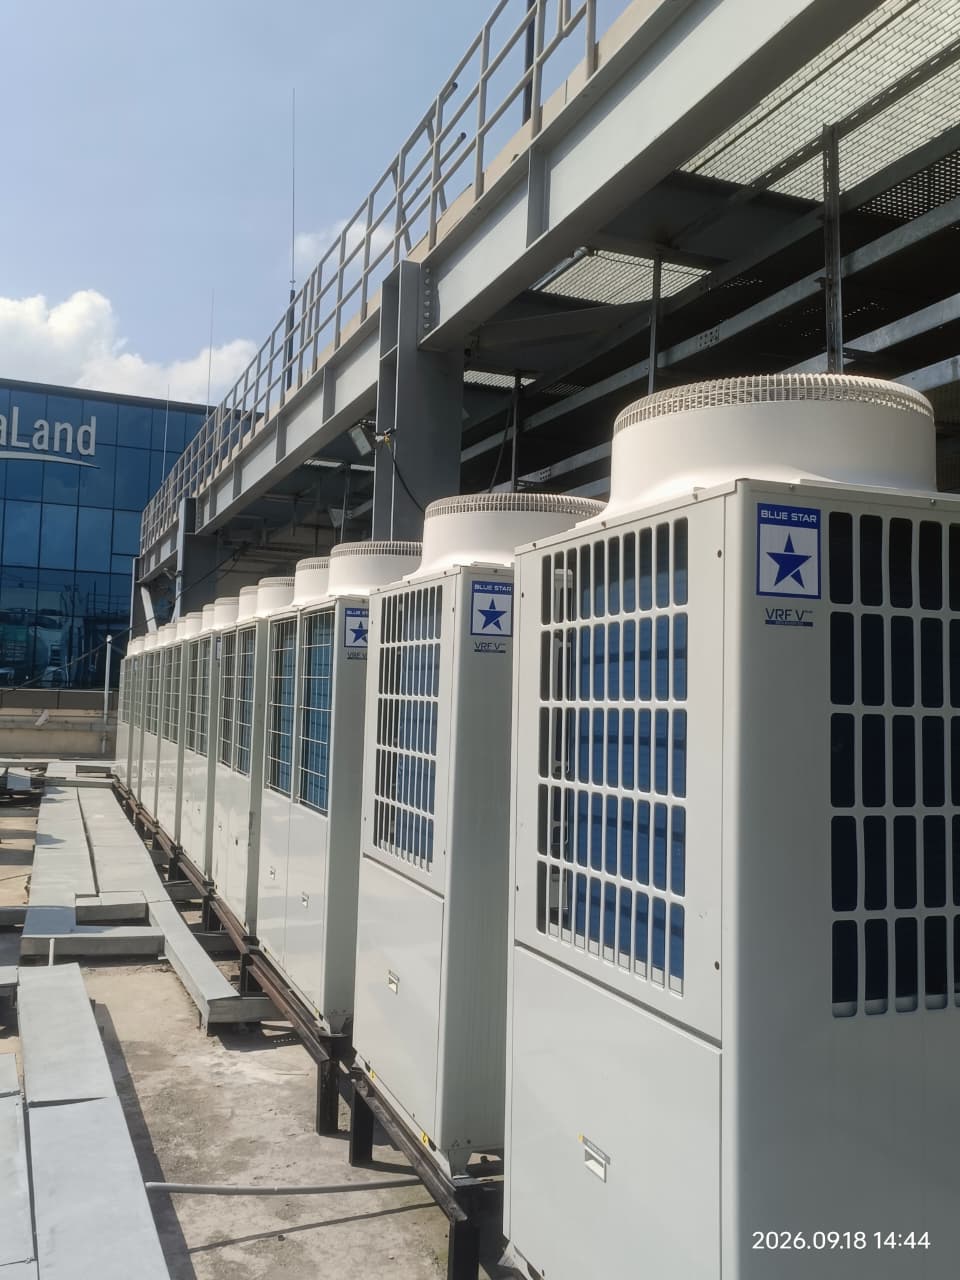
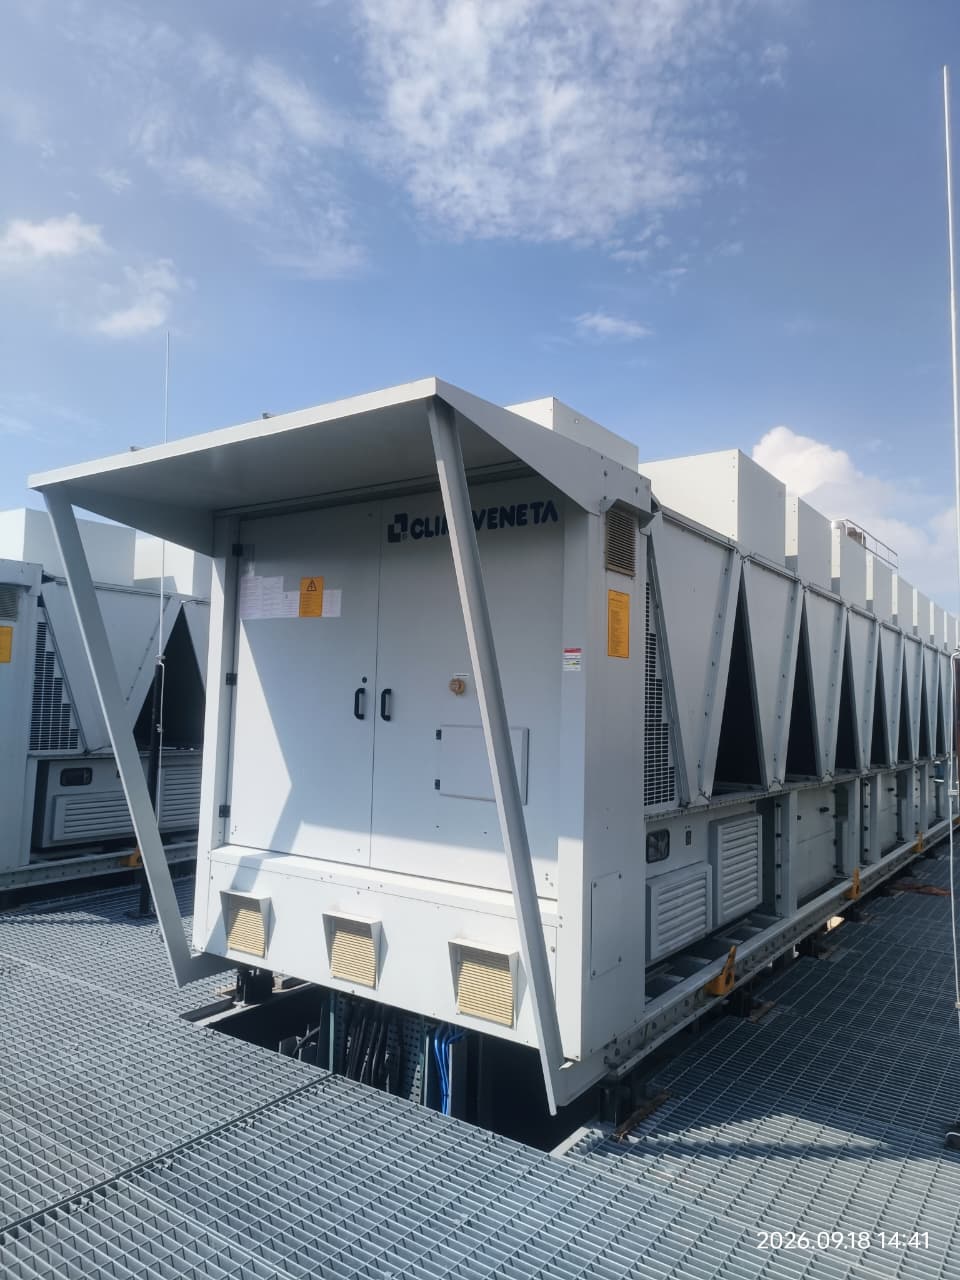
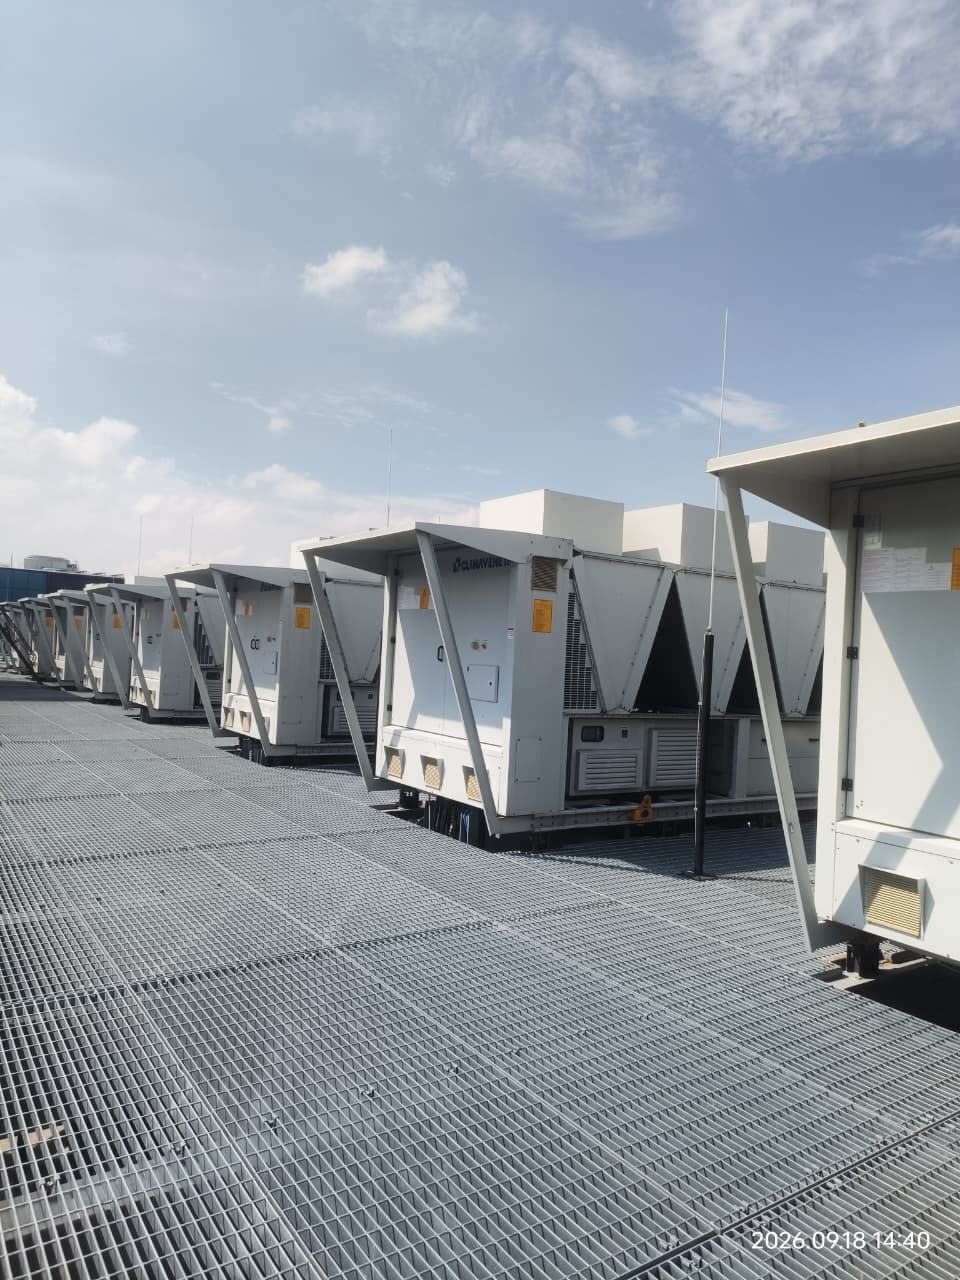
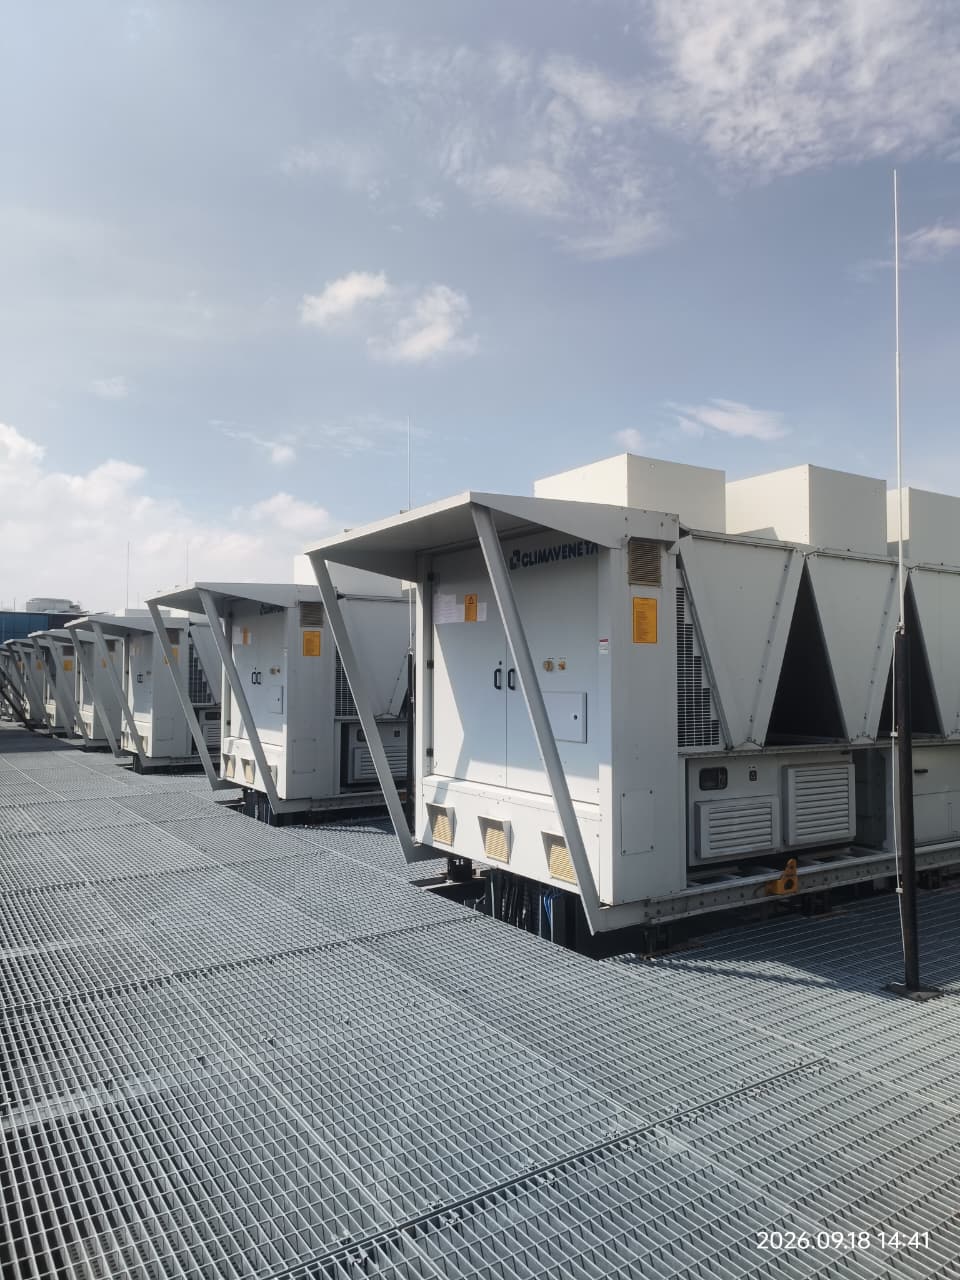
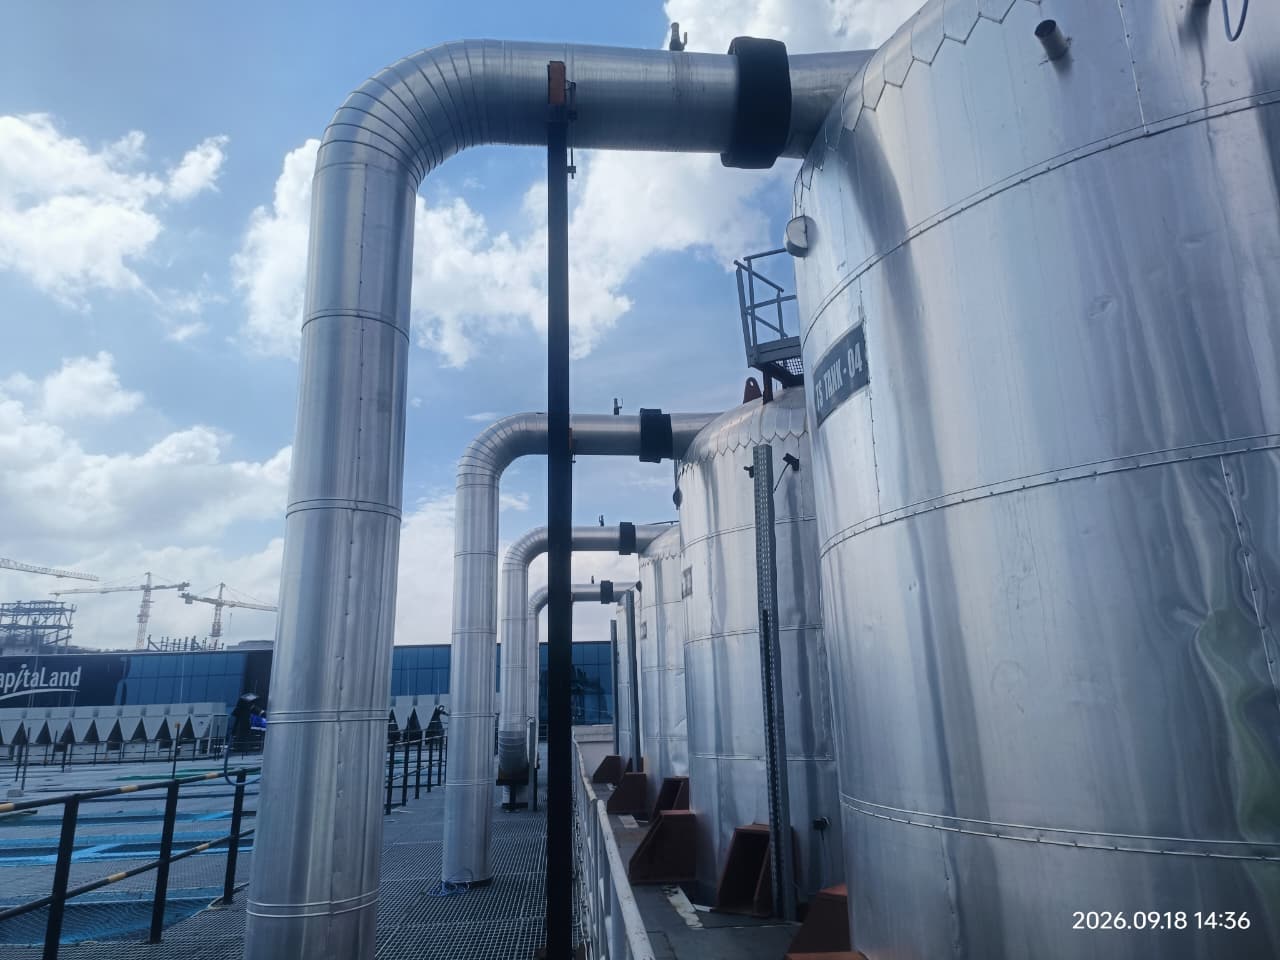
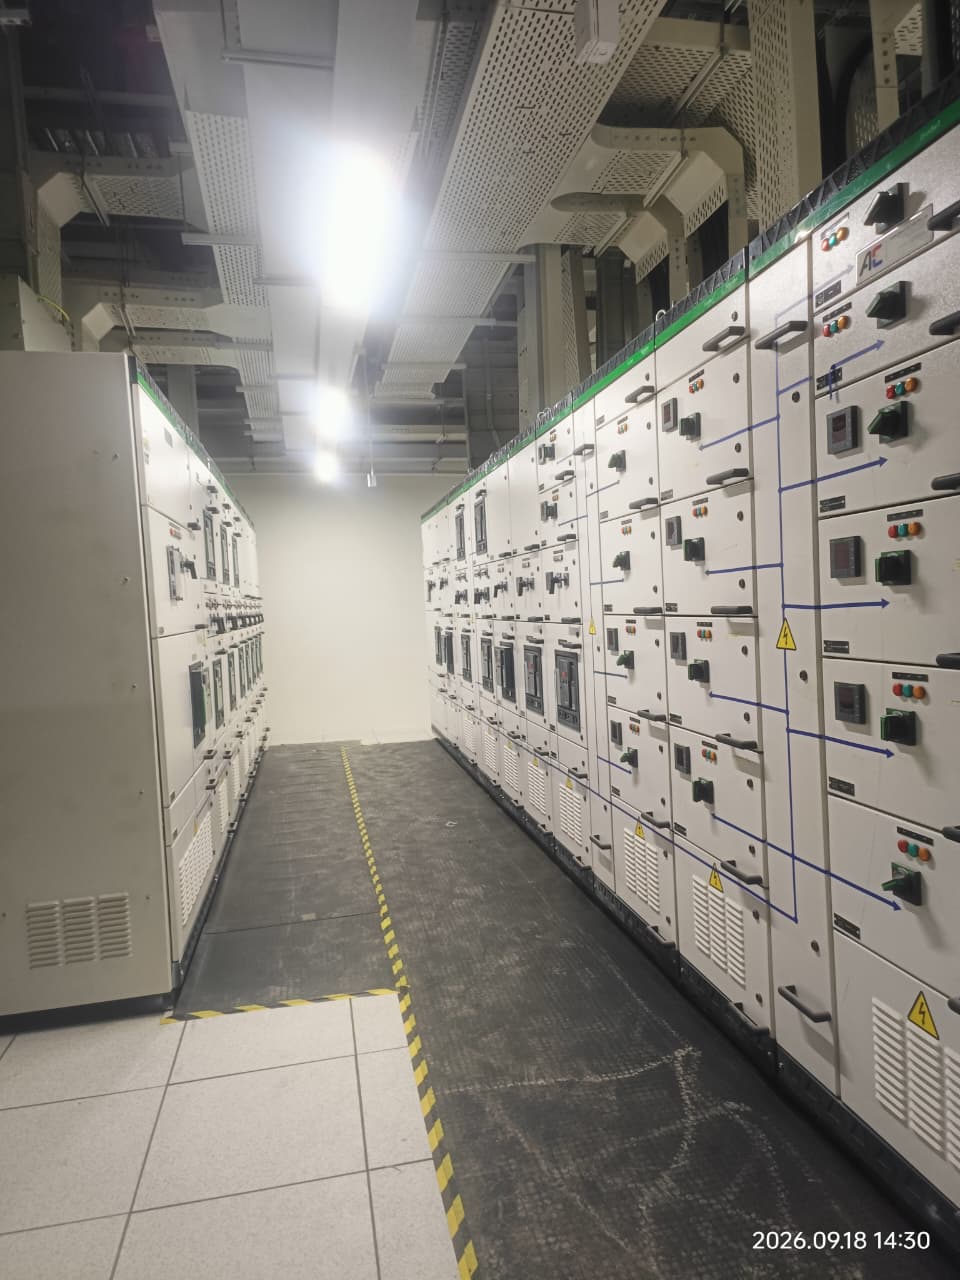
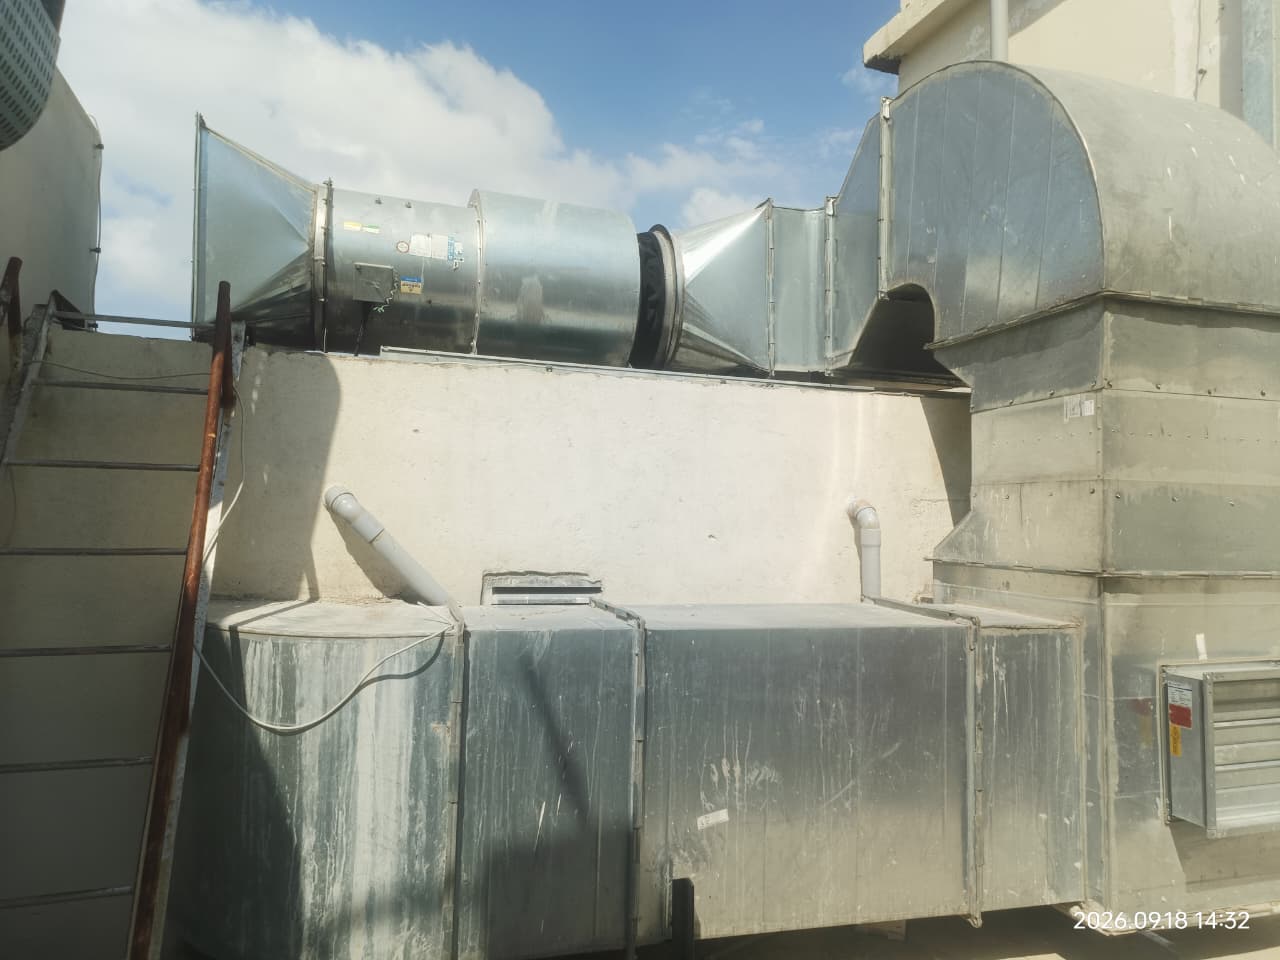
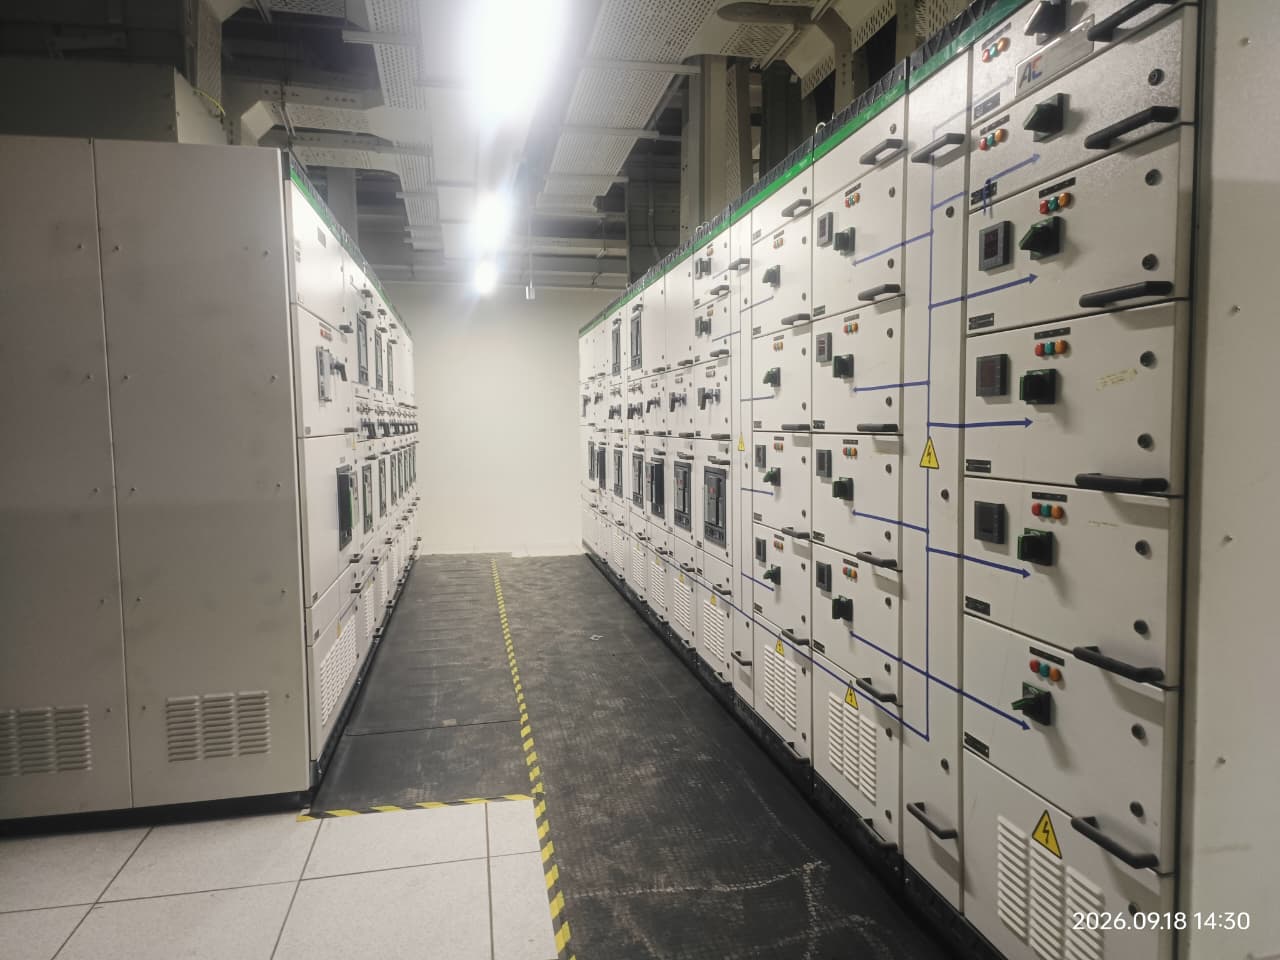
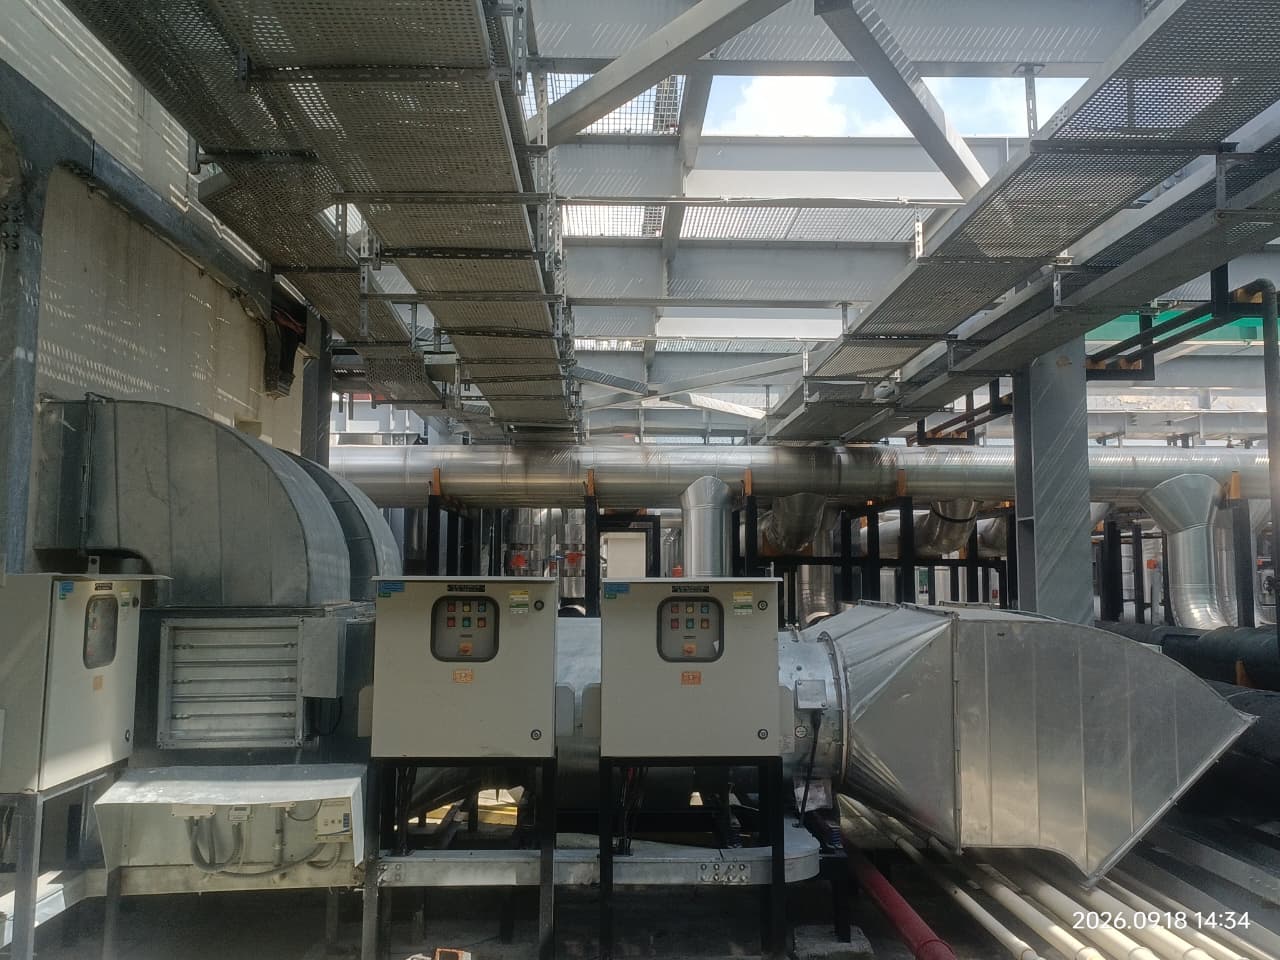
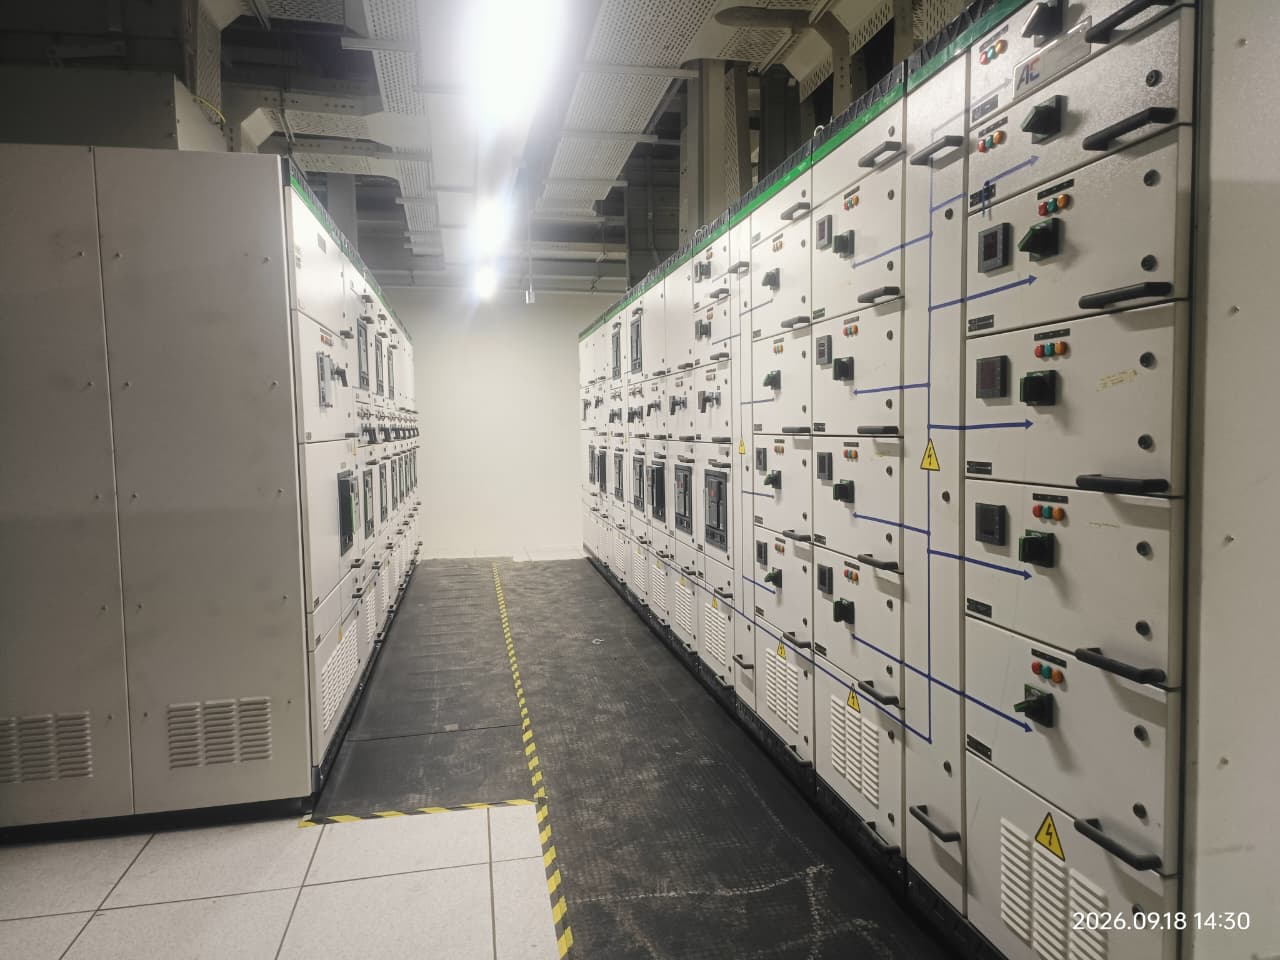
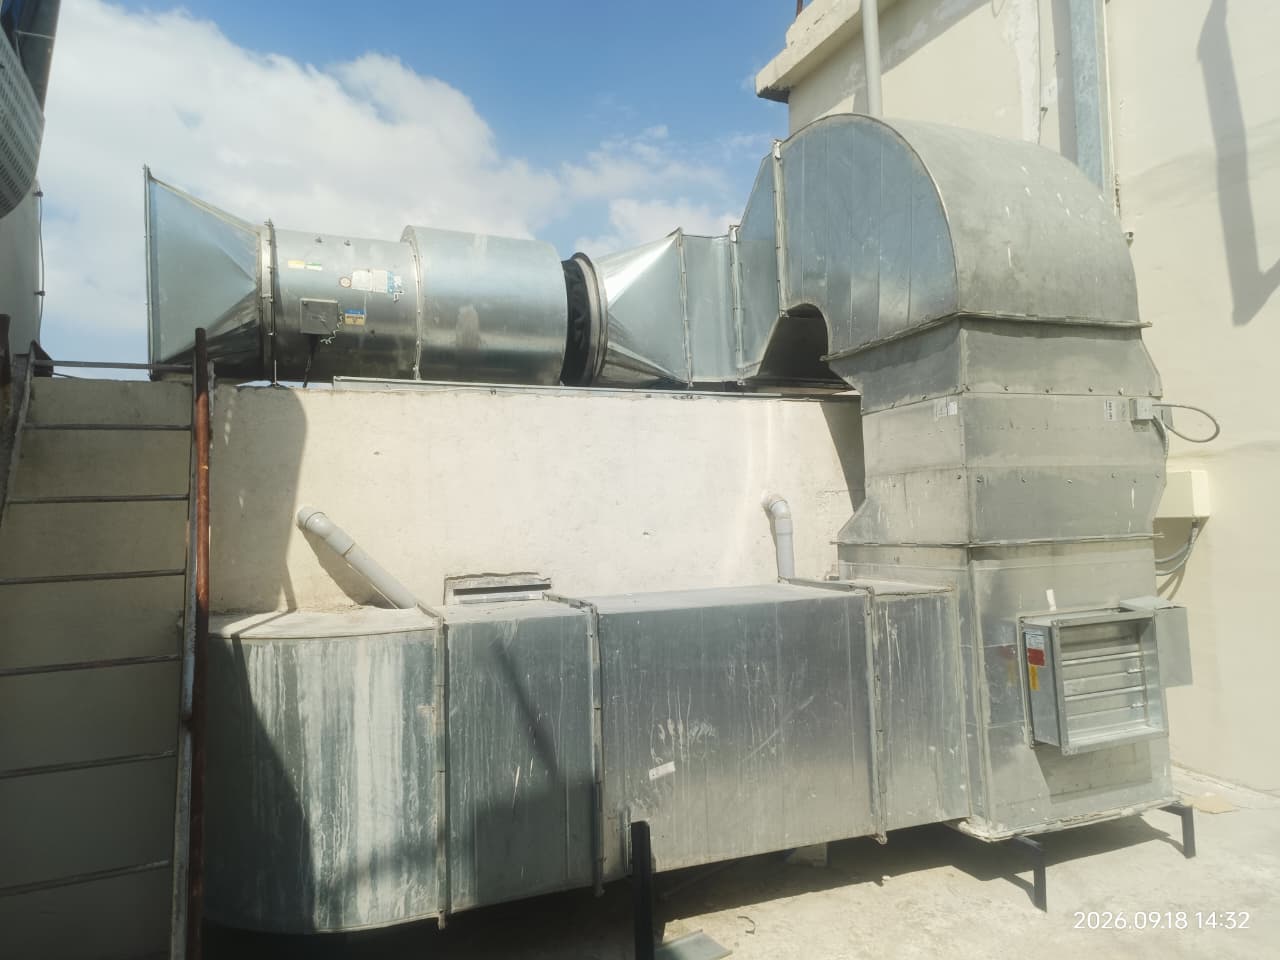
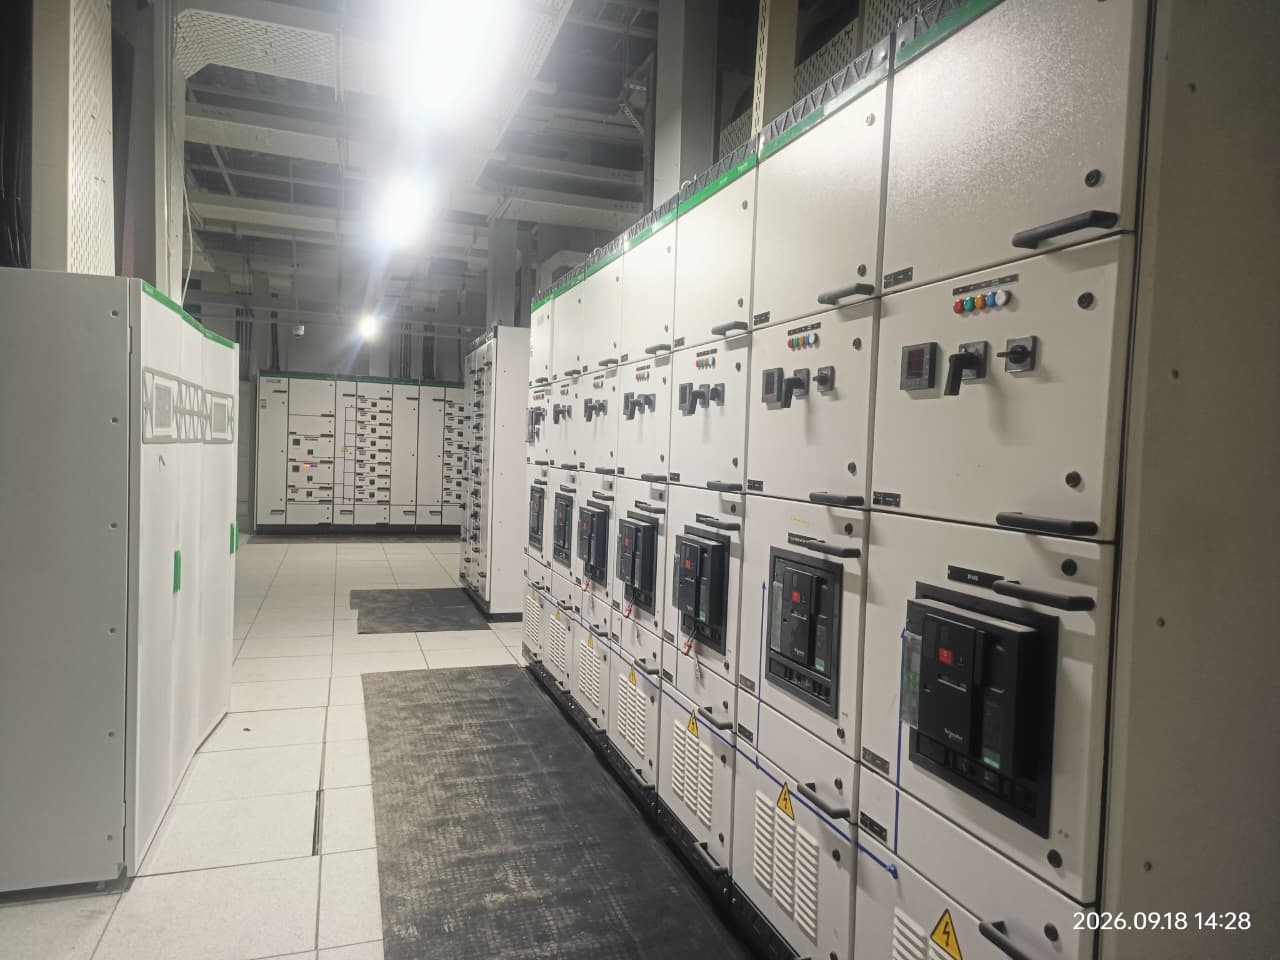
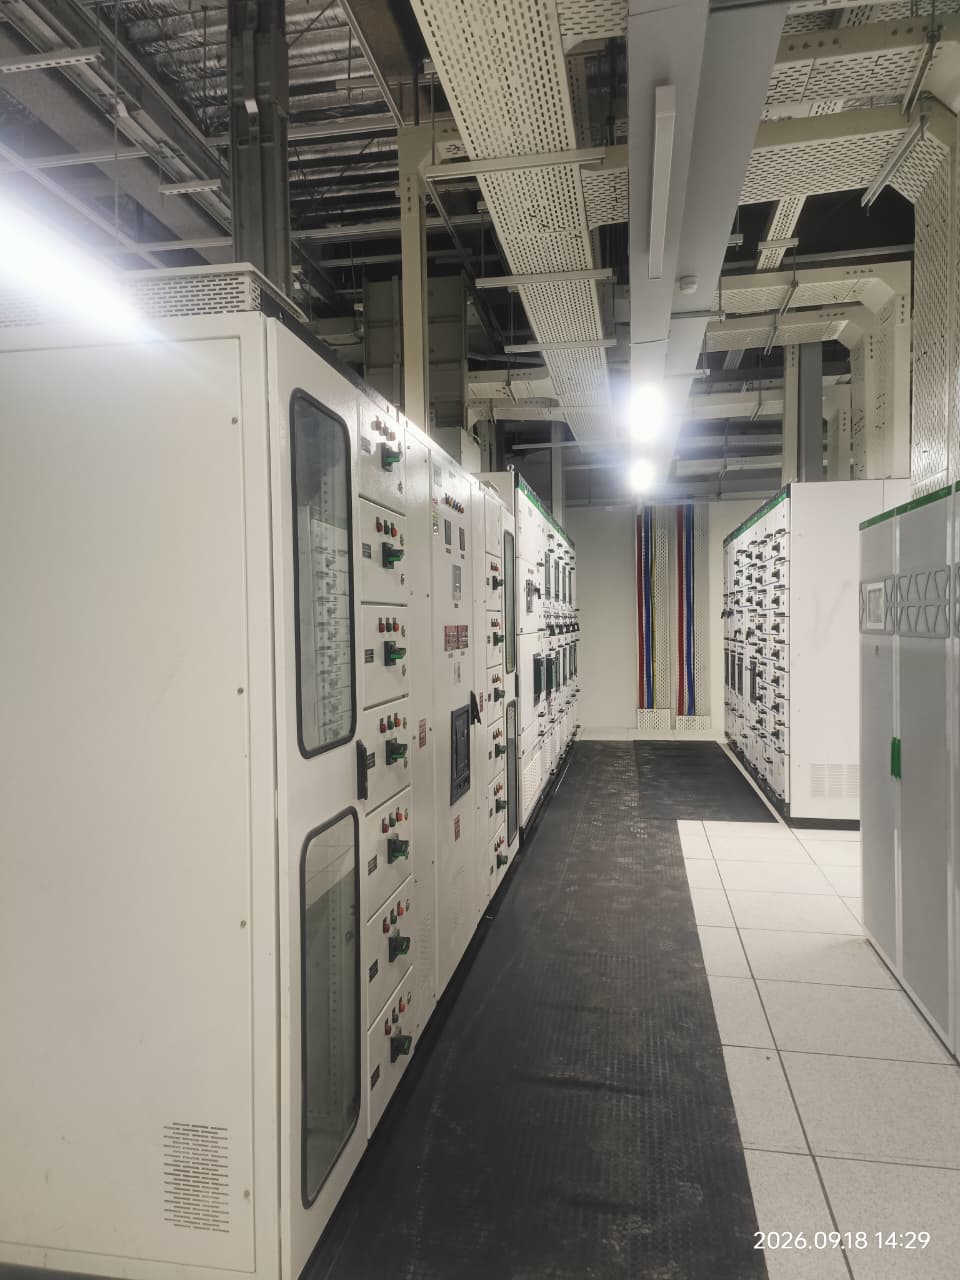
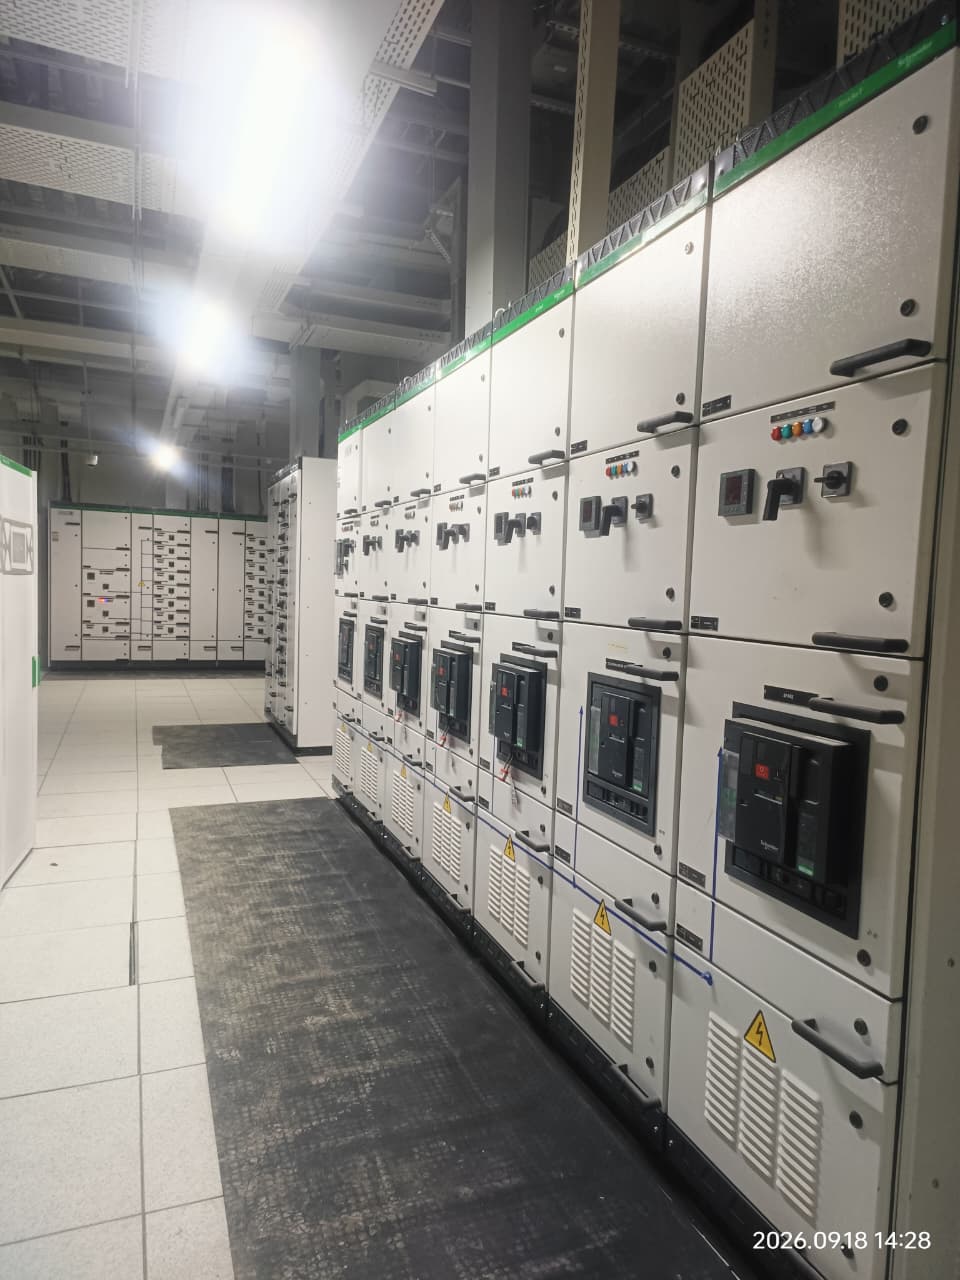
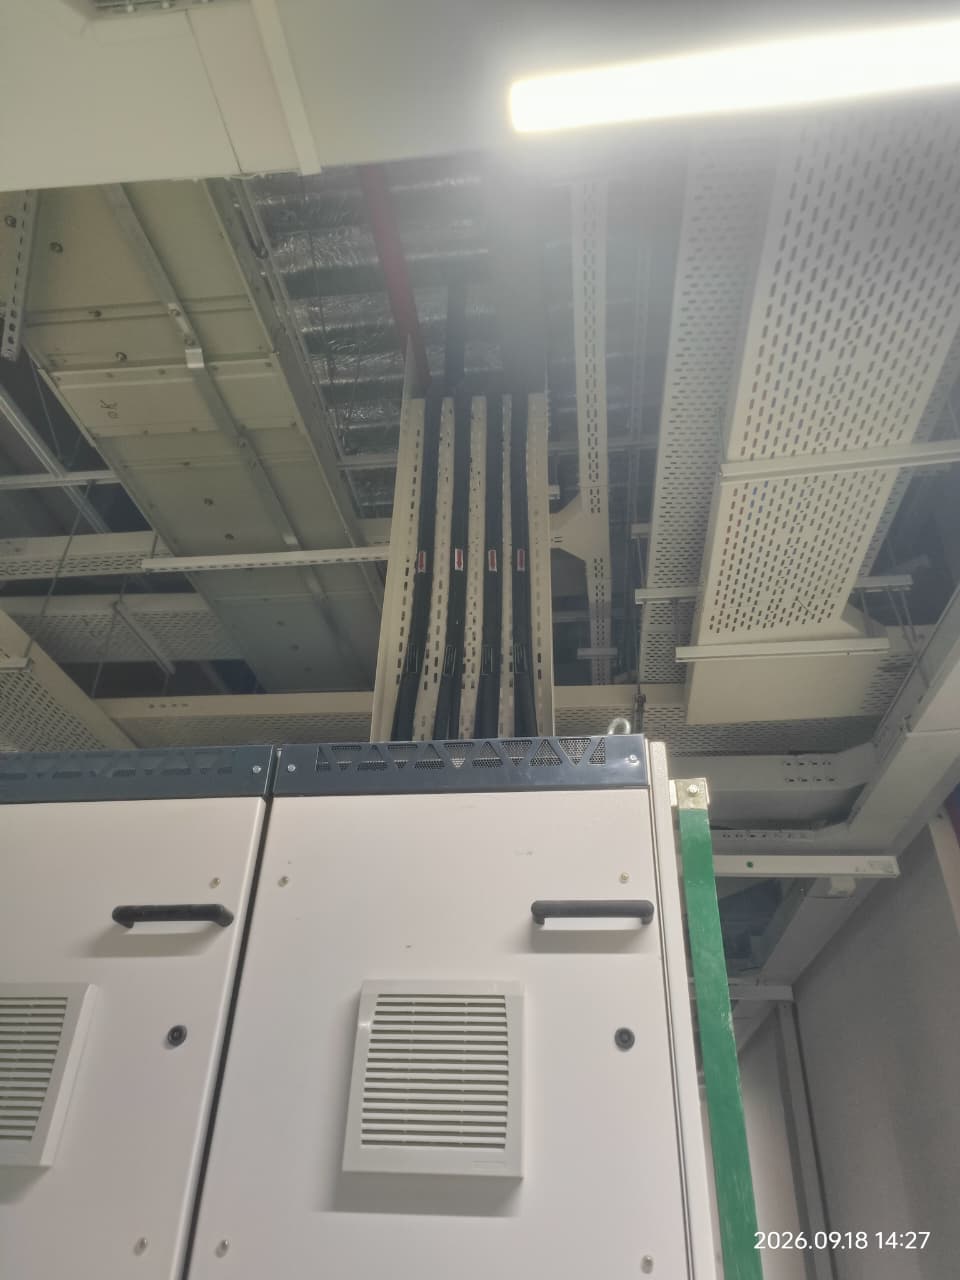
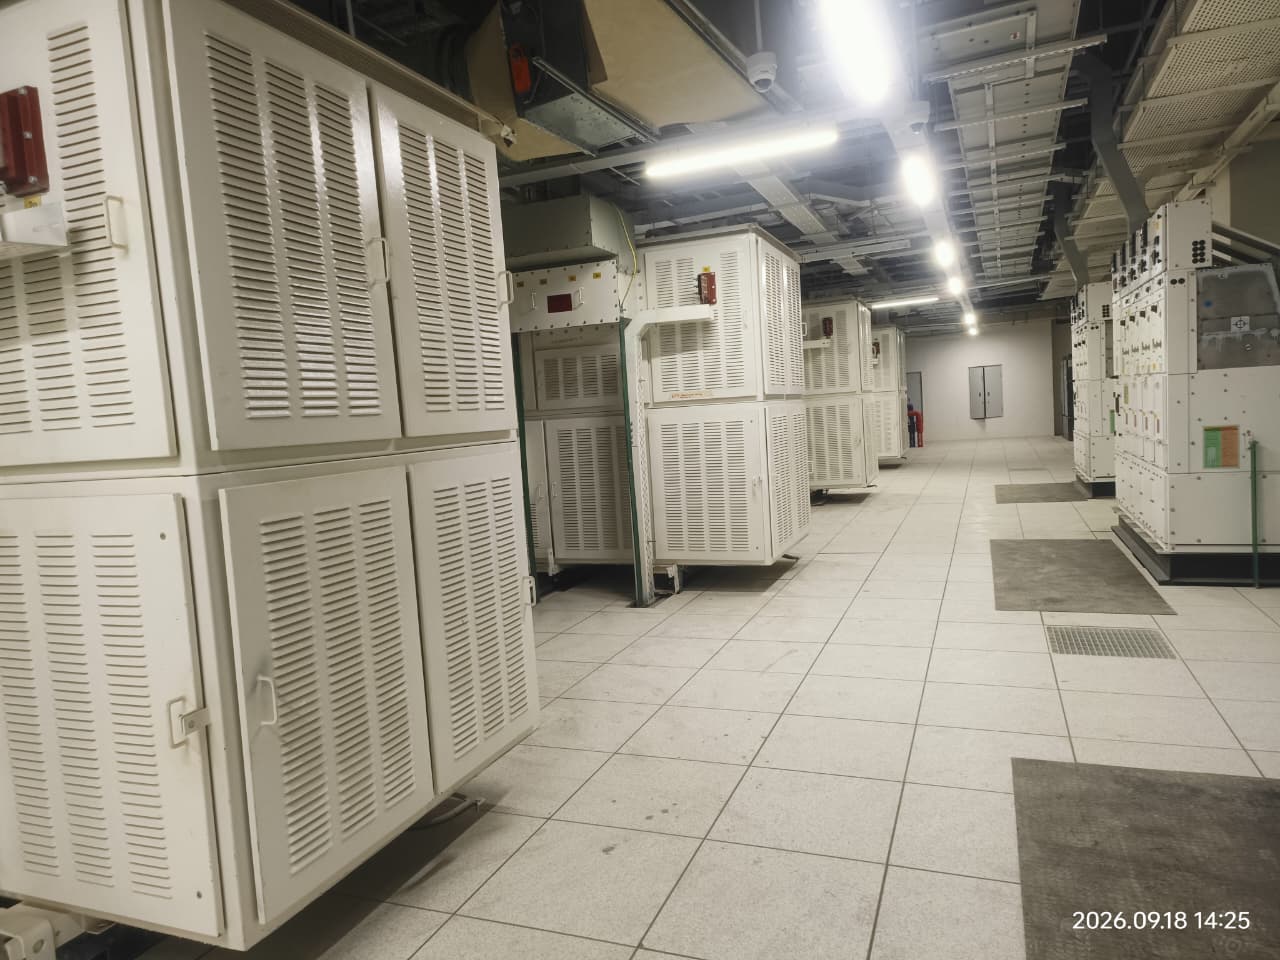
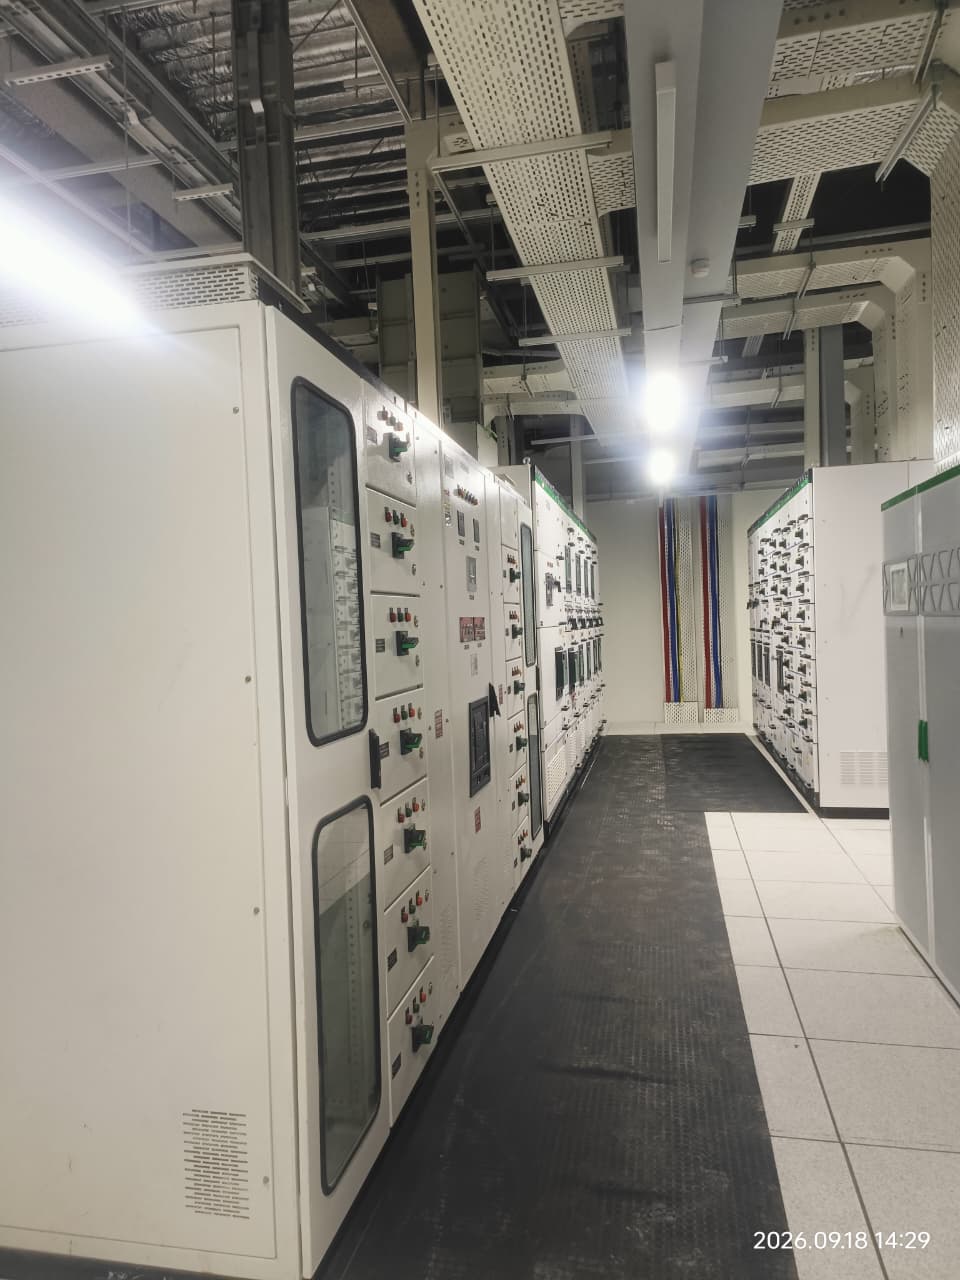
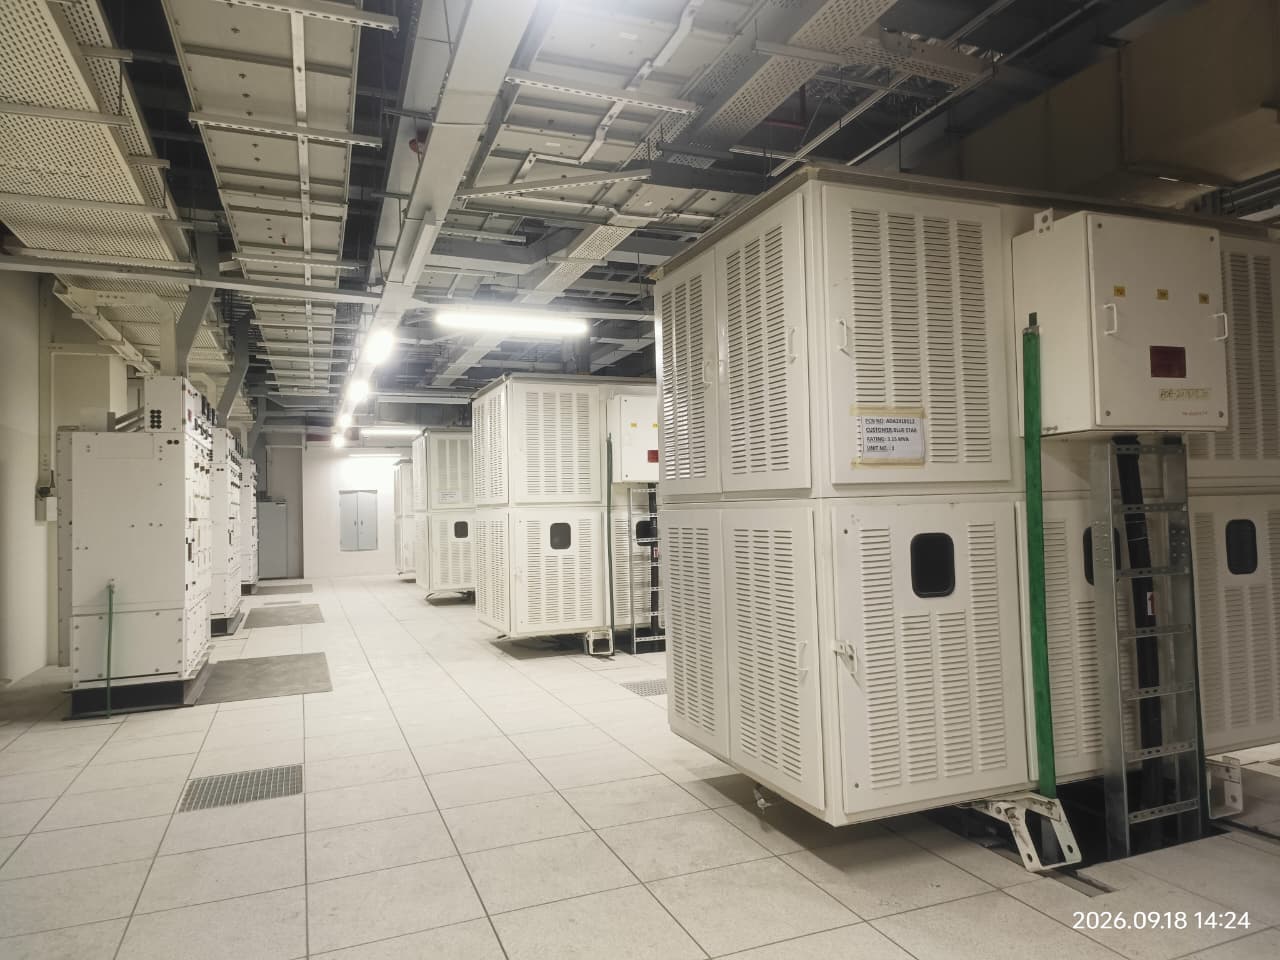
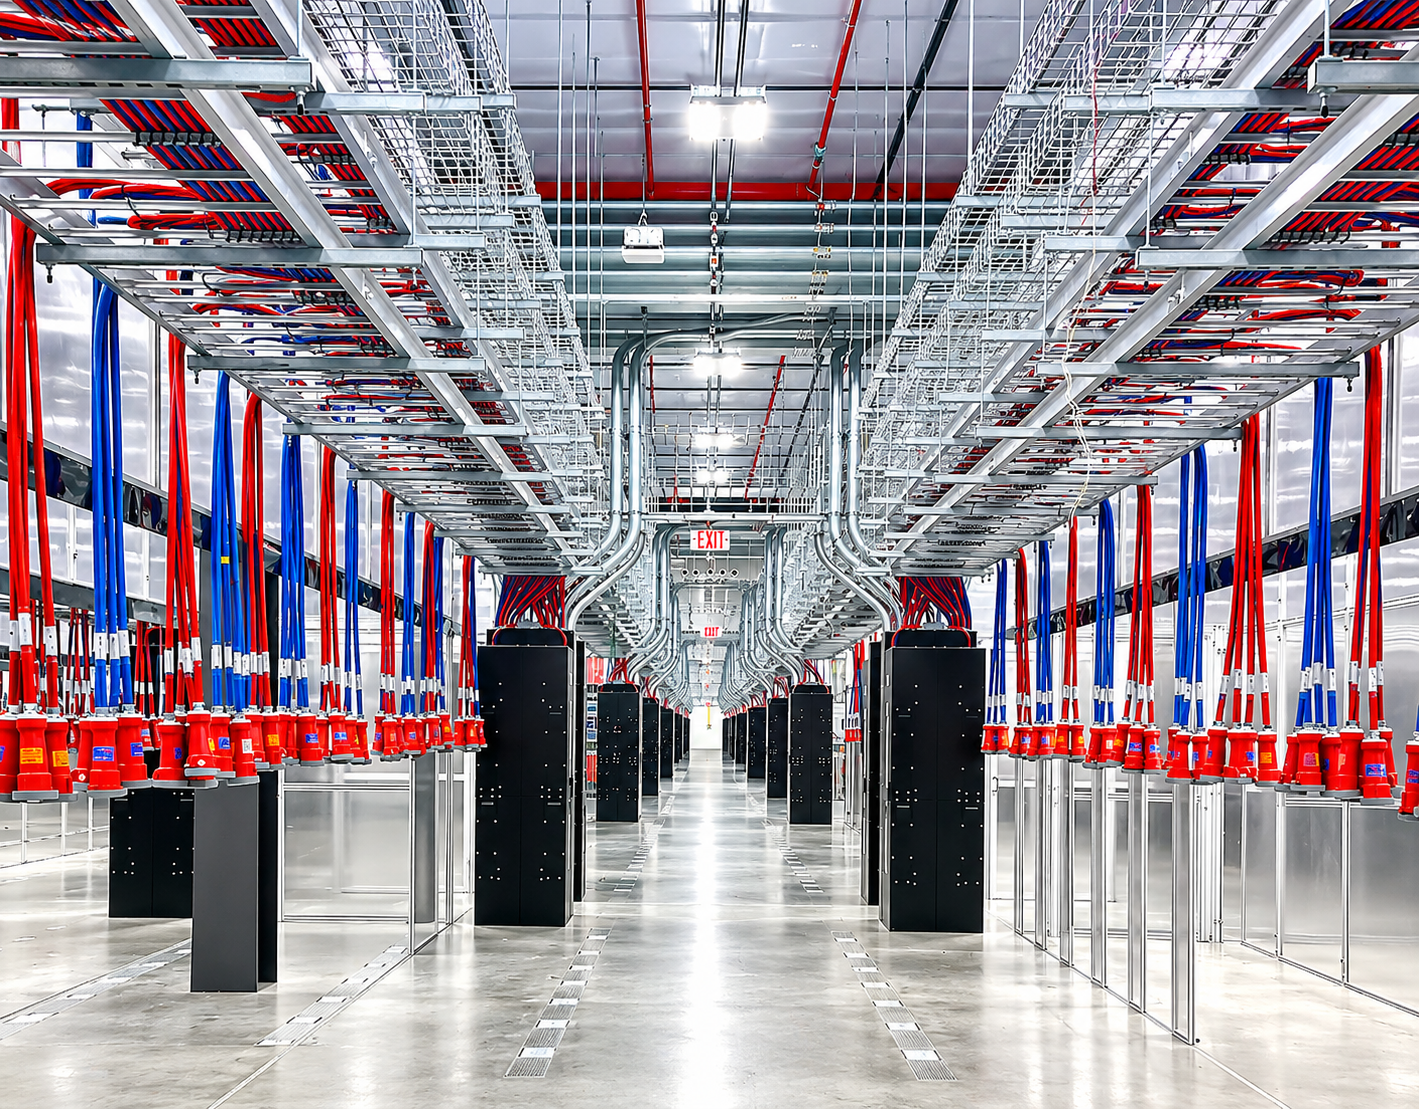
APEX DATA ENGINEERING is a sister company specializing in comprehensive data center solutions. We provide expert services across data center fit-out, MEP (Mechanical, Electrical, and Plumbing) works, structural fabrications, cable tray installations, and panel manufacturing.

Our commitment is to deliver high-quality, reliable, and efficient infrastructure tailored to support your critical data operations.

Our Services
Data Center Fit-Out
Data Center Fit-Out

Complete turnkey solutions for data center construction and setup, ensuring precision and compliance with industry standards.

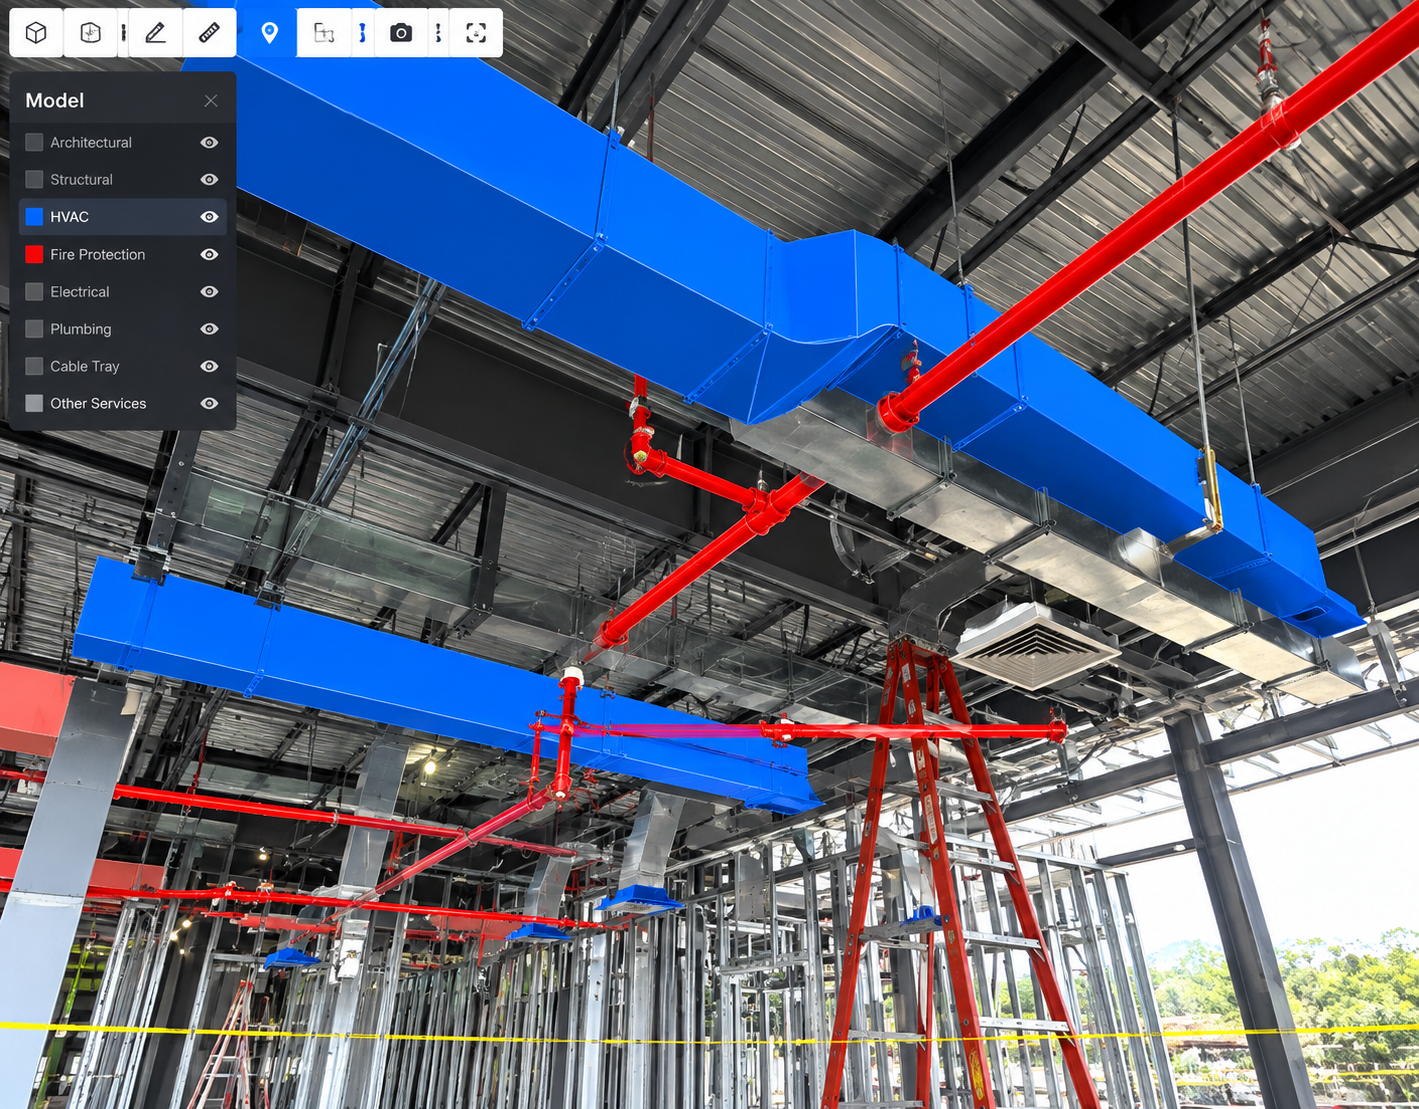
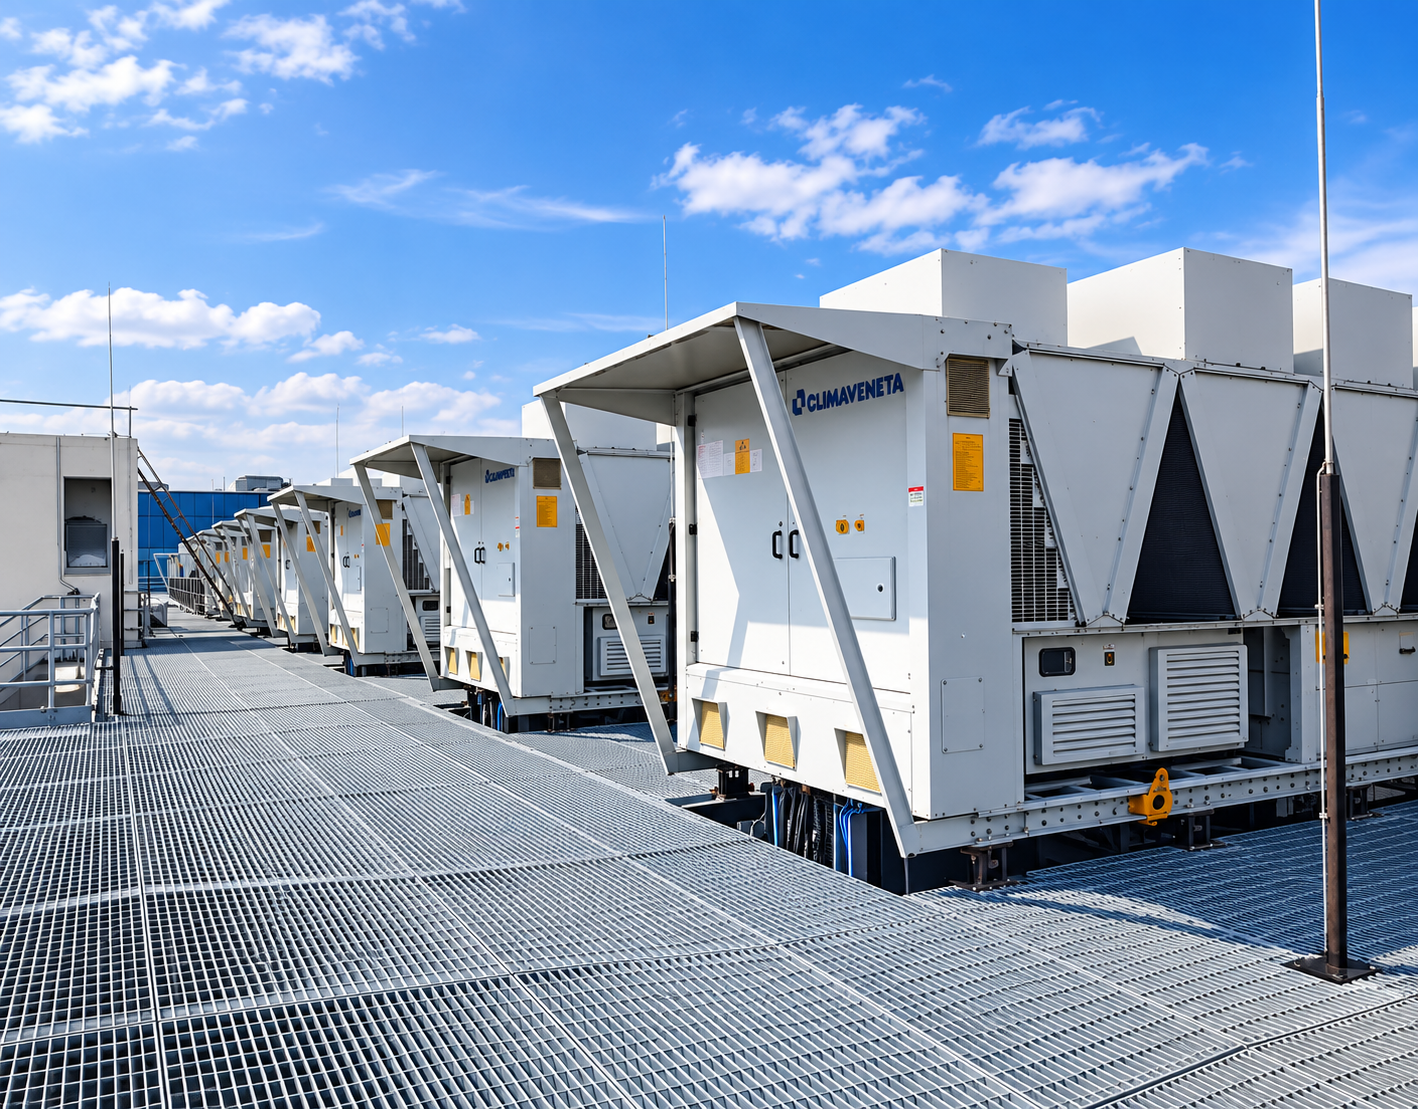
MEP Works
MEP Works

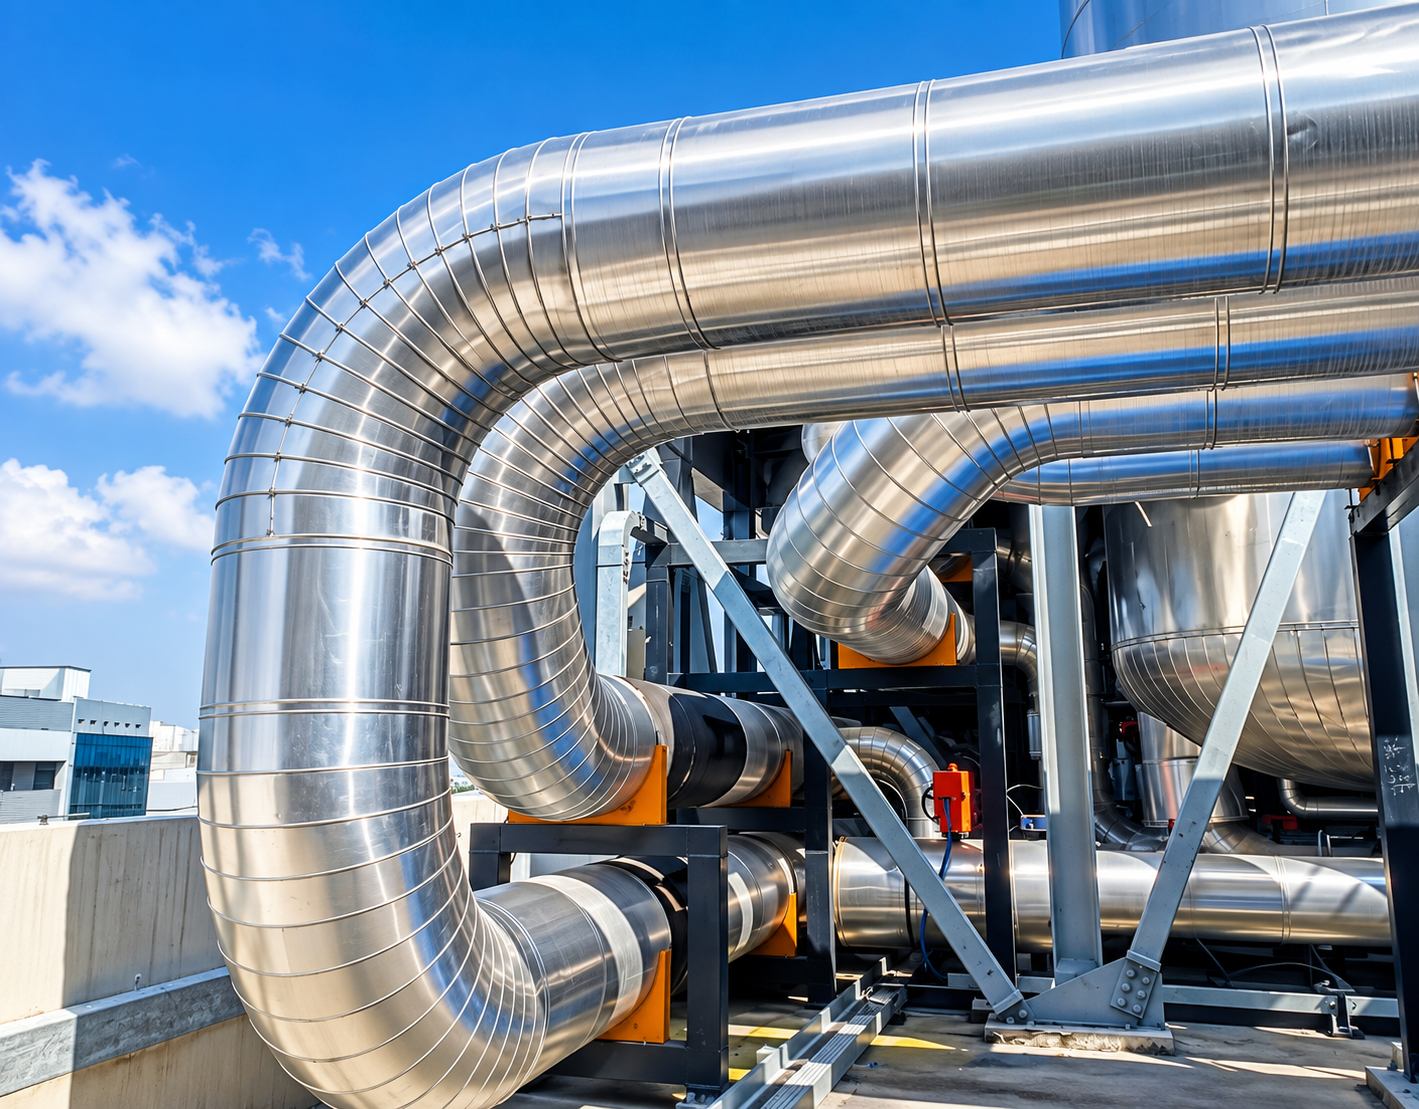
Expert design, installation, and maintenance of mechanical, electrical, and plumbing systems optimized for data center environments.

Structural Fabrications

Custom fabrication services catering to various structural needs, ensuring strength, durability, and timely delivery.

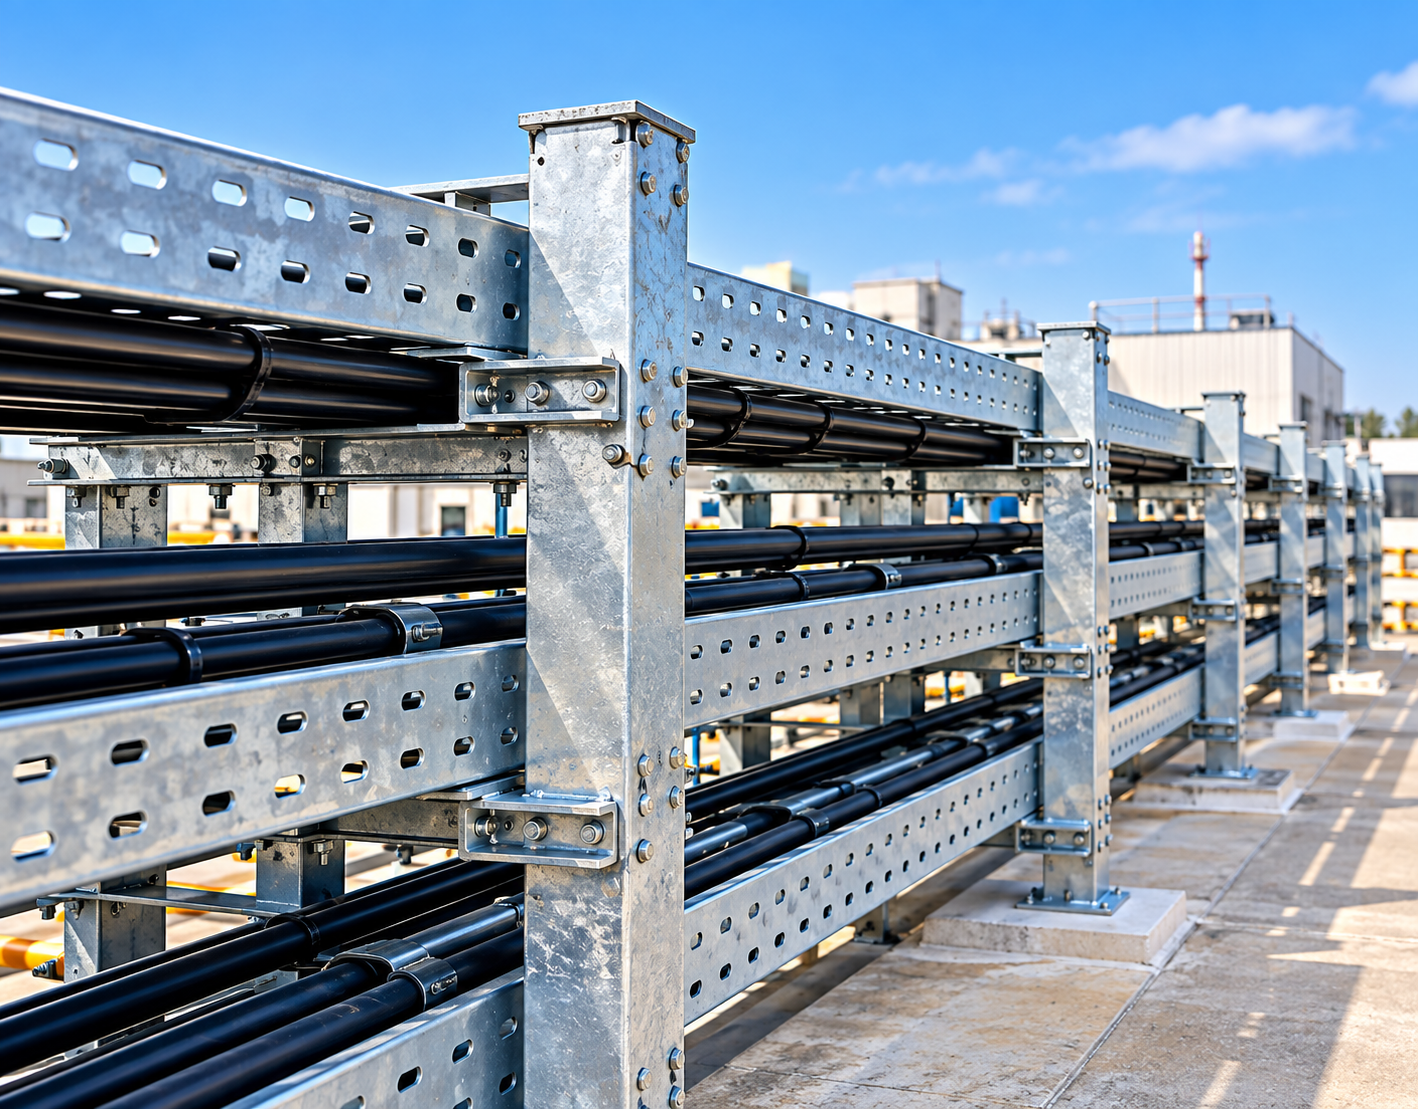
Cable Tray Installation

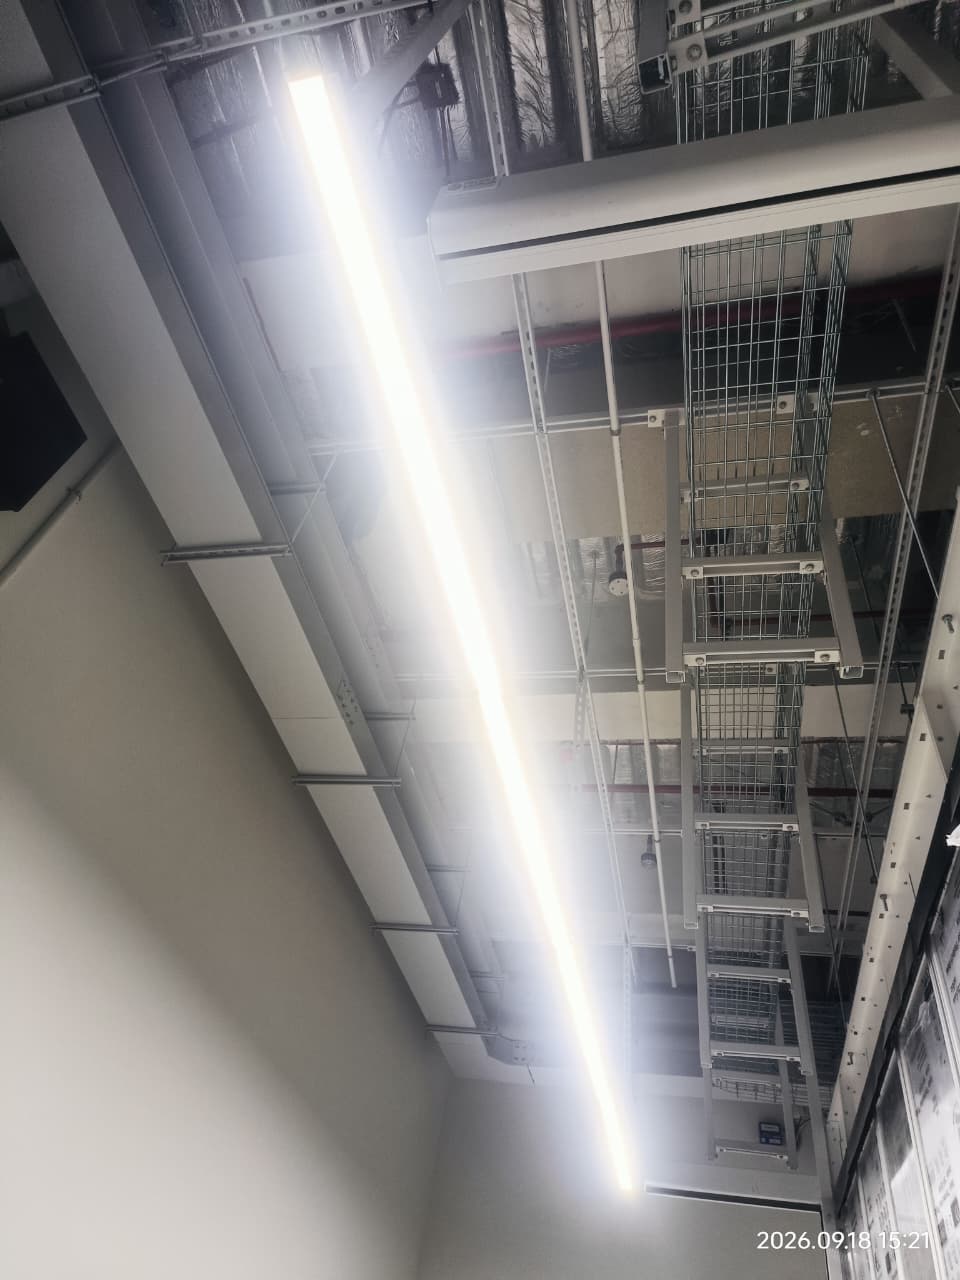
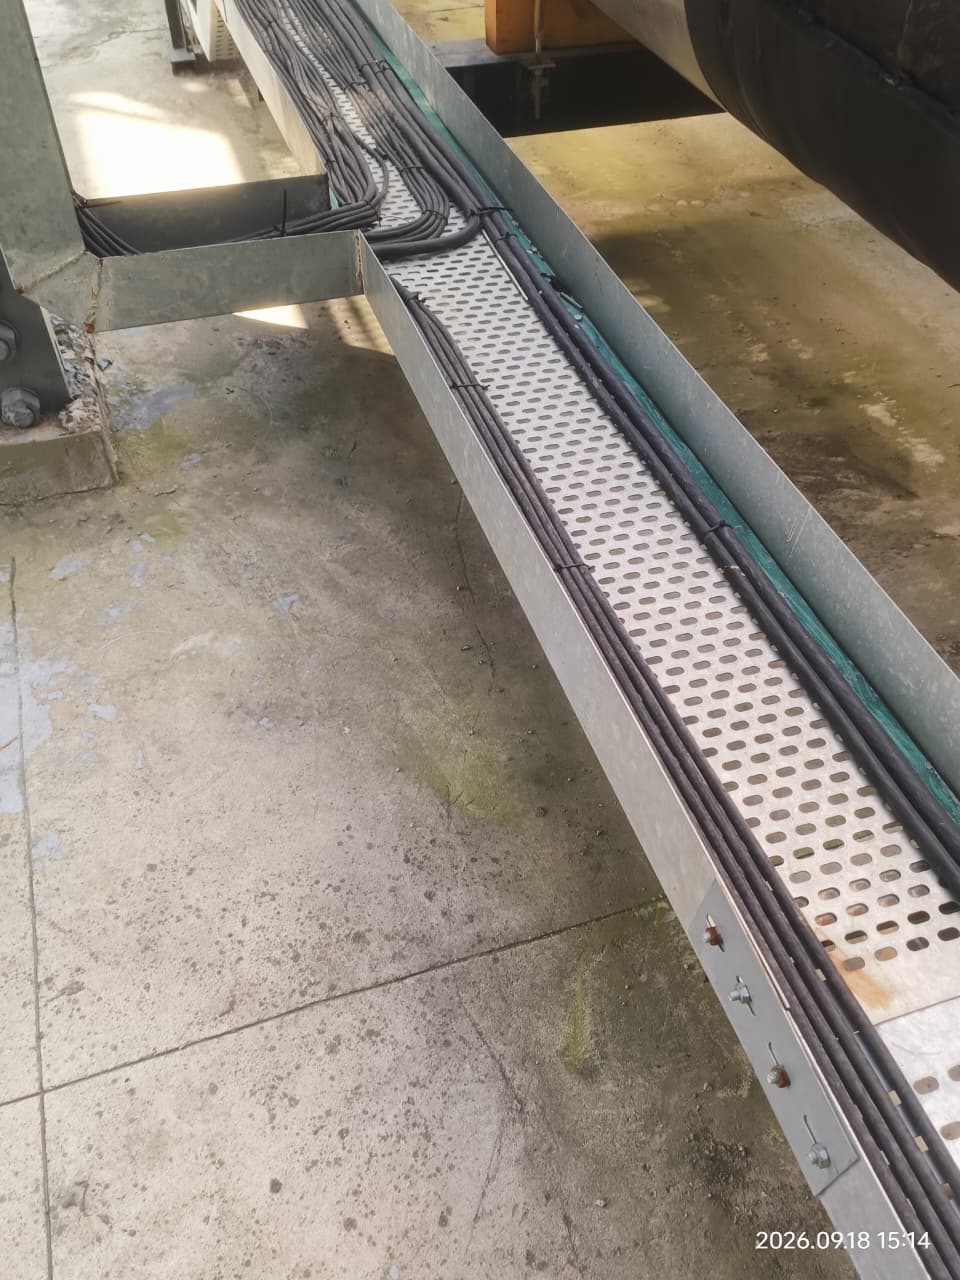
Supply and installation of cable trays designed for optimum cable management and safety.

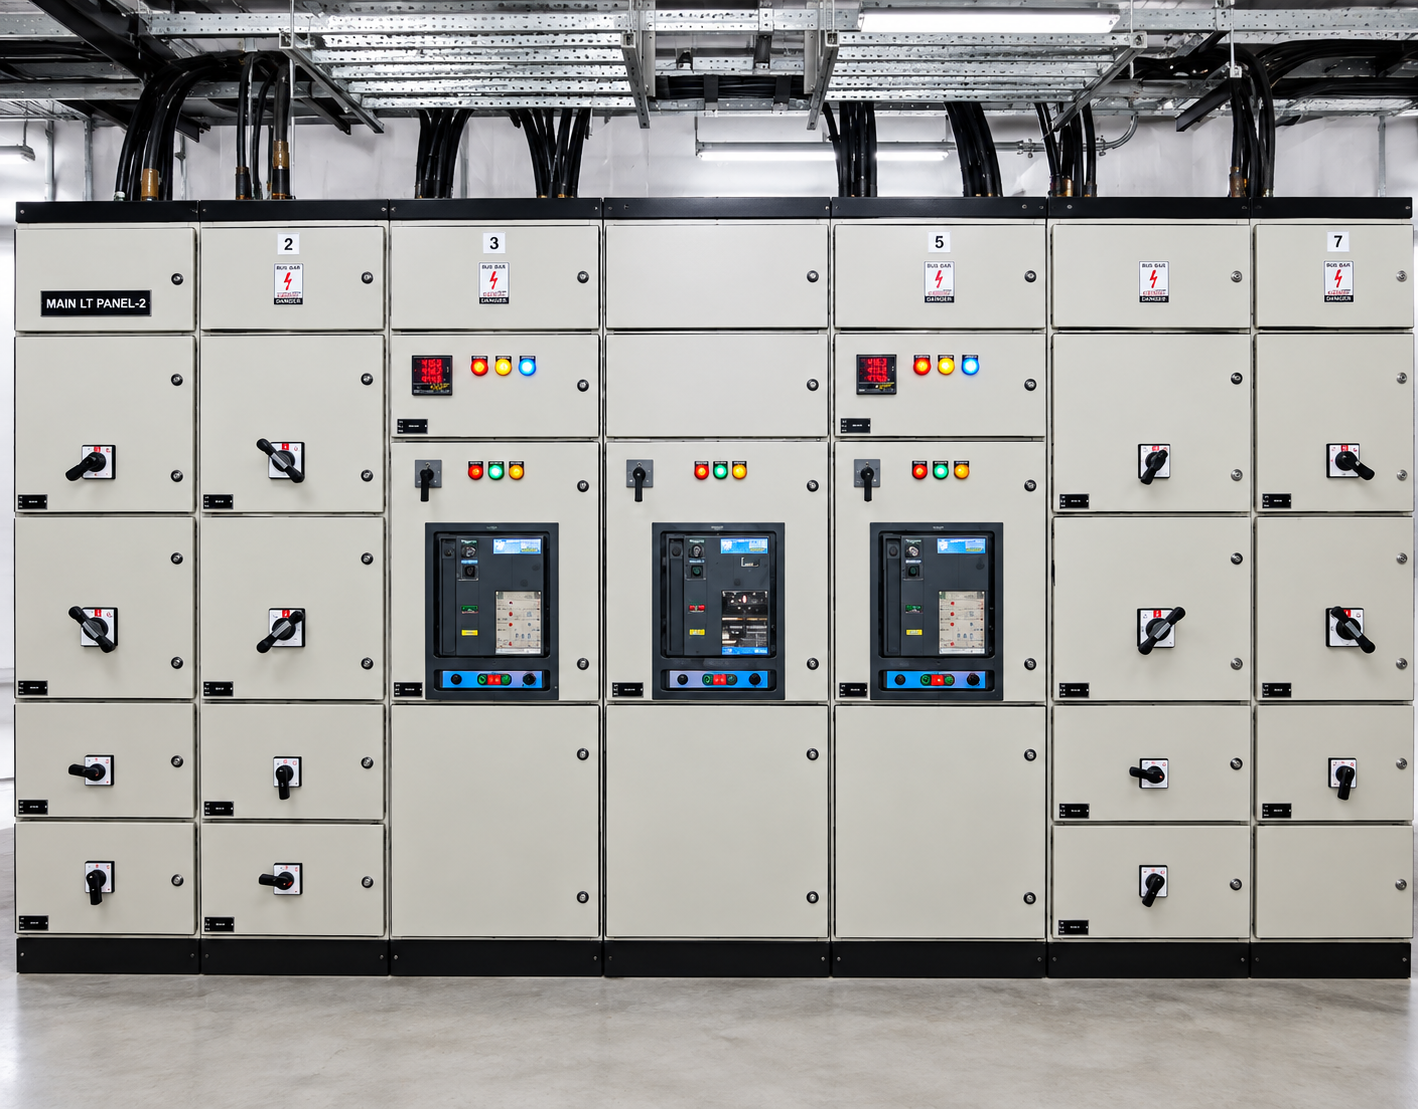
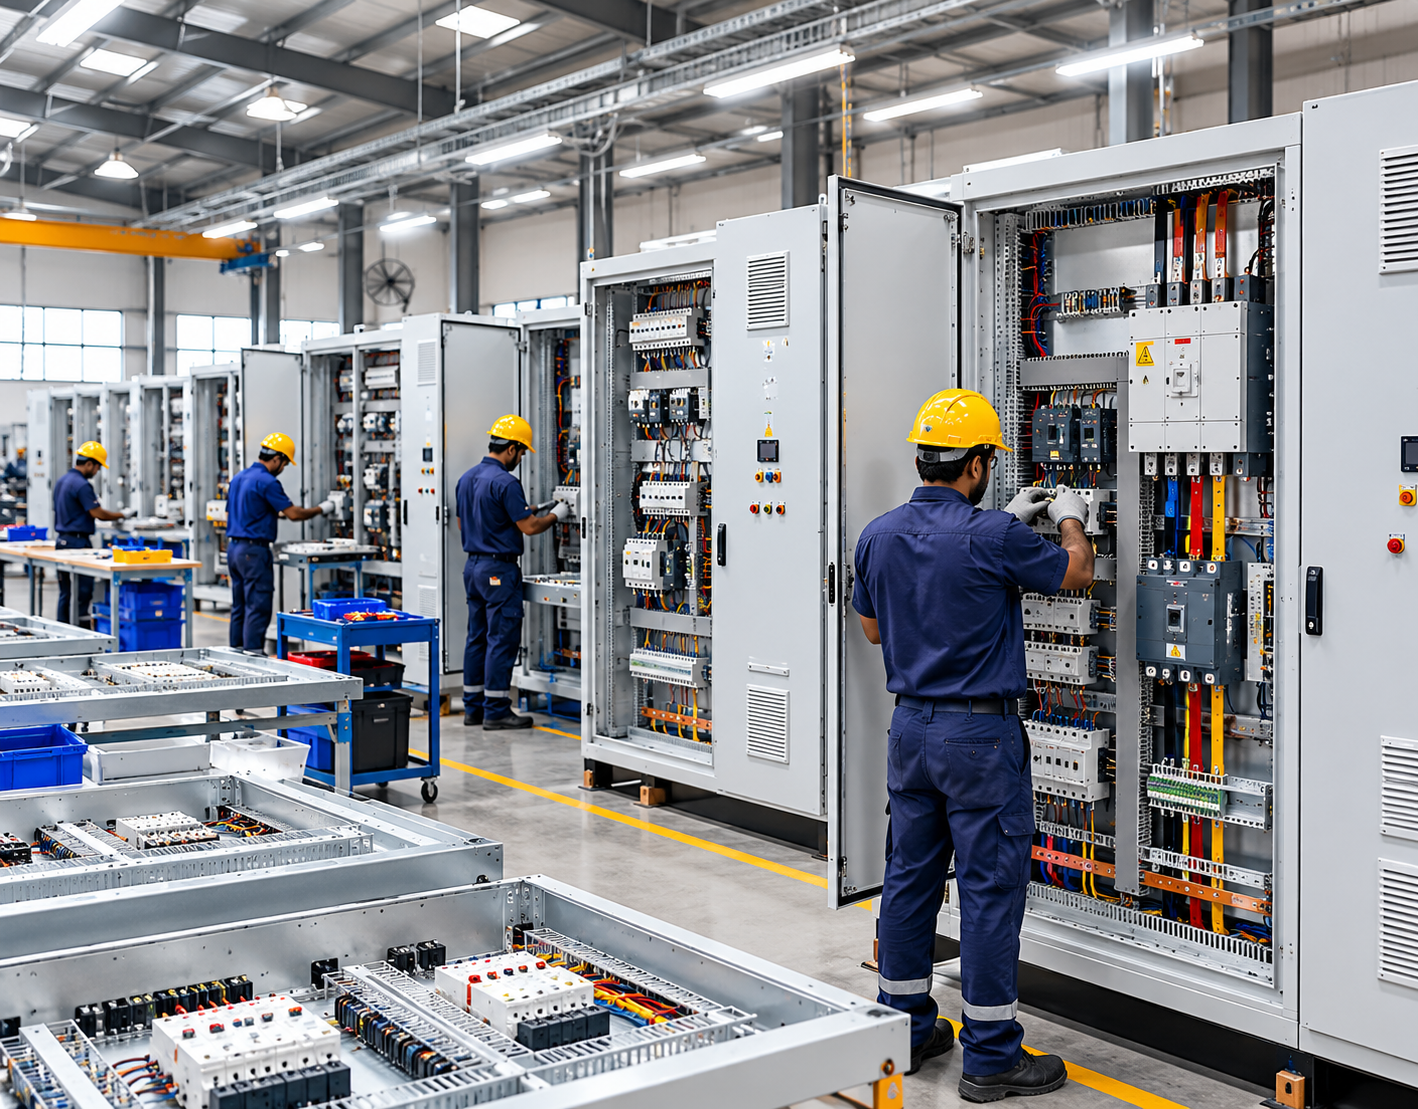
Panel Manufacturing
Panel Manufacturing

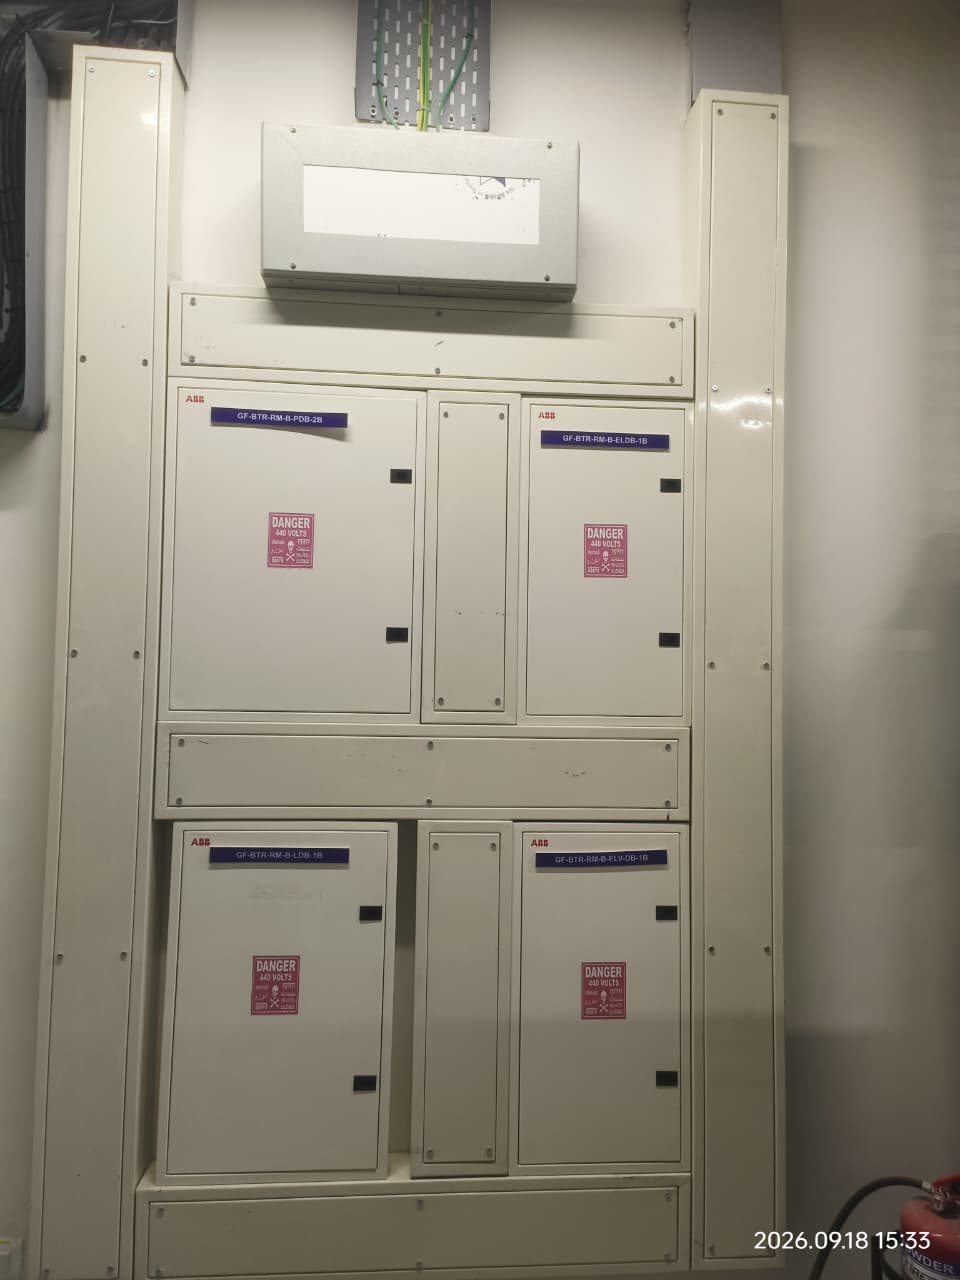
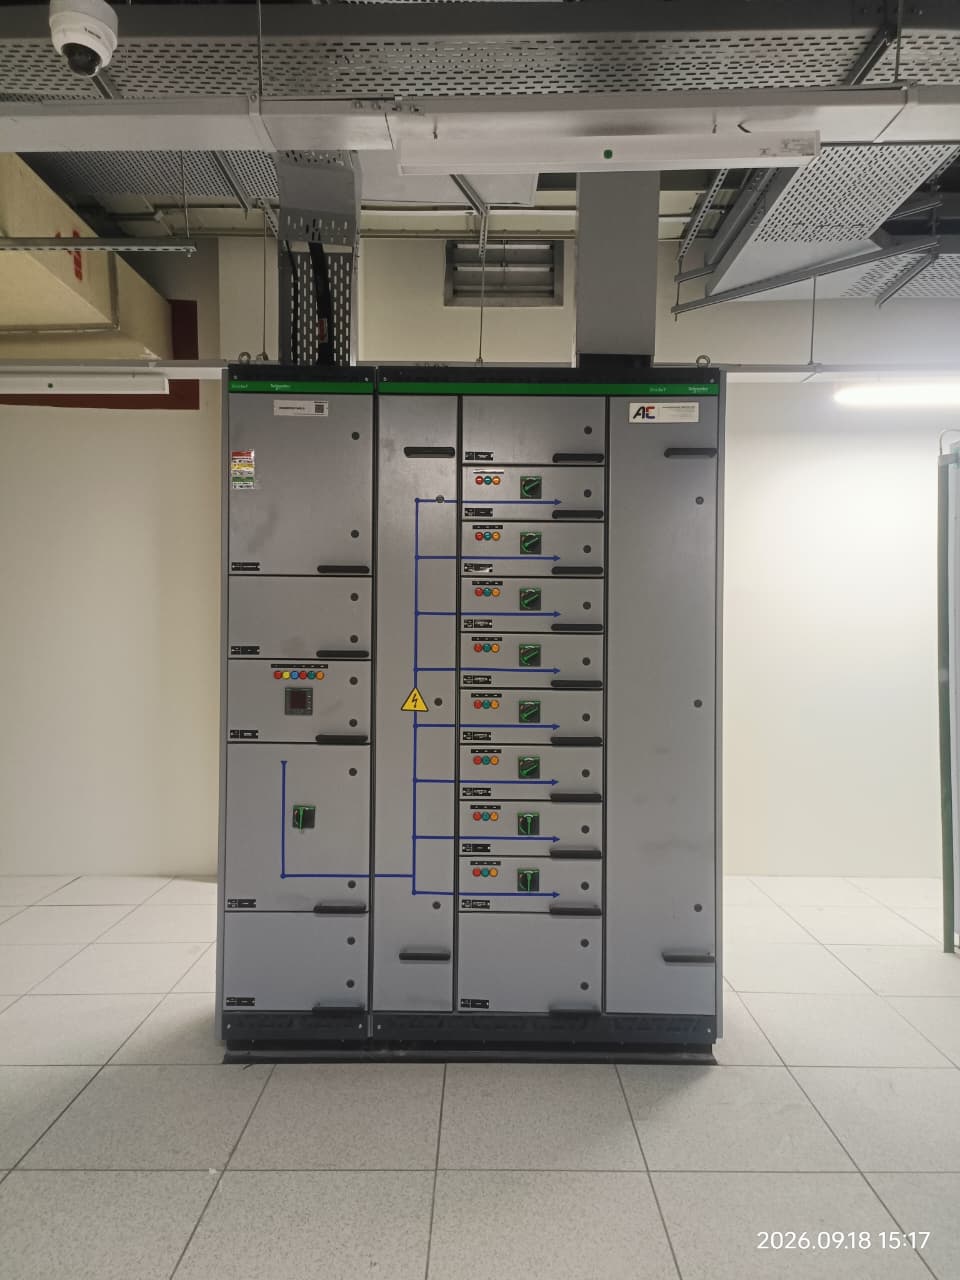
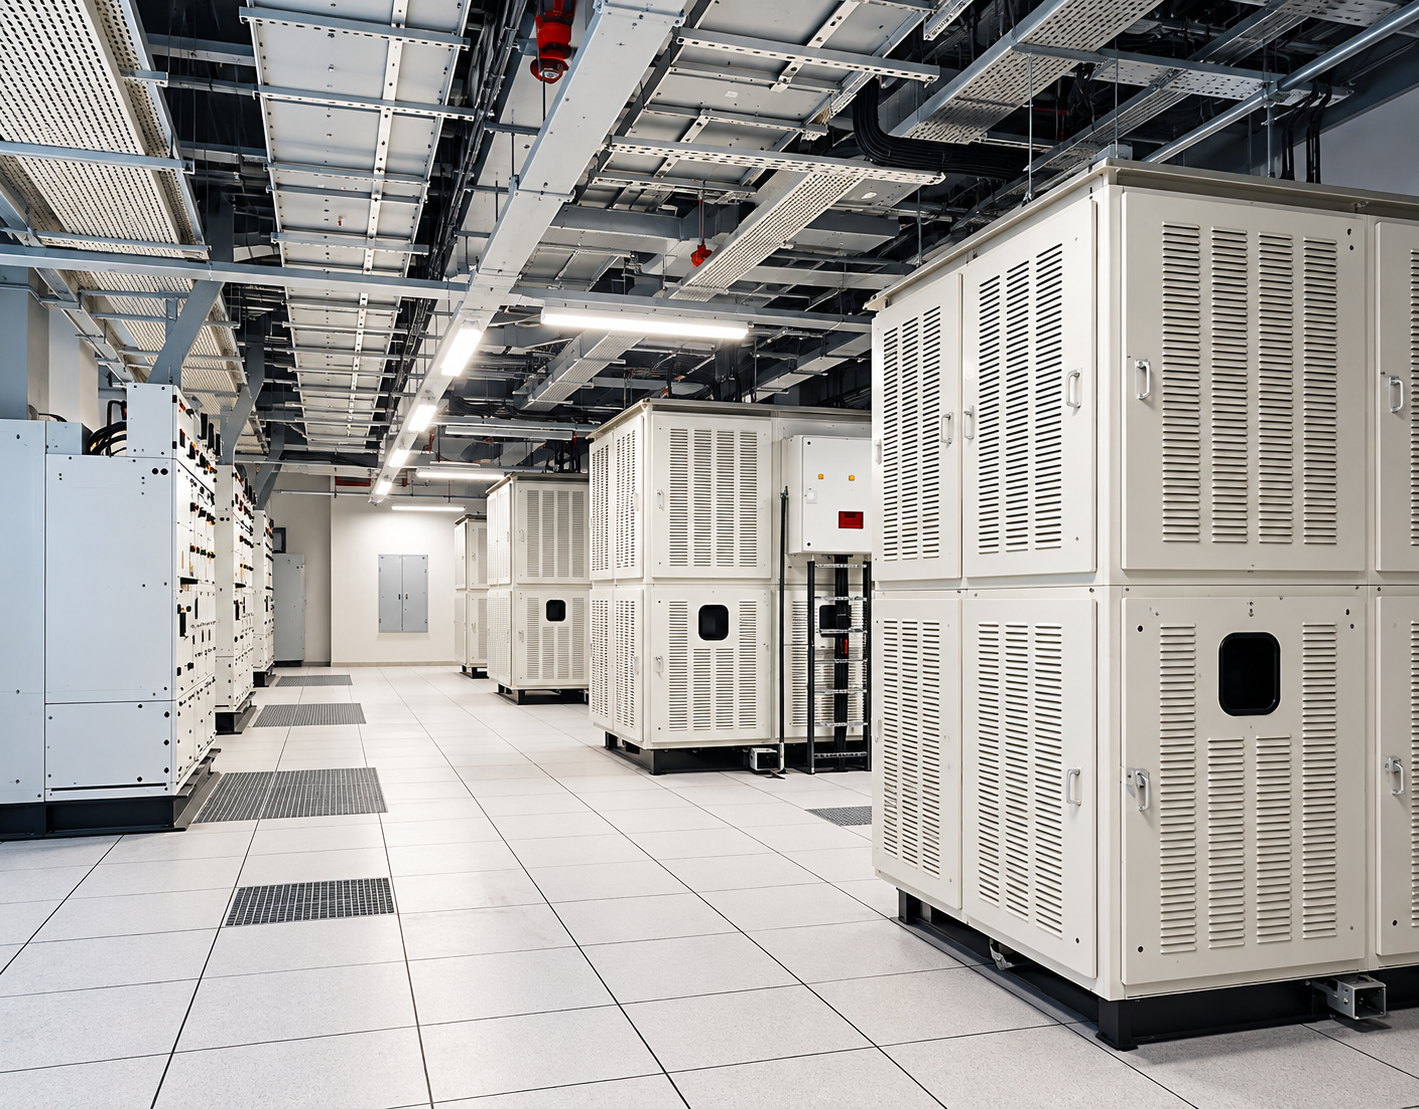
Production of high-quality electrical panels, designed to meet the specific requirements of data centers and industrial applications.

Our Key Clients

We proudly deliver SITC (Supply, Installation, Testing, and Commissioning) projects for reputed clients including:

Amazon Bridge Data Centers STT CapitaLand
Our Strengths
  • Expertise in handling complex data center projects.
  • Skilled workforce with a commitment to quality and safety.
  • Use of advanced technology and superior materials.
  • Timely project delivery and efficient customer service.
Vision

To be the leading engineering partner for data centers, enabling organizations to build resilient, scalable, and energy-efficient infrastructure.

Quality organisation

Who owns quality

Our Factory Quality function operates under the strategic direction of the Head of Quality, supported administratively by dedicated Factory Quality Controllers aligned to specific customer requirements. This structure ensures consistent quality, compliance, and customer satisfaction across all operations.

Delivery Head
Project Director
Quality Head
Quality Controller
Factory quality work on the shop floor
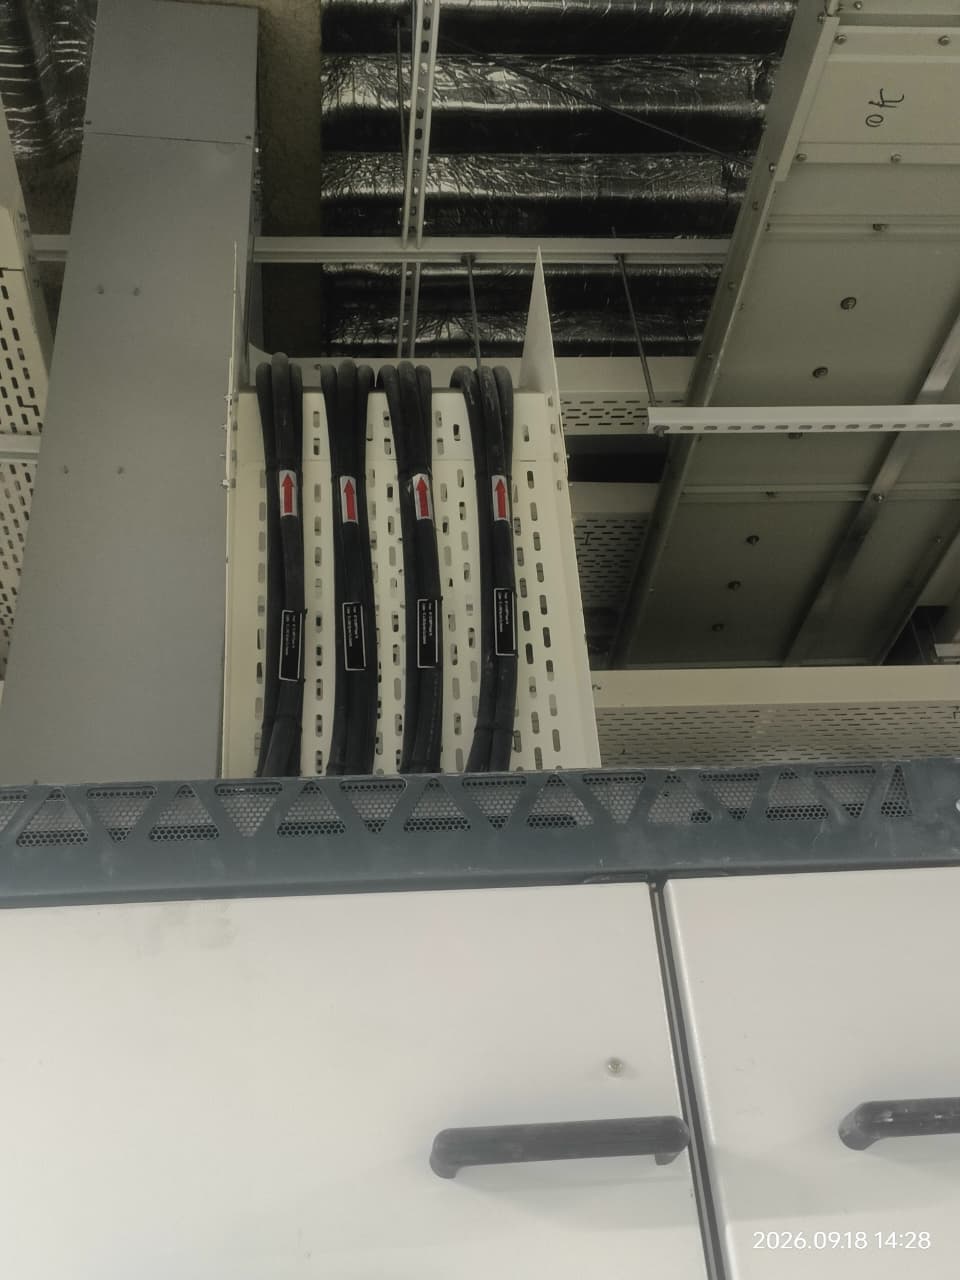
Installed cable management checked on site
Quality planning for factory work
Recognition for quality performance
Functional reporting Administrative reporting QC: Quality Control

Quality team

Key deliverables

Planning quality documents before construction

Pre-construction

  • Quality manual: management plan, assurance plan, method statements, test plan, checklists and formats.
  • Quality visuals: policy, theme, construction do’s and don’ts, and activity-based films.
  • Prequalification criteria and kick-off meetings with key contractors and vendors.
  • Project organisation chart with quality deployment, cascaded to the respective vendors.
Inspection and testing during construction

During construction

  • Inspection of ongoing works and approval of incoming materials at factory and site.
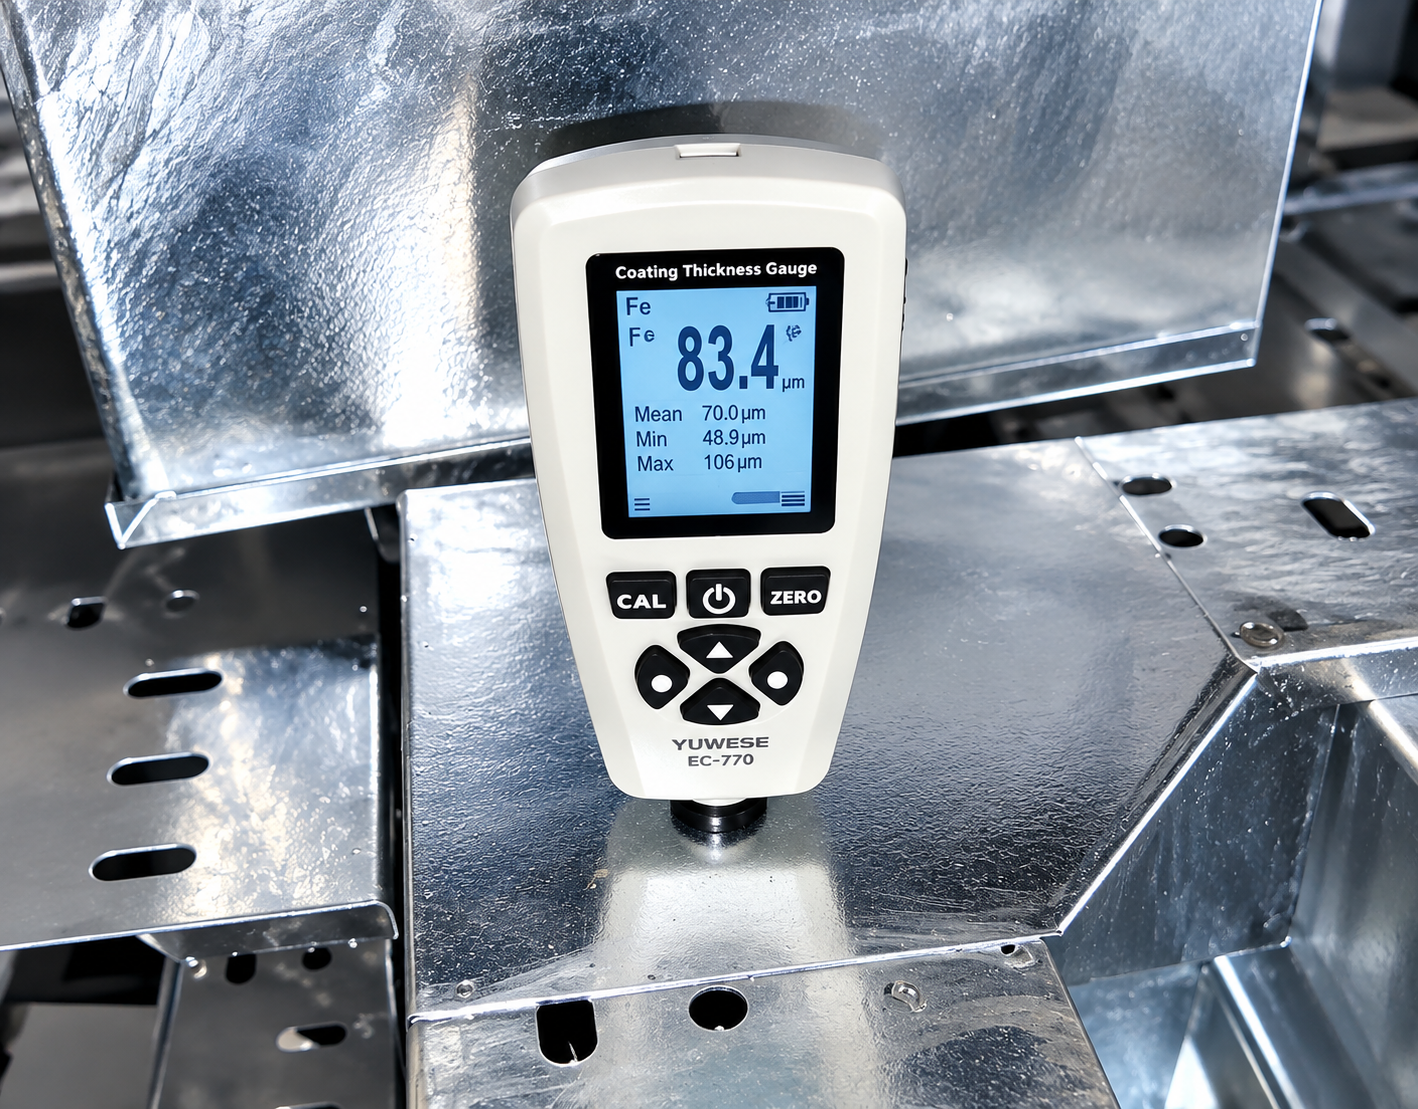
  • Testing of product performance, components and key materials against the requirement.
  • Training for workers, supervisors and engineers, plus toolbox talks and quality walks.
  • Assessments against defined quality parameters and standards.
  • Control of nonconformities through root cause and corrective action.
  • Recognition through Work of the Week, quality awareness and knowledge sharing.
Completed installation ready for handover

Post-construction

  • Snagging and de-snagging, then handover to the concerned representative or authority.
  • Testing and commissioning of product performance and the integrated system test.
  • Training for the operation and maintenance team, with an O&M user manual.
  • Technical assistance during the defect liability period.
  • Further quality improvements based on project learnings.

Quality control

Three inspection plans

Planning quality documents before construction

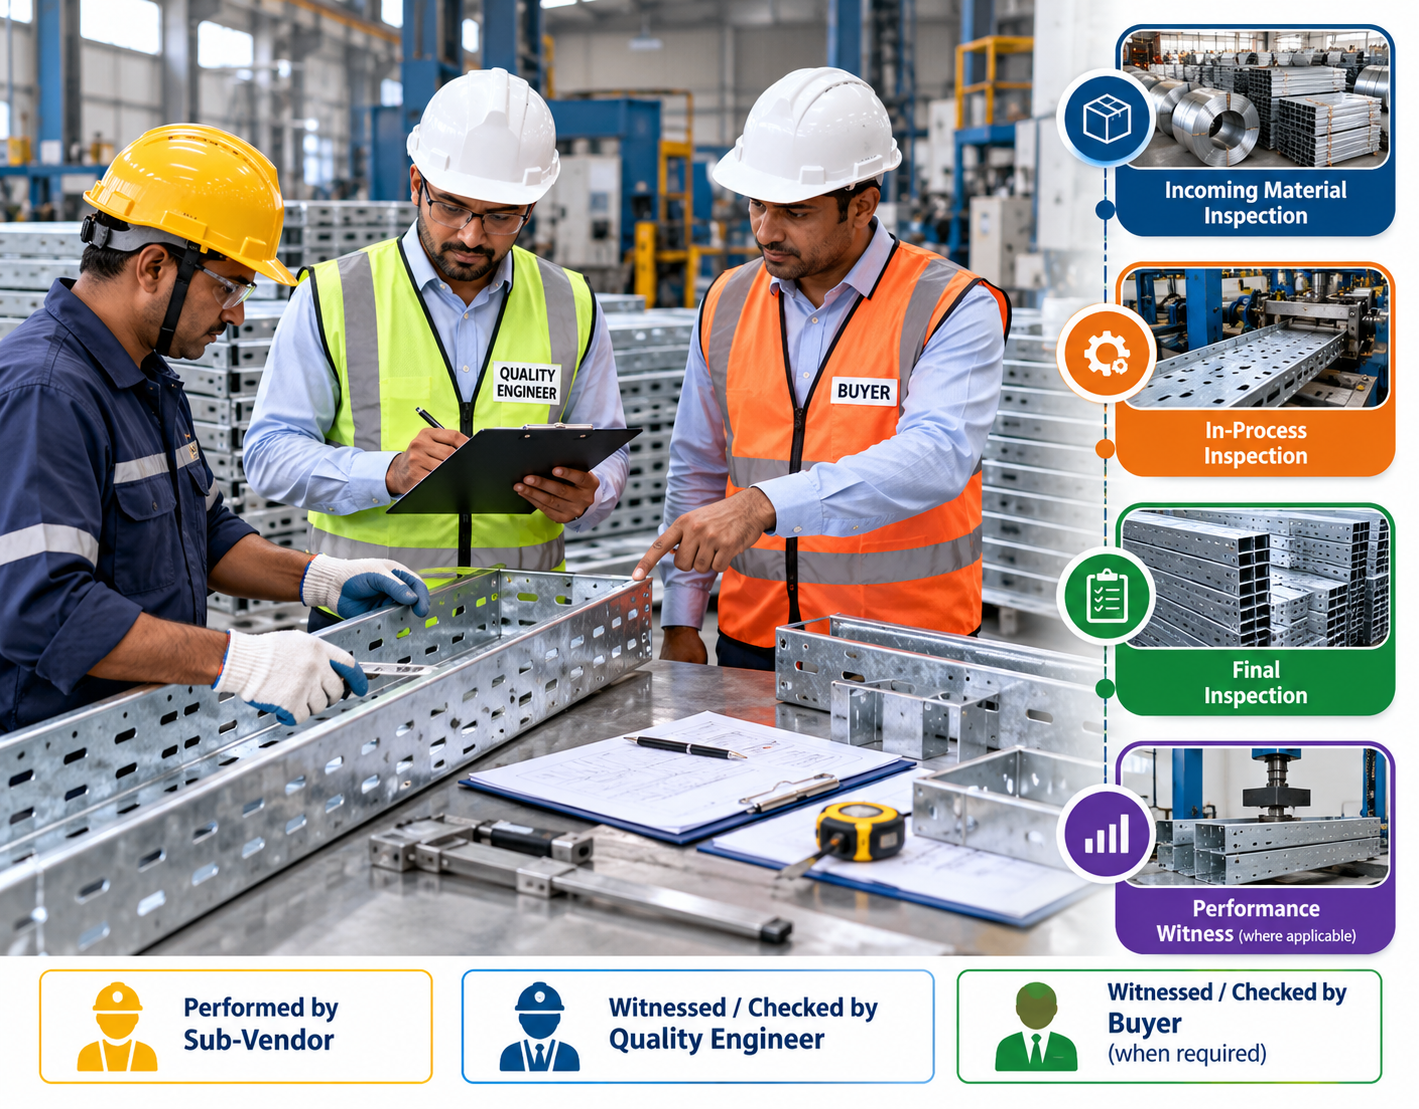
ITP

Inspection test plan for procured material at the sub-vendor factory.

  • Performed by the sub-vendor.
  • Witnessed or checked by the quality engineer, and by the buyer when required.
  • Records: incoming material inspection, in-process inspection, final inspection, and performance witness where it applies.
Planning quality documents before construction

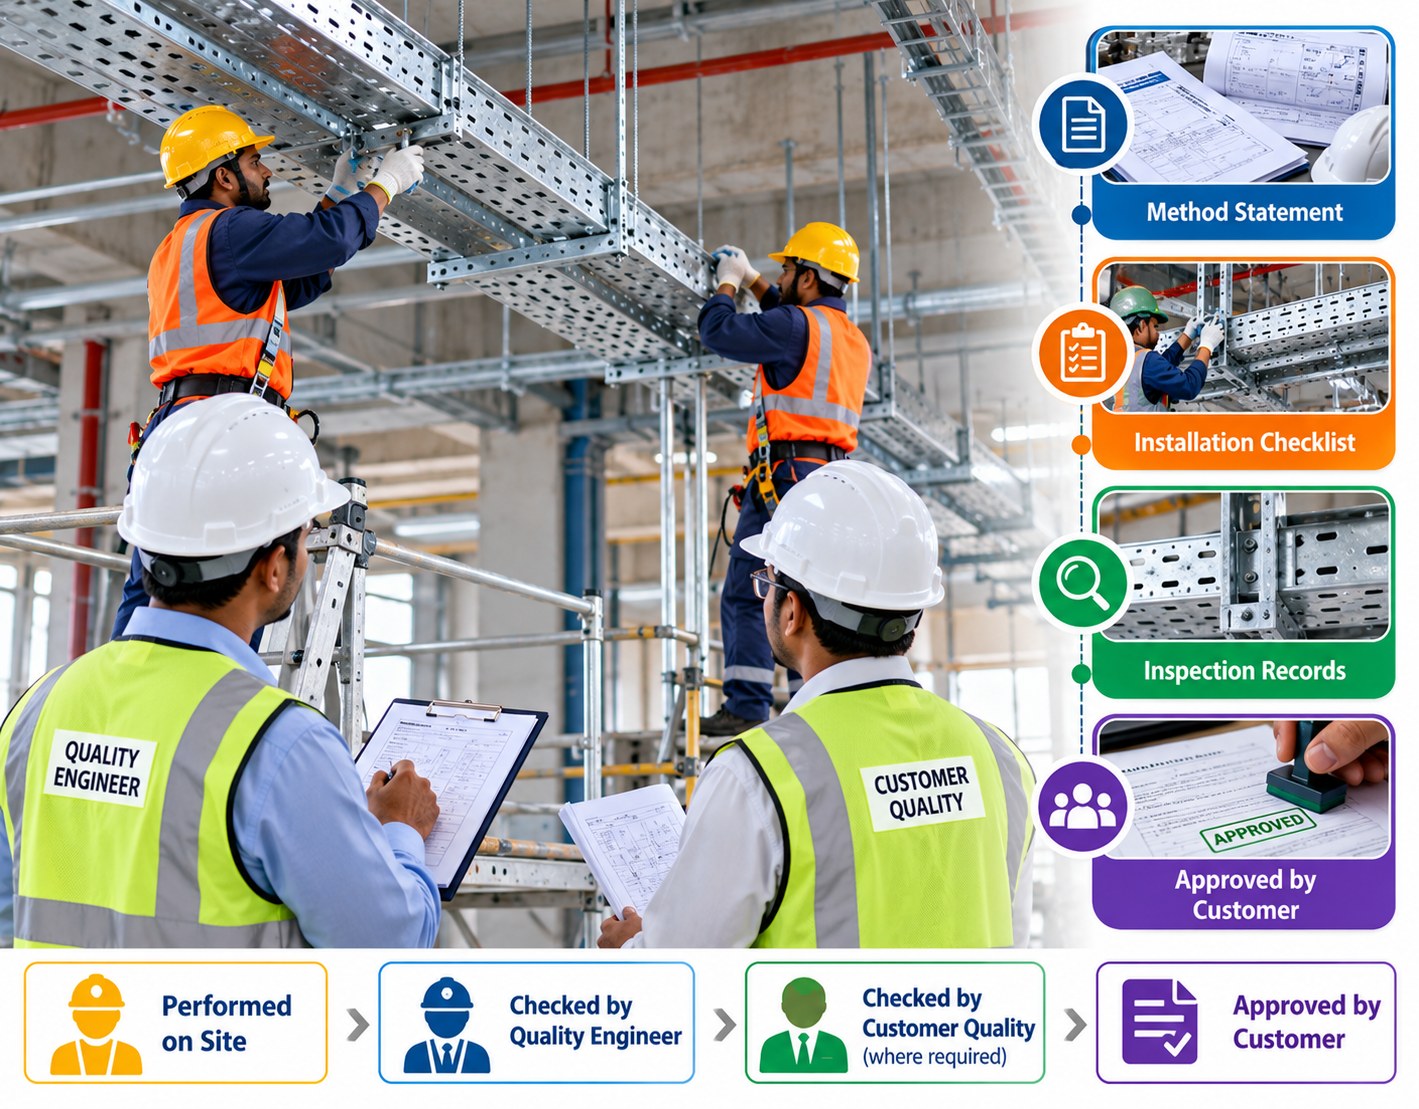
FQP

Field quality plan for physical installation of the system.

  • Performed on site and checked by the quality engineer and, where required, customer quality.
  • Approved by the customer.
  • Records: method statement, installation checklist and inspection records.
Planning quality documents before construction

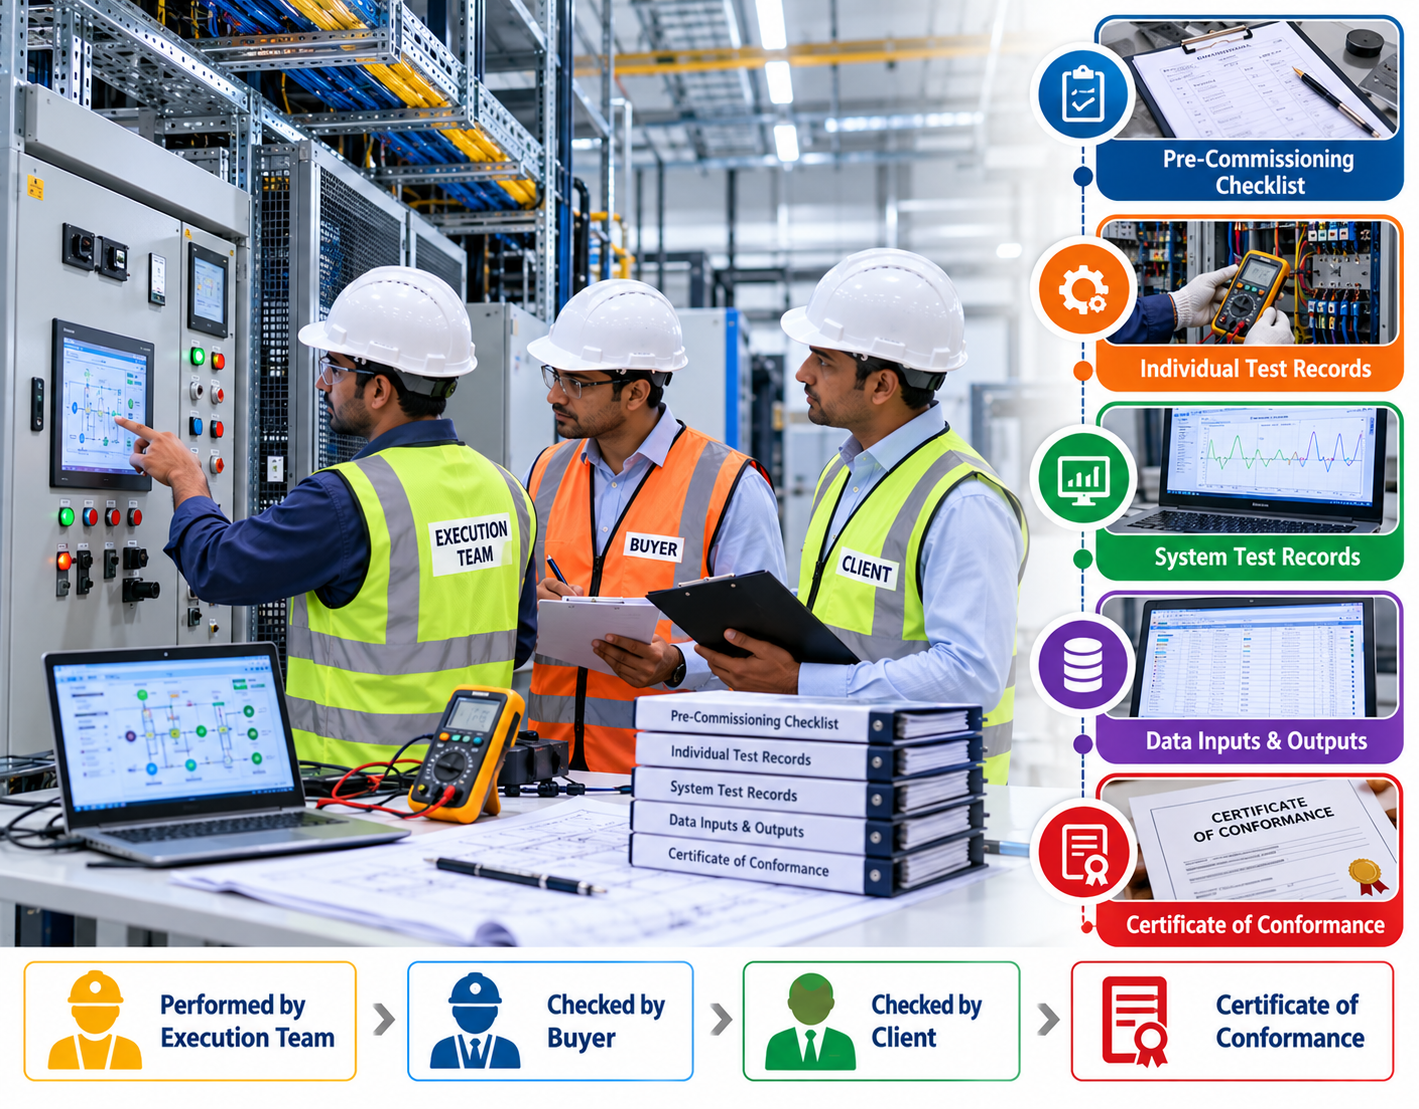
ATP

Acceptance test plan for the integrated performance test.

  • Performed by the execution team and checked by the buyer and the client.
  • Records: pre-commissioning checklist, individual test records, system test records, data inputs and outputs, and the certificate of conformance.

Commissioning levels

Tag colours show readiness

Factory acceptance before the red tag
Level 1 · Red

Factory acceptance

Factory acceptance test or factory witness test. The red tag is assigned once the equipment is delivered to site and anchored in place as per design.

Installation checked before the yellow tag
Level 2 · Yellow

Installation and QA/QC

Yellow is assigned when installation and Level 2 quality checks are complete and the equipment is ready for energisation.

Startup review before the green tag
Level 3 · Green

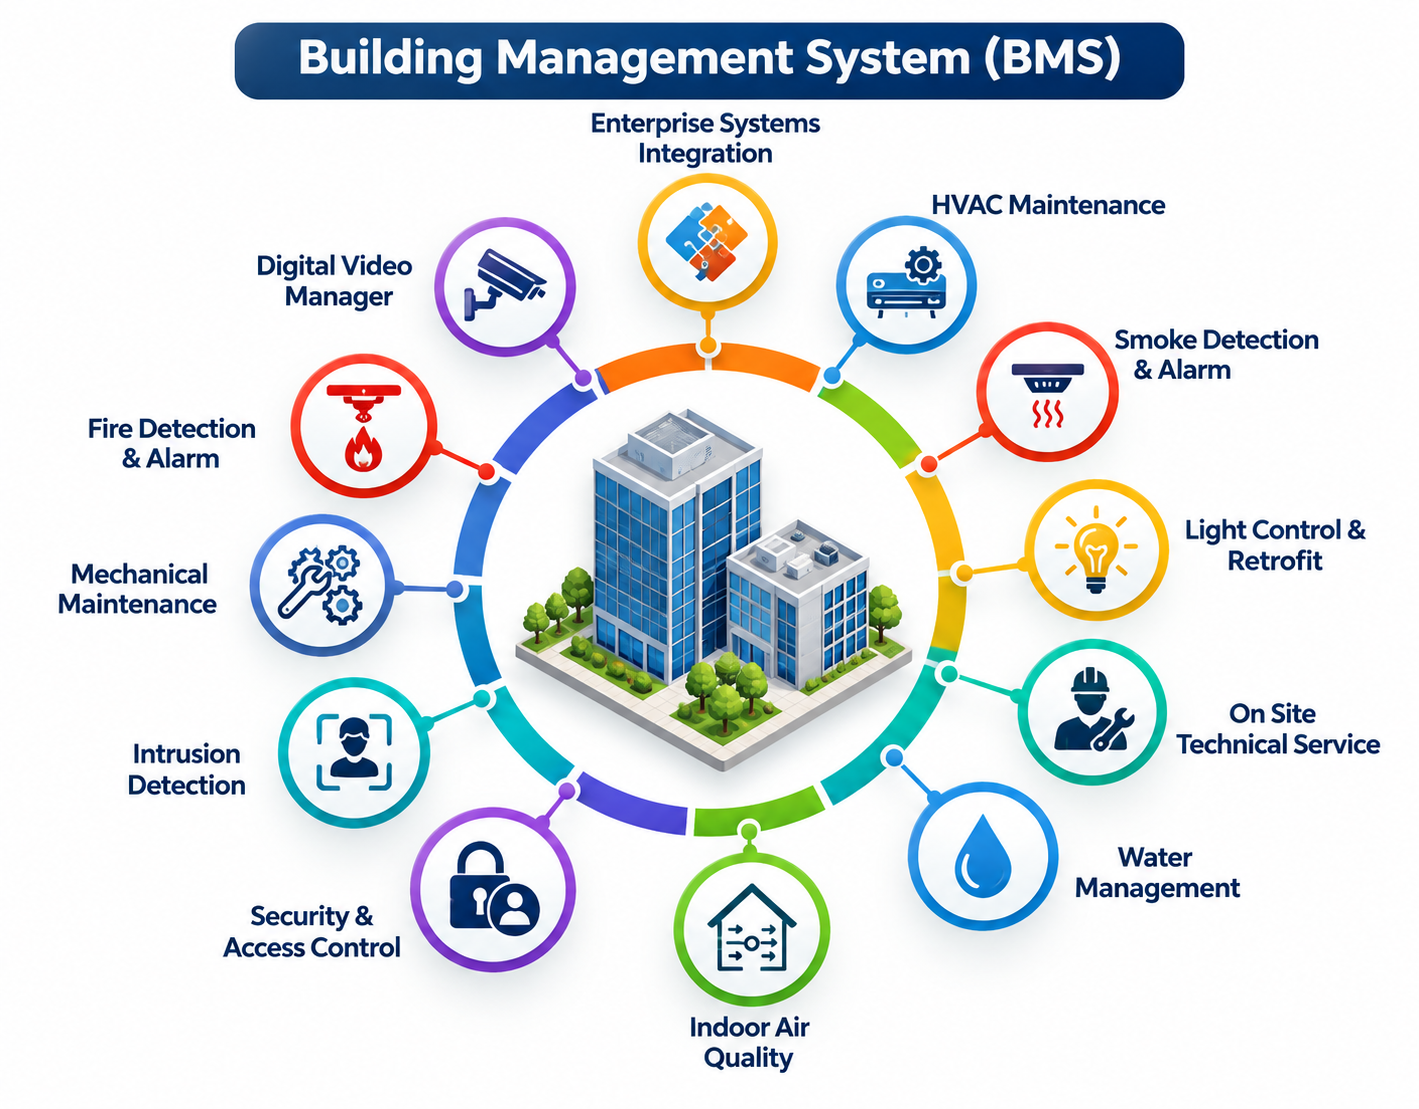
Startup and BMS

Green is assigned when Level 3 startup checks are complete and the equipment is ready for the functional test.

Functional performance before the blue tag
Level 4 · Blue

Functional performance

Blue is assigned when Level 4 functional checks and the sequence of operation are complete and the equipment is ready for the integrated system test.

Integrated system test before the white tag
Level 5 · White

Integrated system test

White is assigned after a successful pre-integrated system test and the final integrated system test.

Project close-out and handover
Level 6 – 7 · No tag

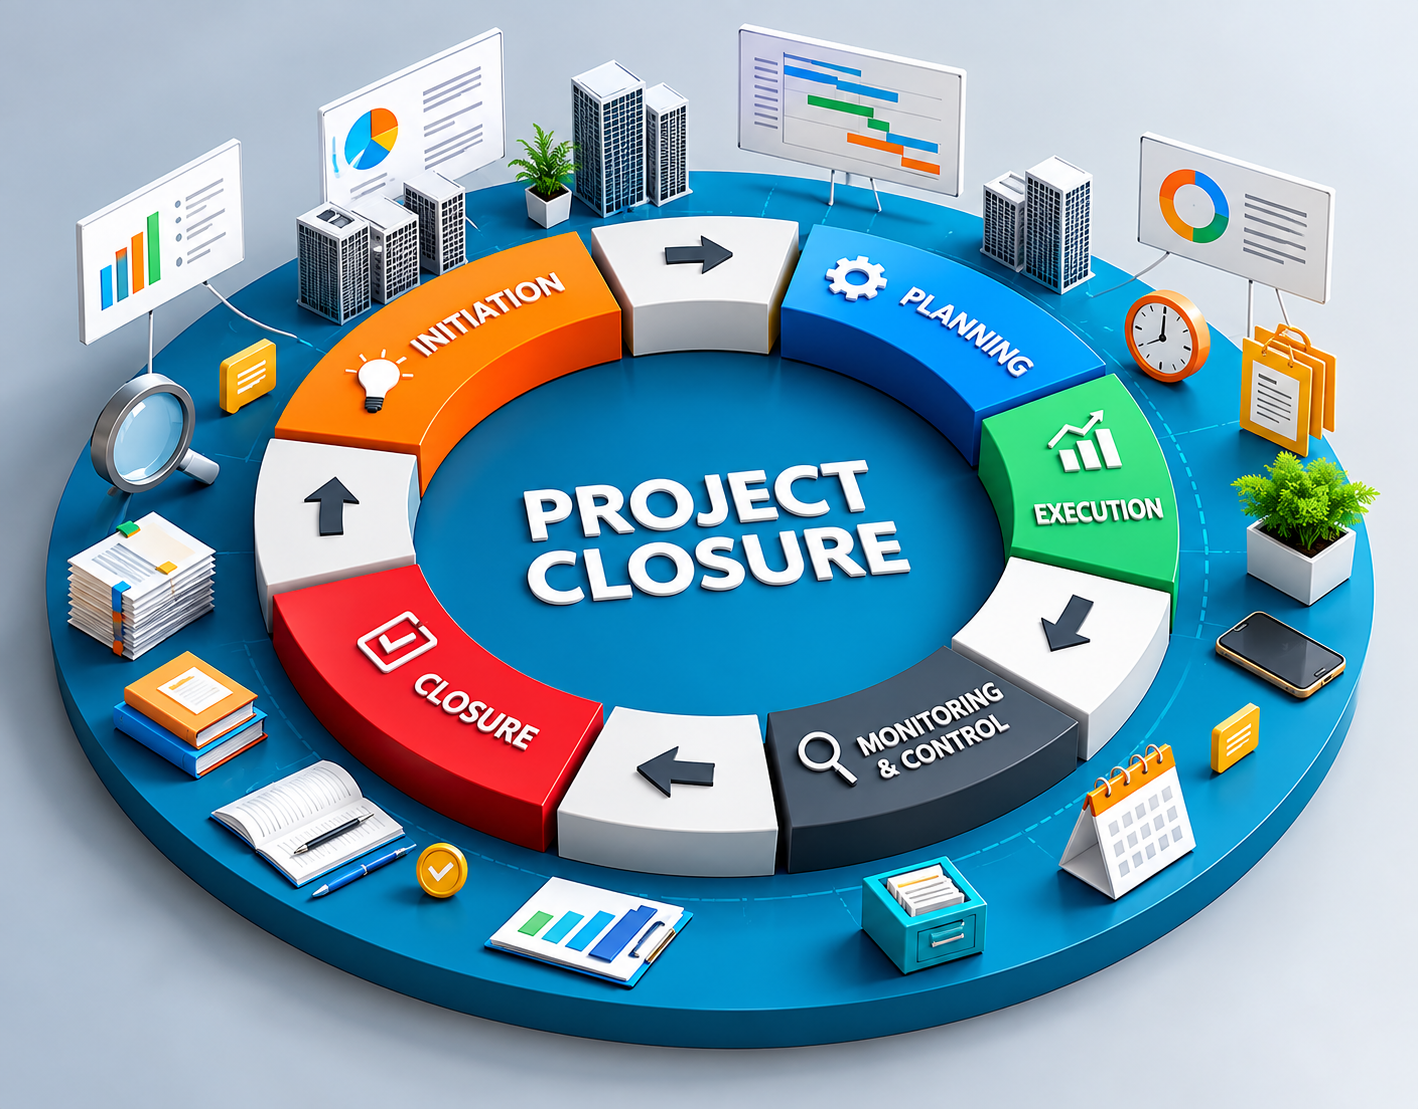
Project closure

Level 6 is close-out and turnover. Level 7 is acceptance of the final reports and documents.

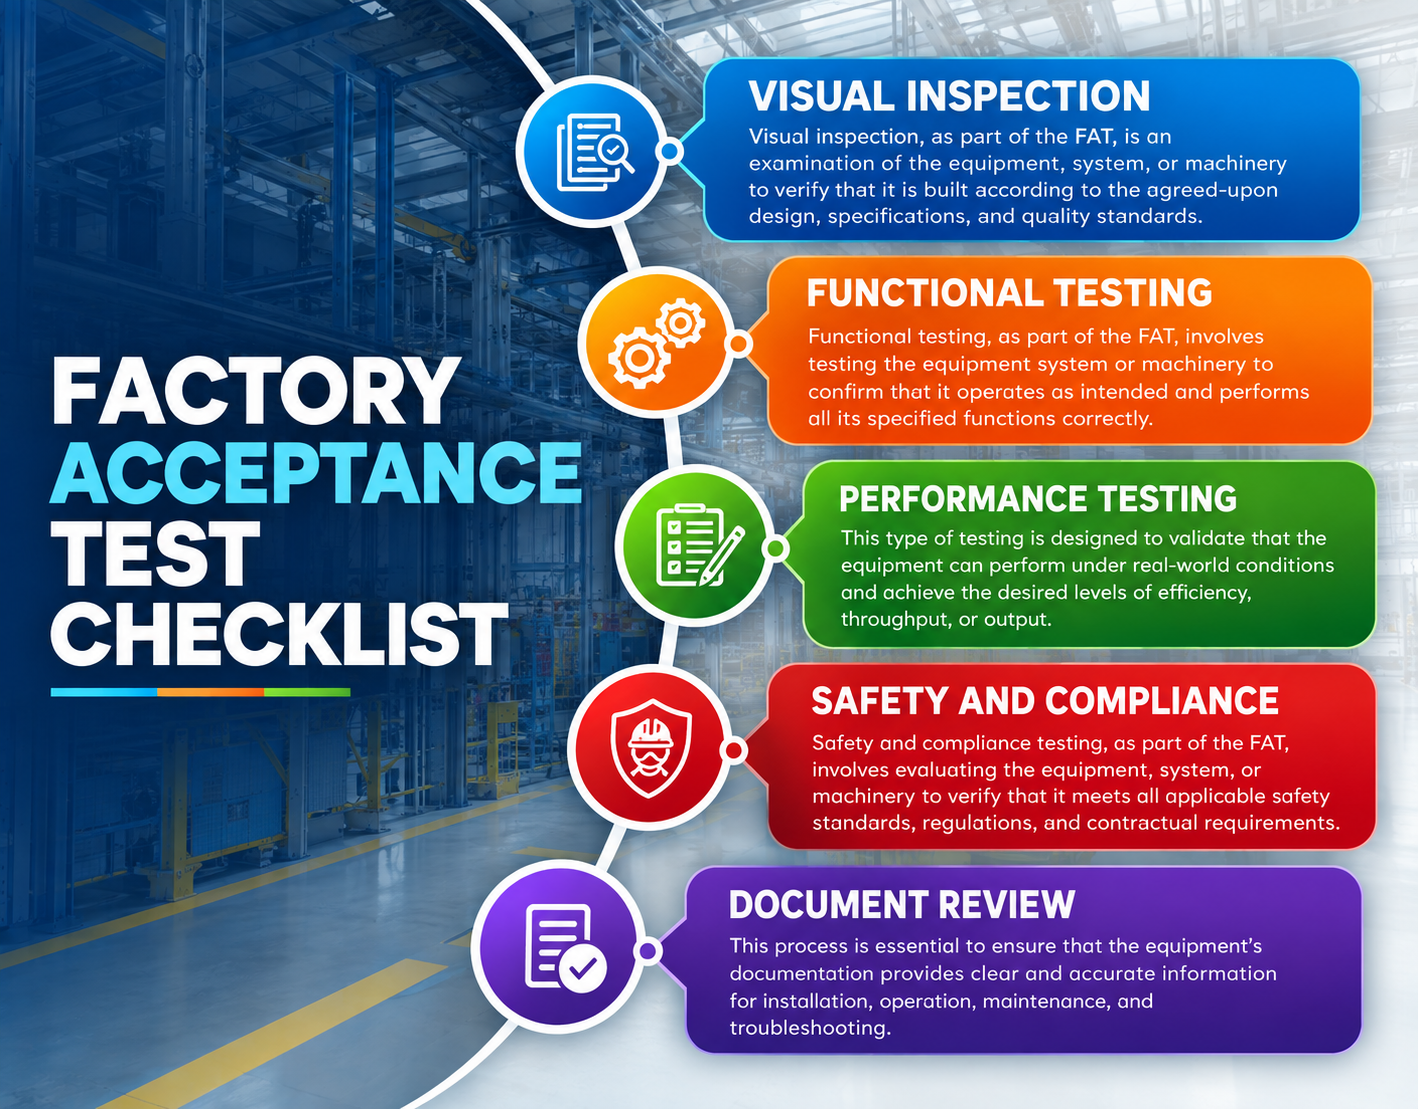
Factory acceptance test

Checked before anything leaves the factory

Before material is dispatched to site, the parameters in the quality assurance plan are verified and inspected at factory level. Nothing is released on paperwork alone.

Materials

Samples, incoming inspection and stacking

Sample gallery

Material samples are showcased in the sample gallery against the tender specification, the approved technical data sheet, and feedback from the PMC or client.

IMIR quality check

  • On arrival, materials are inspected by the quality team before unloading.
  • They are checked against the approved technical data sheet, bill of quantities and technical specification.
  • Material that meets the requirement receives unloading clearance.
  • Unsatisfactory material is rejected and the supplier is informed.

Stacking at the work location

Material at the work front is stacked so it stays identifiable, accessible and protected until it is installed.

Stacking in the store

Store stacking keeps batches separated, off the ground where required, and preserved until issue.

Welding

Preparation, performance and DP testing

Preparation

  • A 45-degree V groove is prepared by grinding the pipe.
  • A 2.5 mm gap is maintained between the pipes.

Performance at site

  • Each welder performs a welding test at site under the quality engineer and the PMC or client representative.
  • The test piece is sent to a laboratory for testing and evaluation.
  • A successful result produces an acceptance certificate, which is mandatory before that welder continues on site.

DP test

Dye penetrant testing is carried out as a random check on 5–10% of the welds.

TBT programmes

Briefings before the work, recognition after it

  • A safety induction is conducted for every site worker before they are deployed on site.
  • Job-specific toolbox talks are held regularly for all site workers.
  • A monthly reward and recognition programme selects and awards contractors.

Quality documentation

Project-specific records that control the work

The documents used to control quality at the work front are project specific.

Plans

Field quality plan and quality management plan, with the inspection test plan.

Approvals

Material sample and mock-up approval documents.

Methods

Work method statements for the activities being carried out.

Installation

Installation checklists completed as the work is built.

Commissioning

Commissioning checklists for startup and system tests.

Factory

Factory acceptance test records before dispatch.

Observations

Internal observations, NCR and CAPA

Internal quality observations are raised when work drifts from the approved method or specification. A nonconformance report records what failed. Corrective and preventive action then identifies the probable root cause and the action that stops it happening again.

Contact Apex Data Engineering


Mobile: +91 7842005913 / info@apexdataengineering.in

Office: Umamaheswara Apartment - 401, Road No. 2, Kousalya Colony, Krishnaja Hills, Nizampet, Hyderabad, Telangana 500118.